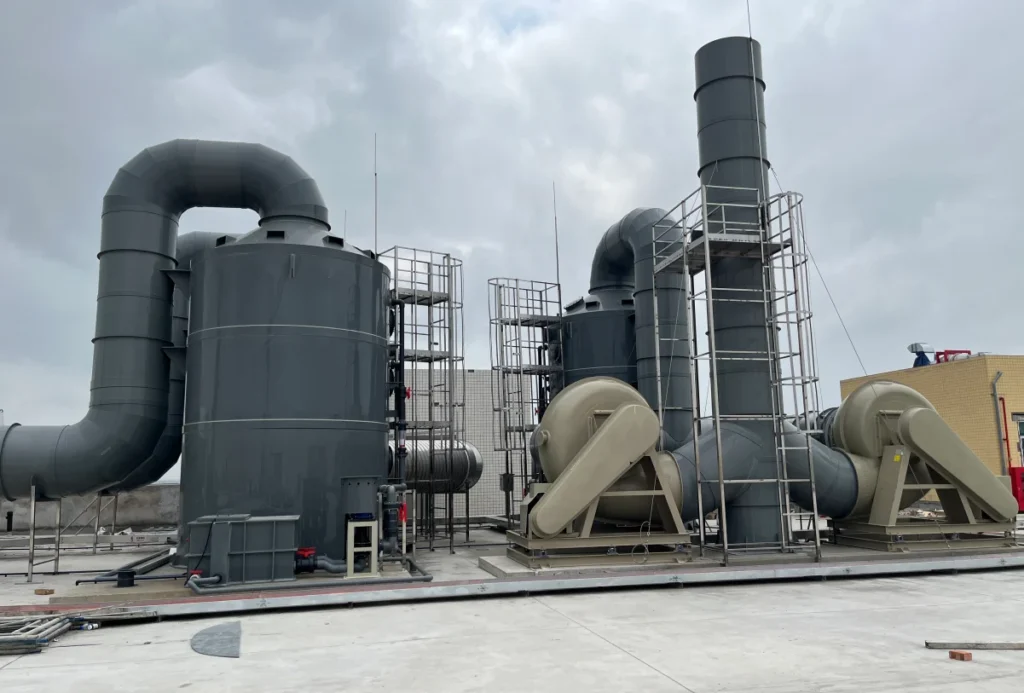
Sulfur dioxide (SO2) is the most widespread acid gas pollutant in the industrial world, emitted by coal-fired power plants, industrial boilers, chemical plants, refineries, and marine engines; electric power generators alone account for roughly two thirds of the SO2 in the atmosphere (US EPA, What is Acid Rain?). An so2 scrubber system is the standard technology for removing SO2 from exhaust streams, using either a limestone slurry (for large installations) or a caustic solution (for smaller plants) to chemically absorb the SO2 and convert it to a non-volatile sulfate or sulfite compound. This guide covers what an SO2 scrubber system is, the chemistry of limestone versus caustic scrubbing, the design parameters for scrubber vessel selection and sizing, the operating cost comparison between the two main reagents, and the applications across power generation, industrial boilers, and chemical processing.
Key Takeaways
- SO2 scrubber systems use either limestone slurry or caustic soda, and the choice is driven by plant size. Limestone costs approximately $0.02-0.05 per kg SO2 removed but requires slurry handling, forced oxidation, and gypsum dewatering equipment. Caustic costs $0.30-0.60 per kg SO2 removed but operates with clear solution chemistry, lower capital cost, and simpler maintenance. The economic crossover is at approximately 500 metric tons per year of SO2 removed.
- The pH setpoint directly controls the caustic consumption rate for an SO2 scrubber. At pH above 7, the reaction consumes 2 moles of NaOH per mole of SO2. At pH 5-7, it consumes 1 mole per mole. Operating at pH 6.5-7.0 balances removal efficiency (90-95%) against chemical cost, consuming approximately 40% less caustic than pH 8 operation.
- Spray towers dominate large FGD installations because they tolerate limestone slurry abrasion and scaling. Packed beds are the standard for caustic-based SO2 removal on clean gas streams. Venturi scrubbers serve applications requiring simultaneous fine particulate and SO2 capture. The trend in modern FGD design is to remove fly ash upstream of the SO2 absorber to produce cleaner gypsum and reduce vessel erosion.
- SO2 scrubbers inherently remove 50-80% of SO3 and coarse particulate, but cannot capture sub-micron acid mist. The visible blue haze from some FGD stacks is caused by sulfuric acid mist droplets (0.1-2 µm) that pass through the spray tower. A wet electrostatic precipitator downstream of the SO2 scrubber is the standard solution. For SO2 scrubber systems, see our SO2 gas scrubber products → and exhaust gas scrubber systems →.
What Is an SO2 Scrubber System?
An so2 scrubber system is a wet scrubber that removes sulfur dioxide from industrial exhaust gas by contacting the gas with an alkaline scrubbing medium (see our chemical scrubber system guide → for the broader scrubbing framework). The SO2 dissolves into the liquid phase and reacts with the alkaline reagent to form a non-volatile sulfite or sulfate salt that is removed from the system as a liquid blowdown or solid byproduct. The chemistry is different from HCl or HF scrubbing because SO2 is a moderately soluble gas whose absorption rate depends on both the liquid-phase pH and the gas-phase concentration.
How SO2 Scrubbing Differs from HCl or H2S Scrubbing
SO2 sits between HCl and H2S in terms of removal difficulty. HCl is highly soluble and reacts instantly with caustic at any pH above 7. H2S requires an oxidation step after absorption because it is a weak acid. SO2 requires neither an oxidant nor a special catalyst, but its absorption rate is pH-dependent: the reaction slows significantly below pH 5, and the solubility of SO2 in water is limited compared to HCl (8.5 g per 100 mL at 25 °C, with a Henry’s law constant of 8.10×10⁻⁴ atm·m3/mol; PubChem CID 1119).
A wet scrubber for so2 removal must provide adequate gas-liquid contact time (3-6 seconds) for the SO2 to dissolve and react. The mass transfer is controlled by the liquid-side resistance, meaning that increasing the L/G ratio improves removal more than increasing the gas velocity. This is the opposite of HCl scrubbing, where the gas-side resistance controls and the L/G ratio has a smaller effect.
The Three Main SO2 Removal Approaches
Limestone wet scrubbing uses a slurry of calcium carbonate (CaCO3) in water. The SO2 reacts with the limestone to form calcium sulfite (CaCO3 has a solubility product of 3.36×10⁻⁹ at 25 °C; PubChem CID 10112), which can be oxidized to gypsum (CaSO4-2H2O) – a salable wallboard raw material. Limestone is the cheapest reagent per mole of SO2 removed, at approximately $0.02-0.05 per kg of SO2. It is the standard reagent for power plant FGD systems above 100 MW.
Caustic soda scrubbing uses a sodium hydroxide (NaOH) solution. The SO2 reacts with NaOH to form sodium sulfite (Na2SO3). Caustic is more expensive than limestone ($0.30-0.60 per kg of SO2) but forms a clear solution rather than a slurry, eliminating the solids handling and scaling problems that limestone systems face. It is preferred for industrial boilers below 100 MW.
Seawater scrubbing uses the natural alkalinity of seawater to absorb SO2. The seawater is returned to the ocean after treatment. Seawater scrubbing is limited to coastal installations and requires large volumes of seawater but has the lowest operating cost of any FGD technology.
Limestone Wet Scrubber vs Caustic Scrubber vs Seawater
The choice between these three depends on plant size, reagent availability, waste disposal options, and the required removal efficiency. Limestone is the low-cost leader for large plants. Caustic offers simplicity for small plants. Seawater is lowest cost but is geographically constrained.
SO2 Scrubber Chemistry – Limestone vs Caustic vs Seawater
The chemical reactions for SO2 removal follow different paths depending on the reagent. Each path produces a different byproduct and has different operating cost implications.
Limestone (CaCO3) Reaction Chemistry
Limestone slurry absorbs SO2 in a two-step process. First, SO2 dissolves into the aqueous phase and reacts with water to form sulfurous acid:
SO2 + H2O -> H2SO3
The sulfurous acid then reacts with the dissolved calcium carbonate:
CaCO3 + H2SO3 -> CaSO3 + CO2 + H2O
The calcium sulfite (CaSO3) can be further oxidized by injecting air into the scrubber sump:
2 CaSO3 + O2 + 4 H2O -> 2 CaSO4-2H2O (gypsum)
Gypsum is a salable byproduct used in wallboard manufacturing; the EPA Acid Rain Program reports that flue gas desulfurization has helped deliver annual SO2 reductions of over 95% from the power sector (US EPA, Acid Rain Program Results). The quality of the gypsum depends on the residual calcium sulfite content and the chloride concentration in the scrubbing slurry. For wallboard-grade gypsum, the residual sulfite must be below 1% and the chloride below 200 ppm.
CaCO3 + SO2 -> CaSO3 + CO2 – Gypsum as Byproduct
The advantage of limestone over caustic is that limestone costs approximately $10-30 per metric ton compared to $400-600 per ton of NaOH equivalent, and the gypsum byproduct can offset 10-20% of the total FGD operating cost. The disadvantage is that limestone is a solid slurry (30-40% solids as-prepared, before dilution into the recirculating absorber loop) that requires slurry preparation equipment, presents scaling risk, and produces a solid waste stream (if gypsum is not sold).
Caustic (NaOH) Reaction Chemistry
Caustic scrubbing follows a pH-dependent stoichiometry. At pH above 7, the reaction consumes 2 moles of NaOH per mole of SO2:
SO2 + 2 NaOH -> Na2SO3 + H2O
At pH 5-7, the reaction shifts to single-mole stoichiometry:
SO2 + NaOH -> NaHSO3
The pH setpoint directly controls the operating cost. Operating at pH 6 (closer to the single-mole regime) consumes half the caustic of pH 8 but has a lower driving force for SO2 absorption. The economic optimum is typically pH 6.5-7.5, depending on the SO2 concentration and the local cost of NaOH.
2NaOH + SO2 -> Na2SO3 + H2O – pH-Dependent Stoichiometry
The sodium sulfite byproduct is fully soluble in water (30.7 g per 100 g water at 25 °C; PubChem CID 24437), so the caustic scrubber produces a clear blowdown stream without the solids handling requirements of a limestone system. The blowdown containing sodium sulfite/sulfate can be discharged to wastewater treatment, though some facilities aerate the sump to oxidize the sulfite to sulfate, reducing the chemical oxygen demand of the discharge.
Seawater Scrubbing Chemistry
Seawater contains natural bicarbonate alkalinity (approximately 140-160 mg/L as CaCO3 equivalent). Sulfur dioxide dissolves readily in water – 8.5% by weight at 25 °C (PubChem CID 1119) – which is what makes seawater scrubbing viable. SO2 absorbed into the seawater reacts with the alkalinity:
SO2 + H2O + 1/2 O2 -> H2SO4
HCO3- + H+ -> CO2 + H2O
The sulfuric acid produced by SO2 oxidation is neutralized by the seawater bicarbonate, and the resulting sulfate-enriched seawater is returned to the ocean. The pH of the discharge seawater is typically adjusted to 6.5-7.0 by air stripping and mixing with fresh seawater before discharge.
Reagent Selection – Limestone vs Caustic Decision Tree
The decision between limestone and caustic follows the plant size. For annual SO2 removal above approximately 500 metric tons per year, limestone is more economical despite the higher capital cost for slurry handling. For smaller loadings, caustic’s simplicity and lower capital cost make it the preferred choice. The crossover point in annual chemical cost is approximately $40,000-60,000 per year.
SO2 Scrubber Design Parameters
The design of an so2 scrubber system follows gas-liquid contact principles. An so2 scrubber system using limestone requires a spray tower with large-diameter nozzles to prevent plugging. A caustic-based so2 scrubber system can use a packed bed because the clear solution does not contain abrasive solids.
Scrubber Vessel Selection – Spray Tower vs Packed Bed vs Venturi
The spray tower is the standard vessel for limestone FGD systems because the open chamber handles the abrasive limestone slurry without plugging or erosion. A limestone spray tower operates at 0.3-1.2 m/s gas velocity with multiple spray levels (typically 3-5) to achieve the required contact time; the design basis for acid-gas packed and spray towers, including L/G ratio and mist-eliminator sizing, is set out in EPA Control Cost Manual, Section 5, Chapter 1: Wet Scrubbers for Acid Gas. The limestone slurry at 5-15% solids in the recirculating absorber loop is recirculated through large-diameter spray nozzles (25-50 mm) designed to resist erosion and plugging.
A packed bed scrubber is the standard vessel for caustic-based SO2 removal where the inlet gas is clean of particulate. The packing provides 100-200 m2 of wetted surface per m3 of bed volume, which is necessary for efficient SO2 mass transfer because the driving force is smaller than for HCl. Packed bed depth is typically 2-4 meters.
A venturi scrubber is used when the exhaust contains both SO2 and fine particulate. The venturi captures the particulate at the throat while initiating SO2 absorption, and a downstream packed bed or spray tower completes the SO2 removal.
L/G Ratio and Tower Sizing
For a limestone spray tower with 3 spray levels treating 50,000 m3/h of flue gas at 0.8 m/s:
- Tower diameter: 4.7 m
- L/G ratio: 8-12 L/m3
- Recirculation rate: 50,000 x 10 = 500,000 L/h
For a caustic packed bed scrubber treating the same flow:
- Tower diameter: 3.8 m (at 1.2 m/s)
- L/G ratio: 2-5 L/m3
- Packing depth: 2-3 m of 25 mm polypropylene Pall rings
pH Control and Slurry Chemistry Management
For a limestone wet scrubber, the slurry pH is maintained at 5.0-6.0, the window in which limestone dissolution and SO2 absorption are both fast enough for economical operation (EPA Control Cost Manual, Sec. 5 Ch. 1). Below pH 4.5, SO2 absorption efficiency drops sharply because the sulfite concentration in the liquid approaches equilibrium with the gas-phase SO2. Above pH 6.0, limestone dissolution slows, and unreacted CaCO3 passes through the system without contributing to SO2 removal.
pH Setpoint – 5.0-6.0 for Limestone, 6-8 for Caustic
For caustic scrubbers, the pH setpoint is 6-8. At pH 6-7, the reaction follows the single-mole stoichiometry (NaHSO3), consuming half the caustic of pH >7 but providing a lower driving force for absorption. The economic pH setpoint for caustic SO2 scrubbing is typically 6.5-7.0.
Gypsum Scaling Prevention and Blowdown
Gypsum (CaSO4-2H2O) has a solubility of approximately 2.0 g/L in water at 20 °C. Precipitation is governed by the solubility product (Ksp) and local supersaturation rather than by a bulk TDS threshold, so gypsum begins to crystallise on internal surfaces once the dissolved calcium and sulfate concentrations exceed saturation, particularly on the mist eliminator and in the sump. Forced oxidation (air injection into the sump) converts calcium sulfite to gypsum, which precipitates as a slurry that is removed continuously from the system. The blowdown rate controls the chloride concentration, which must stay below 20,000 ppm to prevent chloride stress corrosion in the absorber vessel. Gypsum solubility is 0.2 g per 100 mL of water at 20 °C (PubChem CID 24928), so the absorber operates close to saturation and the margin to scaling is narrow.
Industrial Applications
Coal-Fired Power Plants – Large-Scale FGD
The single largest application for so2 scrubber system technology is flue gas desulfurization at coal-fired power plants – some power plants use scrubbers, or flue gas desulfurization equipment, to reduce the sulfur leaving their stacks (US EIA, Coal and the environment). Approximately 85% of FGD units installed in the United States are wet scrubbers, with roughly 79% using lime or limestone. A typical 500 MW coal unit produces flue gas at 1,500,000-2,000,000 m3/h containing 500-2,000 ppmv SO2; new solid-fuel-fired units are limited to 520 ng/J (1.2 lb/MMBtu) heat input under 40 CFR Part 60, Subpart Da. The FGD spray tower treats this gas in three to five spray levels with limestone slurry at L/G of 8-12 L/m3, achieving 90-98% SO2 removal. Wet and dry acid-gas scrubbers are documented at 95-99% removal in the EPA’s control-cost review (EPA, Wet and Dry Scrubbers for Acid Gas – Control Cost Manual Review).
The gypsum byproduct from a 500 MW plant is approximately 150,000 metric tons per year at 8,000 operating hours, which can be sold to wallboard manufacturers or used in cement production. The gypsum sales revenue offsets 10-20% of the total FGD operating cost.
Industrial Boilers Below 100 MW
Industrial boilers below 100 MW face a different economic calculation than large utility boilers. At this scale, the capital cost of a limestone slurry preparation system and the complexity of gypsum handling are difficult to justify. A caustic-based so2 scrubber system is the standard solution for industrial boilers, using a packed bed or spray tower with 5-10% NaOH solution at pH 6-8.
For a 50,000 m3/h industrial boiler flue gas at 500 ppmv SO2, the caustic consumption at pH 6.5 is approximately 40 kg/h of pure NaOH (39.997 g/mol; PubChem CID 14798). The annual chemical cost is approximately $326,000 at the 50% caustic price used in the cost section below. The simplicity of the so2 scrubber system – no slurry pumps, no gypsum dewatering – justifies the higher reagent cost at this scale.
Chemical Plants and Refineries
Chemical plants and petroleum refineries produce SO2 from sulfuric acid regeneration plants, sulfur recovery units, and catalyst regeneration processes. The SO2 concentration in these streams ranges from 200-5,000 ppmv – far above the OSHA permissible exposure limit of 5 ppm as an 8-hour time-weighted average (29 CFR 1910.1000 Table Z-1) –, often at elevated temperatures (150-400 °C). A quench section upstream of the scrubber cools the gas to saturation temperature before it enters the packed bed or spray tower.
Refinery sulfur recovery unit tail gas scrubbers typically use caustic or amine-based systems to reduce SO2 below 100 ppmv. In the power sector, coal-fired units must meet a 1.0 lb/MWh SO2 standard under 40 CFR Part 63, Subpart UUUUU (MATS). The spent caustic from refinery SO2 scrubbers contains sodium sulfite/sulfate and can be sent to the refinery wastewater treatment system.
Marine Diesel Engine Exhaust
The IMO 2020 sulfur cap regulations limit marine fuel sulfur content to 0.50% globally, down from 3.50%, with a stricter 0.10% limit inside designated Emission Control Areas (IMO, IMO 2020 – cleaner shipping for cleaner air). Ship operators can use high-sulfur fuel oil with an exhaust gas cleaning system (scrubber) rather than switching to low-sulfur fuel. Marine SO2 scrubbers use seawater or caustic in open-loop or closed-loop configurations. The scrubber must handle the ship motion, load variations from 10-100% engine power, and the limited space available for the scrubbing system. More than 4,000 ships have installed SO2 scrubbers since 2020 to comply with the IMO regulations.
Wet Scrubber for SO2 Removal – Operating and Cost Considerations
The operating cost of a wet scrubber for so2 removal is dominated by the reagent cost, which varies by a factor of approximately 10 between limestone and caustic systems. Understanding the cost drivers is essential for selecting the right technology.
Operating Cost Comparison – Limestone vs Caustic
| Cost Component | Limestone (Large FGD) | Caustic (Small Boiler) |
|---|---|---|
| Reagent cost per kg SO2 removed | $0.02-0.05 | $0.30-0.60 |
| Capital cost per m3/h gas flow | $50-150 | $30-80 |
| Solids handling cost | $0.01-0.03/kg SO2 | None |
| Waste stream | Gypsum (solid) | Sodium sulfite (liquid) |
| Complexity | High (slurry + dewatering) | Low (solution only) |
Annual Chemical Cost Calculation
The annual chemical cost follows from the reaction stoichiometry and the local reagent price:
For a caustic scrubber treating 500 ppmv SO2 at 50,000 m3/h with 95% removal at pH 6.5:
Inlet SO2 load (before removal efficiency, at 25 °C molar volume): 50,000 x (500 x 64/24.45) / 1,000,000 = 65.4 kg/h
NaOH consumption at 1:1 ratio: 65.3 x 40/64 = 40.8 kg/h pure NaOH
At 50% delivery concentration: 40.8 / 0.50 = 81.6 kg/h of 50% caustic
Annual cost at $500/tonne: 81.6 x 8,000 x $500 / 1,000 = $326,400/year
Worked Example: 500 ppmv SO2 at 50,000 m3/h
For a limestone system removing the same SO2 mass:
Limestone consumption (CaCO3): 65.3 x 100/64 = 102 kg/h
At $20/tonne: 102 x 8,000 x $20 / 1,000 = $16,320/year
Gypsum production: 65.3 x 172/64 = 171 kg/h
Gypsum value at $8/tonne: 171 x 8,000 x $8 / 1,000 = $10,944/year
Net limestone cost after gypsum credit: $16,320 – $10,944 = $5,376/year
On a net-of-gypsum-credit basis, the limestone system’s reagent cost is approximately 60x lower than the caustic system’s gross reagent cost, but the capital cost is higher and the operating complexity is significantly greater.
Waste Management – Gypsum vs Sodium Sulfite
Limestone FGD systems produce solid gypsum that can be sold or landfilled. Caustic systems produce a liquid blowdown containing sodium sulfite/sulfate that must be discharged to a permitted wastewater treatment system. The disposal cost for liquid waste ranges from $0.50-5.00 per 1,000 L depending on local regulations, adding $5,000-50,000 per year to the caustic scrubber operating cost.
SOx Scrubber System – Multi-Pollutant Control
An sox scrubber system is designed to handle multiple sulfur oxide pollutants simultaneously – primarily SO2 and SO3, which together are referred to as SOx. An sox scrubber systems installation typically captures 90-98% of SO2 and 50-80% of SO3 in a single vessel. In practice, most SO2 scrubbers also capture 50-80% of the SO3 present in the flue gas, though the small fraction of SO3 (typically 0.5-2% of total SOx) forms a sulfuric acid mist that is difficult to remove.
Combined SO2 and NOx Removal
Some sox scrubber systems are designed to remove NOx in addition to SO2. The most common approach is to add an oxidizing agent (H2O2, O3, or NaOCl) to the scrubbing solution to convert NO to NO2, which then dissolves and reacts with the alkaline reagent. Combined SO2/NOx systems achieve 90-98% SO2 removal and 50-80% NOx removal. The cost of the oxidizing agent typically adds 30-60% to the total chemical cost compared to SO2-only scrubbing.
SO2 and Particulate Simultaneous Removal
Wet scrubbers inherently capture some particulate while absorbing SO2. The particulate removal efficiency depends on the scrubber type and the particle size distribution. A venturi scrubber handling fly ash-laden boiler exhaust captures 95-99% of fine particulate while absorbing 90-95% of SO2. A spray tower designed for SO2 removal captures 50-80% of coarse particulate above 10 µm but is ineffective for sub-micron particulate.
The trend in modern FGD design is to remove fly ash upstream of the SO2 scrubber in an electrostatic precipitator or baghouse, rather than attempting to remove both in the same vessel. This produces a cleaner gypsum byproduct (uncontaminated by fly ash) and reduces erosion of the spray tower internals.
SO3 and Acid Mist Control
Approximately 0.5-2% of the sulfur in the fuel oxidizes to SO3 during combustion. The SO3 combines with water vapor in the flue gas to form sulfuric acid mist (H2SO4), which condenses as fine droplets below approximately 200 °C. These droplets are too small (0.1-2 µm) for spray towers to capture by inertial impaction. The visible blue haze often seen from FGD-equipped stacks is caused by sulfuric acid mist. Wet electrostatic precipitators are increasingly installed downstream of FGD scrubbers to remove the acid mist.
Frequently Asked Questions
What is an SO2 scrubber system?
An so2 scrubber system is a wet scrubber that removes sulfur dioxide from industrial exhaust gas using an alkaline reagent – typically limestone slurry for large systems, caustic soda for smaller systems, or seawater for coastal installations.
What is the difference between a limestone wet scrubber and a caustic wet scrubber?
A limestone wet scrubber uses a calcium carbonate slurry that reacts with SO2 to form calcium sulfite, which can be oxidized to gypsum. The reagent is cheap ($0.02-0.05 per kg SO2) but the system is complex, requiring slurry handling and solids dewatering. A caustic scrubber uses sodium hydroxide solution, which costs 10x more per kg of SO2 removed but is simpler to operate with clear solution chemistry.
What removal efficiency can an SO2 scrubber achieve?
Wet FGD systems achieve 90-98% SO2 removal. Spray towers in utility power plants achieve 90-95% with 3-5 spray levels. Packed bed scrubbers with caustic achieve 95-98% at moderate L/G ratios.
How much does an SO2 scrubber cost to operate?
The operating cost is dominated by the reagent. For a 50,000 m3/h boiler at 500 ppmv SO2 with 95% removal, a caustic system costs approximately $326,000 per year in chemical, while a limestone system costs approximately $16,000 per year in reagent with a $10,000 per year gypsum credit.
What is the difference between an SO2 scrubber and an SOx scrubber?
An SO2 scrubber targets sulfur dioxide specifically. An sox scrubber system handles both SO2 and SO3, and in some configurations also removes NOx and particulate. The term SOx (sulfur oxides) encompasses both SO2 and SO3. Both sox scrubber systems and SO2 scrubbers use similar hardware; the SOx designation indicates multi-pollutant capability.
Sources
- U.S. Environmental Protection Agency – Acid Rain Program Results (the Acid Rain Program has helped deliver annual SO2 reductions of over 95% and annual NOx reductions of over 89%; wet sulfate deposition fell by more than 70% between 1989-1991 and 2020-2022).
- U.S. Environmental Protection Agency – What is Acid Rain? (two thirds of SO2 and one fourth of NOx in the atmosphere come from electric power generators; acid rain usually has a pH between 4.2 and 4.4).
- U.S. Environmental Protection Agency, Control Cost Manual (7th ed.) – Section 5, Chapter 1: Wet Scrubbers for Acid Gas (design basis for packed-bed and spray-tower acid-gas absorbers, including L/G ratio, packing depth and mist-eliminator sizing).
- U.S. Environmental Protection Agency – Wet and Dry Scrubbers for Acid Gas – Control Cost Manual Review (wet and dry acid-gas scrubbers are documented at 95-99% SO2 removal).
- U.S. Energy Information Administration – Coal and the environment (some electric power plants use scrubbers (flue gas desulfurization equipment) to reduce the amount of sulfur exiting their smokestacks).
- International Maritime Organization – IMO 2020 – cleaner shipping for cleaner air (from 1 January 2020 the global upper limit on the sulphur content of ships’ fuel oil is reduced to 0.50% (from 3.50%); inside designated Emission Control Areas the limit is already 0.10%).
- U.S. National Library of Medicine, PubChem (CID 1119) – Sulfur dioxide (solubility in water 8.5% at 25 °C (11.9% at 15 °C); Henry’s law constant 8.10×10⁻⁴ atm·m3/mol at 25 °C; molecular weight 64.07; boiling point −10 °C).
- U.S. National Library of Medicine, PubChem (CID 24928) – Calcium sulfate dihydrate (gypsum) (solubility 0.2 g per 100 mL water at 20 °C (2.0 g/L); density 2.32 g/cm3; molecular weight 172.17).
- U.S. National Library of Medicine, PubChem (CID 10112) – Calcium carbonate (solubility product constant 3.36×10⁻⁹ at 25 °C; molecular weight 100.09).
- U.S. National Library of Medicine, PubChem (CID 14798) – Sodium hydroxide (solubility in water 109 g per 100 mL at 20 °C; molecular weight 39.997).
- U.S. National Library of Medicine, PubChem (CID 24437) – Sodium sulfite (solubility 30.7 g per 100 g water at 25 °C; molecular weight 126.05).
- U.S. National Library of Medicine, PubChem (CID 23665763) – Sodium bisulfite (molecular weight 104.06; soluble in 3.5 parts cold water and 2 parts boiling water).
- U.S. Occupational Safety and Health Administration / eCFR – 29 CFR 1910.1000 – Air Contaminants (Table Z-1) (sulfur dioxide (CAS 7446-09-5) permissible exposure limit 5 ppm (13 mg/m3) as an 8-hour time-weighted average).
- U.S. Environmental Protection Agency / eCFR – 40 CFR Part 60, Subpart Da – Electric Utility Steam Generating Units (solid or solid-derived fuel units limited to 520 ng/J (1.2 lb/MMBtu) heat input SO2; new units also limited to 97% reduction or 1.0 lb/MWh gross output).
- U.S. Environmental Protection Agency / eCFR – 40 CFR Part 63, Subpart UUUUU – Mercury and Air Toxics Standards (MATS) (coal-fired units: sulfur dioxide 1.0 lb/MWh, measured by SO2 CEMS).
- U.S. Environmental Protection Agency / eCFR – 40 CFR Part 1043 – Control of NOx, SOx and PM from Marine Diesel Engines (fuels not meeting the applicable fuel sulfur limits of Regulation 14 of MARPOL Annex VI may be used only where certified equivalent emission controls are fitted).