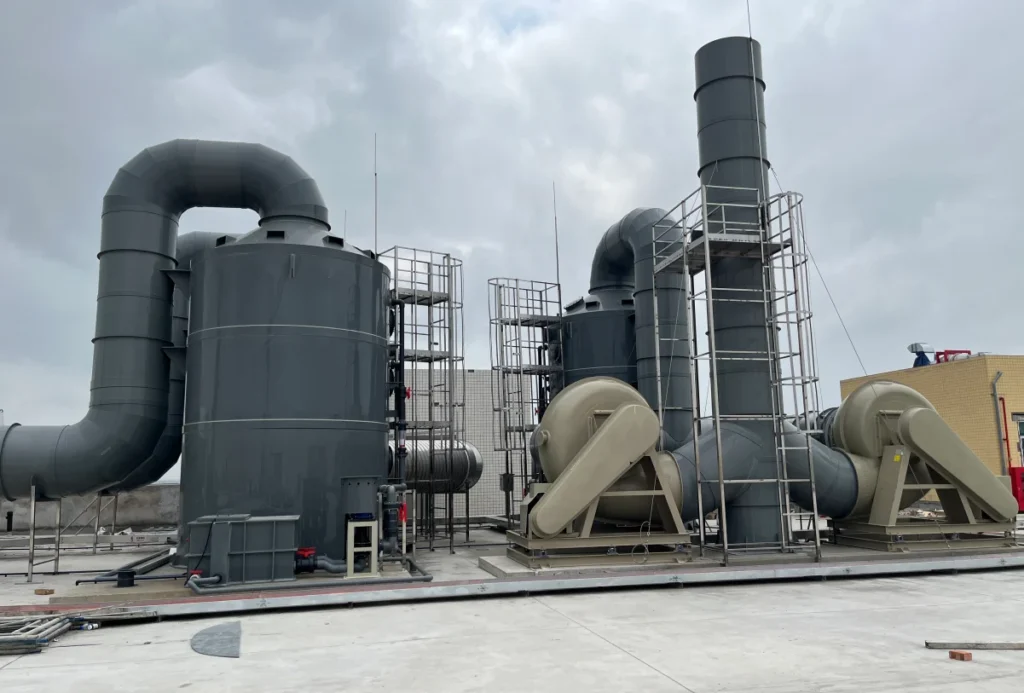
A plant manager facing an acid gas emission limit has a choice: install more mass-transfer surface area, or make the scrubbing liquid chemically reactive toward the target pollutant. A chemical scrubber system takes the second approach. Instead of relying on the physical solubility of the pollutant in water, a chemical scrubber uses a reactive reagent – sodium hydroxide, sulfuric acid, sodium hypochlorite – to convert the pollutant to a non-volatile, non-toxic salt or oxidation product. This guide covers what chemical scrubber systems are, how the four main categories of chemical scrubbing work, the system components and design parameters, and the specific industrial applications where chemical scrubbing is the only practical way to meet emission limits.
Key Takeaways
- A chemical scrubber system achieves higher removal efficiency than physical absorption alone by using a reactive scrubbing liquid that chemically converts pollutants to non-volatile compounds. The four categories – acid-base neutralization, oxidation, alkaline gas scrubbing, and specialty reactive scrubbing – cover the full range of industrial gaseous pollutants from HCl and SO2 to H2S, Cl2, and NH3.
- Chemical consumption is calculated from reaction stoichiometry, not estimated from rules of thumb. For HCl scrubbing with NaOH, 1 mole of caustic neutralizes 1 mole of HCl. For SO2 at pH above 7, 2 moles of NaOH per mole of SO2. For H2S oxidation with NaOCl, 4 moles of hypochlorite per mole of H2S. The annual chemical cost is a recurring operating expense that must be budgeted for the equipment’s service life.
- pH control is the single most critical operating parameter. A deviation of 0.5 pH units from the setpoint can reduce removal efficiency by 10-20%. Redundant pH sensors with weekly calibration, automated reagent metering, and a 1.5-2.0x stoichiometric design margin on the chemical feed pump are standard design practice.
- The scrubber vessel type (spray tower, packed bed, or venturi) is chosen based on the gas stream characteristics, not the chemistry. A packed bed provides the highest mass transfer for gas absorption but requires a clean gas stream. A spray tower tolerates particulate and fouling but provides less contact area. A venturi handles fine particulate and high temperatures. The chemical reagent system is largely independent of the vessel choice. For tailored scrubbing solutions, see our chemical waste gas treatment →.
What Is a Chemical Scrubber System?
A chemical scrubber system is a wet scrubber that uses a chemically reactive scrubbing liquid to remove gaseous pollutants (see our spray tower scrubber guide → for hardware fundamentals). The chemical reaction converts the pollutant into a neutral, non-volatile compound that remains dissolved in the liquid phase, preventing it from re-entering the gas stream. This is fundamentally different from a physical absorption scrubber, where the dissolved pollutant remains in equilibrium with the gas phase and can be stripped back out if conditions change.
How Chemical Scrubbing Differs from Physical Absorption
In a physical absorption scrubber, the pollutant dissolves into the scrubbing liquid according to Henry’s law: the equilibrium concentration in the liquid is proportional to the partial pressure in the gas. For the acid gases this guide covers, that solubility is low – the standard compilation gives SO2 a Henry’s law solubility constant of about 1.2 x 10⁻² mol/(m3 Pa) at 298 K, equivalent to roughly 46 atm per mole fraction (R. Sander, Henry’s Law Constants – Sulfur Dioxide). Once the liquid approaches saturation, absorption stops. For gases with low water solubility (SO2, H2S, Cl2), physical absorption with water alone cannot achieve high removal efficiency regardless of how much packing surface or how many spray stages are provided.
A chemical scrubber system solves this by consuming the dissolved pollutant through a chemical reaction. The reaction product – typically a dissolved salt or oxidized compound – has essentially zero vapor pressure, so it cannot re-enter the gas phase. The effective liquid-side concentration of the unreacted pollutant remains near zero regardless of how many moles have been absorbed. This sustains the maximum possible driving force for mass transfer across the gas-liquid interface.
The Four Chemical Scrubbing Categories
Chemical scrubbing systems fall into four categories based on the reaction mechanism:
Acid-base neutralization uses an alkaline reagent (NaOH, Ca(OH)2, Na2CO3) to neutralize acid gases (HCl, HF, SO2, NOx). The reaction produces a dissolved salt – NaCl, NaF, Na2SO3 – that is discharged in the blowdown stream. This is the most common category, accounting for the majority of installed chemical scrubber systems.
Oxidation scrubbing uses an oxidizing agent (NaOCl, H2O2, KMnO4) to convert reduced pollutants (H2S, mercaptans, sulfides) to oxidized, non-odorous forms (sulfate, disulfides). Oxidation scrubbing is the standard technology for odor control applications.
Alkaline gas scrubbing uses an acidic reagent (H2SO4) to neutralize alkaline gases (NH3, amines). This is less common than acid gas scrubbing but is essential in fertilizer manufacturing and some chemical processes.
Specialty reactive scrubbing uses reagents tailored to specific pollutants – sodium bisulfite for chlorine, caustic and hypochlorite for cyanide, ferric chloride for phosphate – that do not fit the standard acid-base or oxidation categories.
How Chemical Scrubber Systems Work – Chemistry Fundamentals
The chemical reactions inside a scrubber follow predictable stoichiometry. Understanding the molar ratios and the resulting salt concentrations allows the designer to calculate reagent consumption rates, blowdown volumes, and annual chemical costs.
Acid-Base Neutralization
The most common chemical scrubbing reactions involve the neutralization of acid gases with sodium hydroxide:
HCl + NaOH -> NaCl + H2O
One mole of NaOH neutralizes one mole of HCl. For an exhaust stream containing 200 ppmv HCl at 10,000 m3/h, the stoichiometric NaOH consumption is approximately 3.3 kg/h of pure NaOH. The molar masses behind that ratio are 36.46 g/mol for HCl and 39.997 g/mol for NaOH (PubChem CID 313; PubChem CID 14798), so one kilogram of HCl consumes about 1.10 kg of NaOH. At 5% NaOH concentration in the recirculating liquid, the minimum blowdown to prevent NaCl precipitation (at approximately 100,000 ppm TDS) is approximately 33 L/h.
SO2 + 2 NaOH -> Na2SO3 + H2O (at pH > 7)
SO2 + NaOH -> NaHSO3 (at pH 5-7)
The first reaction consumes two moles of NaOH per mole of SO2; the second consumes one mole. The pH is controlled between 6 and 8 to balance removal efficiency against reagent consumption. Below pH 5, absorption efficiency drops steeply.
HF + NaOH -> NaF + H2O
The reaction product NaF has limited solubility (approximately 40 g/L at 20 deg C), and precipitation can occur in the sump and on spray nozzles if the blowdown rate is inadequate. PubChem’s hazard summary puts the maximum solubility of sodium fluoride in water at room temperature at 4.2 g per 100 g of water (PubChem CID 5235), consistent with the 40 g/L figure used here.
Cl2 + 2 NaOH -> NaOCl + NaCl + H2O
Chlorine scrubbing requires pH above 10 to ensure complete reaction and prevent chlorine release from hypochlorite decomposition. The reaction product – sodium hypochlorite – is a commercial bleach solution.
Oxidation Scrubbing
H2S removal typically uses a two-stage process: first absorb H2S into caustic at pH 9-10 to form NaHS, then oxidize with sodium hypochlorite to sodium sulfate:
H2S + NaOH -> NaHS + H2O
NaHS + 4 NaOCl -> Na2SO4 + 4 NaCl + H2O
The overall reaction consumes 4 moles of NaOCl per mole of H2S. Annual operating cost is dominated by hypochlorite consumption.
Mercaptan removal uses similar oxidation chemistry. Methyl mercaptan (CH3SH) is oxidized to dimethyl disulfide (CH3S-SCH3), which has a higher odor threshold and lower vapor pressure, reducing the nuisance impact of the discharge.
The Role of pH Control
In every chemical scrubber system, pH is the primary control variable. A pH sensor in the recirculation line provides the feedback signal for the reagent metering pump, which adjusts the reagent feed rate to maintain the pH setpoint. A deviation of 0.5 pH units from the setpoint can reduce removal efficiency by 10-20% for pollutants where the reaction rate is pH-dependent.
All chemical scrubber systems include a pH control loop with the following components: pH sensor(s) in the recirculation line, a pH controller (typically a PID loop in the PLC), a chemical metering pump with variable-speed drive or modulating valve, and a caustic or acid storage tank with level monitoring. EPA lists scrubber liquid pH among the parameters to monitor as an alternative to scrubber liquid outlet concentration, alongside specific gravity and makeup and blowdown rates (EPA, Monitoring by Control Technique – Wet Scrubber for Particulate Matter).
Chemical Scrubber System Components
A chemical scrubber system includes not only the scrubber vessel itself but the full suite of equipment needed to store, meter, and control the chemical reagent and to manage the reaction products.
Scrubber Vessel – Spray Tower, Packed Bed, or Venturi
The scrubber vessel for a chemical system can be any of the three standard wet scrubber types. The choice depends on the gas stream characteristics, not the chemistry:
Packed bed is the most common choice for chemical scrubbing because it provides the highest mass transfer efficiency per unit volume. EPA’s cost manual makes the same point in general terms, calling packed towers the most commonly used gas absorbers for pollution control (EPA Cost Manual, Section 5.2, Chapter 1). The packing creates the extended gas-liquid contact time needed for chemical reactions that are not instantaneous – SO2 neutralization, H2S oxidation, VOC absorption. Packed beds are used when the gas stream is clean (below 30 mg/Nm3 particulate). EPA’s fact sheet for the device says packed-bed scrubbers are more suitable for gas scrubbing than PM scrubbing and reports plugging as a serious problem because the packing is more difficult to access and clean than other scrubber designs (EPA-452/F-03-015).
Spray tower is chosen when the gas contains particulate or solids-forming contaminants that would plug a packed bed. An open spray tower with caustic injection achieves 95-99% removal of HCl and HF, where the reaction is fast enough that extended contact time is unnecessary. That range matches the vendor-estimated 95 to 99 percent removal EPA reports for inorganic gases in spray towers, and EPA notes spray towers are also less prone to fouling than other wet scrubber designs (EPA-452/F-03-016).
Venturi is used when the gas contains fine particulate and soluble acid gases simultaneously. The venturi captures the particulate and initiates the chemical reaction, with a packed bed or spray tower downstream for final gas polishing. EPA describes the same arrangement, noting that venturis are sometimes used as a pretreatment device to remove PM and prevent clogging of a downstream packed bed scrubber designed to collect primarily gaseous pollutants (EPA-452/F-03-017).
Chemical Reagent Storage and Metering
The reagent storage system must be sized for the consumption rate and the desired refill interval. A chemical plant scrubber consuming 5 kg/h of NaOH at 50% concentration uses approximately 240 kg/day of 50% caustic solution. A 5,000 L storage tank provides approximately 3 weeks of inventory.
The metering pump is typically a positive-displacement diaphragm pump with a turndown ratio of at least 10:1. Pump sizing is based on the stoichiometric requirement multiplied by a factor of 1.5-2.0 to handle concentration surges. The pump speed is controlled by the pH controller output.
pH Control Loop and Blowdown Management
The pH control loop is the most critical control system in any chemical scrubber. Redundant pH sensors are standard: one in the recirculation line for process control and one in the sump for monitoring and alarm. pH sensors in chemical scrubber service require weekly calibration and replacement every 3-6 months because the chemical environment gradually degrades the glass electrode.
Blowdown removes the reaction product salts from the recirculating liquid. The blowdown rate is set by the salt production rate and the target TDS limit:
Blowdown flow = Salt production rate / Target TDS
For an HCl scrubber producing 3.2 kg/h of NaCl with a TDS limit of 80,000 ppm, the blowdown rate is 3.2 / 0.08 = 40 L/h. A conductivity meter provides continuous TDS measurement. The blowdown is typically sent to the plant wastewater treatment system.
Acid Gas and Caustic Scrubbing Applications
Acid gas scrubbing with caustic solution represents the largest installed base of chemical scrubber systems. The applications span chemical manufacturing, metal finishing, semiconductor fabrication, and power generation.
HCl Scrubbing in Chemical Manufacturing
Hydrochloric acid manufacturing, chlorinated solvent production, and PVC manufacturing generate HCl-laden vent streams at concentrations from 100-5,000 ppmv. A packed bed scrubber with caustic solution at pH 7-9 achieves 99%+ removal. EPA’s fact sheet gives packed-bed inorganic-gas removal as 95 to 99 percent from vendor estimates, and for chemical manufacturing the MON rule sets the hydrogen halide and halogen HAP limit at an outlet concentration of 20 ppmv or less (EPA-452/F-03-015; 40 CFR Part 63, Subpart FFFF). The NaCl reaction product is highly soluble and discharged with the blowdown to the plant wastewater system.
The heat of absorption – approximately 74 kJ/mol for HCl dissolving in water – raises the liquid temperature in the scrubber. For high HCl concentrations above 2,000 ppmv, a heat exchanger on the recirculation loop or an increased fresh water makeup rate maintains the sump temperature below 50 deg C.
SO2 Removal in Power and Industrial Boilers
Coal-fired and oil-fired boilers use wet flue gas desulfurization with limestone or lime slurry – a chemical scrubbing process operating at pH 5-6. EPA’s FGD fact sheet gives control efficiencies of approximately 90 percent for limestone systems and up to 95 percent for lime systems, which are significantly more costly (EPA, Flue Gas Desulfurization Fact Sheet). The reaction produces calcium sulfite, which is oxidized to gypsum (CaSO4-2H2O) in the sump. A caustic-based SO2 scrubber operates at pH 6-8 and produces sodium sulfite/sulfate, which is more soluble than calcium salts and does not present the same scaling risk.
HF and Fluoride Gas Control
Hydrogen fluoride is generated in aluminum smelting, phosphate fertilizer production, and semiconductor etching. HF is highly toxic, with a permissible exposure limit of 3 ppmv (as fluoride). That is OSHA’s 8-hour time-weighted average for hydrogen fluoride, listed in Table Z-2 of the air contaminants standard (29 CFR 1910.1000 Table Z-2). Caustic scrubbing at pH 8-10 achieves 99%+ removal. The reaction product – sodium fluoride (NaF) – has limited solubility at approximately 40 g/L, and the blowdown rate must be sufficient to prevent NaF precipitation on packing surfaces and in the sump.
Chlorine, Ammonia, and Specialty Gas Scrubbing
Beyond the mainstream acid-base applications, chemical scrubbing addresses a range of specialty pollutants that require tailored reagent chemistry.
Chlorine Gas Emergency Scrubbing
Facilities that store or use chlorine gas – water treatment plants, pulp and paper mills, chemical manufacturing – install chlorine scrubbers as emergency containment systems. A chlorine gas leak into a storage room is contained by the ventilation system, which routes the room air through a packed bed scrubber operating with 10-15% NaOH solution at pH 10-12. The need for that containment is set by chlorine’s toxicity: OSHA’s air contaminant table lists chlorine with a ceiling limit of 1 ppm (29 CFR 1910.1000 Table Z-1).
The chlorine scrubber must handle the worst-case release at full rated flow for 30-60 minutes without external reagent supply. The caustic storage tank is sized for this contingency. The reaction – Cl2 + 2 NaOH -> NaOCl + NaCl + H2O – is exothermic (approximately 56 kJ/mol), and the sump temperature can rise 10-20 deg C within minutes during a release. A heat exchanger on the recirculation loop or a chilled water supply protects against excessive temperature rise.
Ammonia Removal
Ammonia (NH3) is generated in fertilizer production, livestock operations, and refrigeration systems. Because NH3 is a base, it is scrubbed with an acidic solution – typically sulfuric acid (H2SO4) at pH 2-4: Sulfuric acid scrubbing of ammonia has been studied experimentally; a pilot spray tower optimized for ammonia removal reached 97.92 percent removal using an H2SO4 scrubbing solution with three nozzle stages working together (Jafari et al., Atmospheric Pollution Research 9(4): 783-790, 2018).
2 NH3 + H2SO4 -> (NH4)2SO4
The reaction product – ammonium sulfate – is a valuable fertilizer that can be crystallized from the blowdown stream and sold, partially offsetting the acid consumption cost.
Odor Control Systems
Chemical scrubber odor control systems use a combination of caustic and oxidizing agents to destroy odor-causing compounds. These chemical scrubber systems are designed with two stages.
Stage 1 operates with sodium hypochlorite (NaOCl) at pH 8-10 to oxidize reduced sulfur compounds (H2S, mercaptans, dimethyl sulfide). Stage 2 operates with sodium hydroxide (NaOH) at pH 7-9 to absorb acid gases and the acid byproducts of the oxidation reactions in Stage 1.
Combined removal efficiency for odor-causing compounds is 90-98%, with the outlet achieving a dilution-to-threshold ratio below the local regulatory limit. Odor control is one place where the pollutant itself carries a regulated exposure ceiling: OSHA lists hydrogen sulfide with an acceptable ceiling concentration of 20 ppm and a 50 ppm peak for an 8-hour shift (29 CFR 1910.1000 Table Z-2). Operating costs for a 50,000 m3/h odor control system range from $15,000-40,000 per year including chemicals, electricity, and water.
Chemical Scrubber System Design Parameters
Designing a chemical scrubber system requires sizing the vessel for gas-liquid contact and sizing the chemical feed system for the reaction stoichiometry.
Sizing by Stoichiometry – Chemical Demand vs Hydraulic Demand
The chemical demand – the mass flow of reagent needed to neutralize the target pollutant – is calculated from the reaction stoichiometry. For most applications, the chemical demand is small relative to the hydraulic demand: the recirculation flow rate needed to distribute liquid evenly across the tower cross-section is 50-500 times larger than the stoichiometric minimum.
A practical rule is to maintain the recirculating liquid at 2-5% reagent concentration for acid gas scrubbing. This provides the buffering capacity to handle concentration surges while keeping the salt concentration low enough to prevent precipitation.
Material Selection for Chemical Service
The combination of acid gases, caustic solutions, and dissolved salts creates a corrosive environment that demands careful material selection: EPA’s cost manual reaches the same conclusion for corrosive service, noting that packed columns are preferred to plate towers where acids and other corrosive materials are involved because the tower can then be built of fiberglass, polyvinylchloride, or other less costly corrosion-resistant materials (EPA Cost Manual, Section 5.2, Chapter 1).
- Polypropylene (PP) is the most common material for chemical scrubbers up to 80 deg C. It resists HCl, NaOH, and most salt solutions.
- FRP (vinyl ester) is specified for temperatures up to 110 deg C and for chlorine or strong oxidizer service where PP is chemically attacked.
- Stainless steel (SS316L) is used for high-temperature applications but is not recommended for HCl or HF service.
- PVC/CPVC is used for chlorine and hypochlorite service but is limited to 60 deg C.
Instrumentation and Control
Beyond the pH control loop, a chemical scrubber system should be instrumented with conductivity (for TDS monitoring), ORP (oxidation-reduction potential, for oxidation scrubbing applications), level sensors (sump and reagent tank), and flow meters (recirculation, makeup, blowdown, and reagent). A PLC collects all sensor data and controls the reagent feed, blowdown valve, and makeup water valve based on the setpoints.
Operation, Maintenance, and Safety
Chemical scrubber systems require more active operational attention than water-only scrubbers because the reagent chemistry must be maintained continuously.
Chemical Handling and Storage Safety
Concentrated caustic solutions (50% NaOH) and acids (98% H2SO4) are corrosive to skin and eyes. Regulations require secondary containment sized to the largest tank in the containment area: OSHA’s flammable-liquid standard states that the volumetric capacity of a diked area around an above-ground tank shall not be less than the greatest amount of liquid that can be released from the largest tank it encloses, assuming a full tank (29 CFR 1910.106(b)(2)(vii)(c)(1)). Chemical-plant engineering practice commonly sizes containment at 110 percent of tank capacity to leave freeboard for precipitation and firefighting water. Eyewash and emergency shower stations must be accessible within 10 seconds of the chemical feed pump area. Operators handling concentrated reagents wear chemical-resistant gloves, face shields, and aprons.
Monitoring Parameters
| Parameter | Instrument | Frequency | Target |
|---|---|---|---|
| pH | pH electrode | Continuous | 7-10 (acid gas) / 2-4 (NH3) |
| Conductivity | Conductivity cell | Continuous | <80,000 S/cm (typical TDS limit) |
| ORP | ORP electrode | Continuous | >400 mV (oxidation) |
| Reagent tank level | Level transmitter | Continuous | Refill at 20% |
Common Operating Problems
Salt precipitation occurs when the TDS exceeds the solubility limit of the reaction product. NaF precipitation in HF scrubbers, NaCl crystallization in HCl scrubbers at high blowdown concentration, and CaSO4 scaling in limestone FGD systems are all forms of this problem. Prevention requires adequate blowdown rate and TDS monitoring.
Foaming results from surfactants in the scrubbing liquid, which can enter from the process gas or form from the reaction products themselves. Anti-foam chemical injection or increased blowdown controls foaming. EPA’s list of the most common wet-scrubber operating problems overlaps directly: inadequate liquid flow, liquid re-entrainment, poor gas-liquid contact, corrosion, and plugged nozzles, beds, or mist eliminators (EPA, Monitoring by Control Technique – Wet Scrubber for Particulate Matter).
Reagent overfeed wastes chemical and can cause scaling. A failed pH sensor reading low causes the controller to inject excess reagent, raising the sump pH above the target range and potentially precipitating carbonates from the makeup water.
Frequently Asked Questions
What is a chemical scrubber system?
A chemical scrubber system uses a reactive scrubbing liquid – typically sodium hydroxide for acid gases, sulfuric acid for ammonia, or sodium hypochlorite for odor compounds – to chemically convert gaseous pollutants into non-volatile, non-toxic salts or oxidation products. The chemical reaction removes the equilibrium limitation that restricts physical absorption scrubbers.
How do I choose the right chemical reagent for my pollutant?
Match the reagent to the pollutant chemistry. Acid gases (HCl, HF, SO2, Cl2) require an alkaline reagent, typically NaOH. Alkaline gases (NH3, amines) require an acidic reagent, typically H2SO4. Reduced sulfur compounds (H2S, mercaptans) require an oxidizing reagent, typically NaOCl or H2O2. A reputable scrubber manufacturer can provide reagent recommendations based on a complete gas analysis.
What concentration of caustic should I use in the recirculating liquid?
Maintain 2-5% NaOH by weight in the recirculating liquid for acid gas scrubbing. Below 2%, the buffering capacity is too low for stable pH control. Above 10%, caustic carryover can cause scaling on the mist eliminator. The bulk storage concentration is typically 50% NaOH, which is diluted to the target concentration in the scrubber sump.
How do I calculate chemical consumption?
Calculate from the reaction stoichiometry. For HCl: 1 mole NaOH per mole HCl. For SO2: 2 moles NaOH per mole SO2 (pH >7). For Cl2: 2 moles NaOH per mole Cl2. Multiply the pollutant mass flow rate by the stoichiometric ratio and the molecular weight ratio (NaOH MW / pollutant MW). Add a 20-50% excess for control system response and concentration variations.
What is the most important instrumentation in a chemical scrubber?
The pH control loop is the single most important instrument. A drift of 0.5 pH units can reduce removal efficiency by 10-20%. Redundant pH sensors, weekly calibration, and a reliable chemical metering pump are essential design features.
Note on cost, consumption and equipment-life figures. The consumption, blowdown, storage, reagent-concentration, pH-tolerance, sensor-life and operating-cost figures quoted in this guide are Xicheng engineering estimates and typical vendor ranges, calculated from the assumptions stated alongside each example (gas flow, pollutant concentration, target TDS, reagent strength, utility rates), not published price data; actual values depend on the gas analysis, materials of construction, site conditions and scope. The volumetric inventory examples assume a scrubbing-solution density of about 1 kg/L, so for a 50 percent caustic solution – which is roughly 1.5 kg/L – the same mass of reagent occupies less volume and the refill interval is correspondingly longer. Where a figure comes from a published source, that source is linked inline and listed under Sources at the end of this article.
Sources
- U.S. EPA – EPA-452/F-03-015, Air Pollution Control Technology Fact Sheet: Packed-Bed / Packed-Tower Wet Scrubber.
- U.S. EPA – EPA-452/F-03-016, Air Pollution Control Technology Fact Sheet: Spray-Chamber / Spray-Tower Wet Scrubber.
- U.S. EPA – EPA-452/F-03-017, Air Pollution Control Technology Fact Sheet: Venturi Scrubber.
- U.S. EPA, Office of Air Quality Planning and Standards – Air Pollution Control Cost Manual, Section 5.2, Chapter 1: Wet Scrubbers for Acid Gas.
- U.S. EPA – Air Pollution Control Technology Fact Sheet: Flue Gas Desulfurization (FGD) for SO2 Control.
- U.S. EPA – Monitoring by Control Technique – Wet Scrubber for Particulate Matter (Air Emissions Monitoring Knowledge Base).
- U.S. eCFR – 40 CFR Part 63, Subpart FFFF: NESHAP for Miscellaneous Organic Chemical Manufacturing (MON).
- U.S. OSHA – 29 CFR 1910.1000 Table Z-1, Limits for Air Contaminants.
- U.S. OSHA – 29 CFR 1910.1000 Table Z-2 (hydrogen fluoride 3 ppm; hydrogen sulfide 20 ppm ceiling).
- U.S. OSHA – 29 CFR 1910.106, Flammable Liquids (diked area capacity, 1910.106(b)(2)(vii)(c)(1)).
- U.S. National Library of Medicine (NIH) – PubChem CID 14798: Sodium Hydroxide (molar mass 39.997 g/mol).
- U.S. National Library of Medicine (NIH) – PubChem CID 313: Hydrogen Chloride (molar mass 36.46 g/mol).
- U.S. National Library of Medicine (NIH) – PubChem CID 5235: Sodium Fluoride (solubility in water).
- R. Sander, Max-Planck Institute for Chemistry – Henry’s Law Constants: Sulfur Dioxide (CAS 7446-09-5), compilation published in Atmos. Chem. Phys. 23, 10901-12440 (2023).
- M. J. Jafari, A. H. Matin, A. Rahmati, M. Rezazadeh, D. Panahi – Experimental optimization of a spray tower for ammonia removal, Atmospheric Pollution Research 9(4): 783-790, 2018.