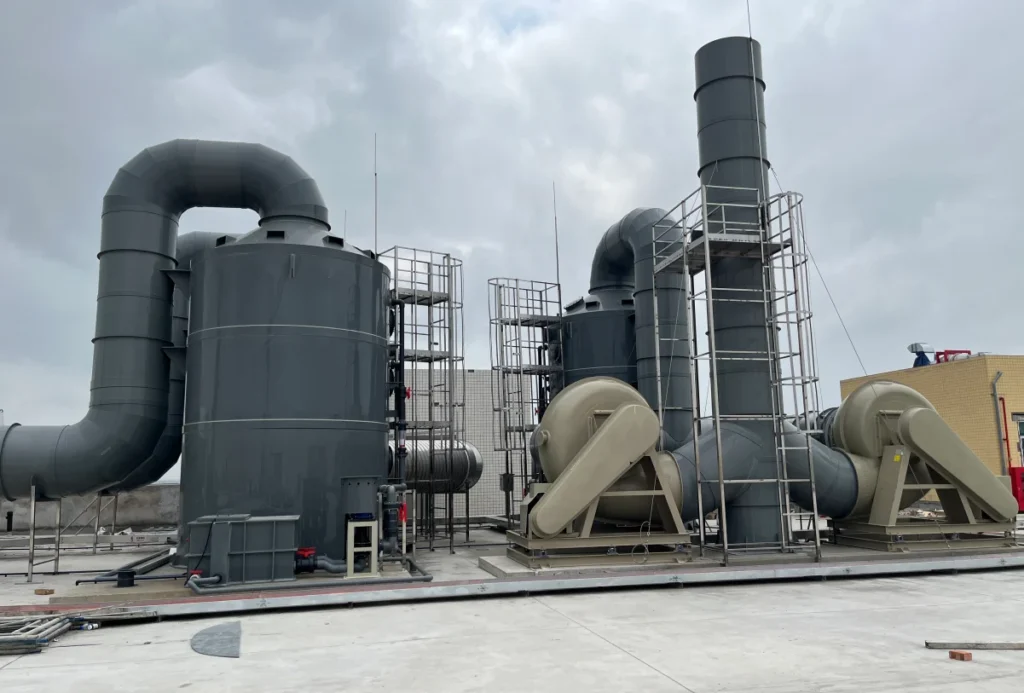
A scrubber sizing calculation answers one question: what size vessel removes what you need removed, from the gas stream you have. The word “scrubber” is what makes that question hard, because two pieces of equipment share the name and they are sized by two unrelated methods.
Search for a scrubber sizing calculation and you will find both methods side by side, with no label on either. A separator sizing sheet and an absorber sizing sheet use the same equation, quote capacity factors of the same order of magnitude, and produce numbers you cannot compare. This article separates them, gives you one ruler to check any velocity you are handed, and then works through the three calculations that most guides never show: the fan total pressure budget, the water balance, and the temperature correction on column diameter.
It stays at the level of method choice. For the full design walkthrough of a wet scrubber — flow regimes, internals, materials, and three worked geometry examples — start with our wet scrubber design guide. For the four interdependent calculations inside a packed tower specifically, see packed bed wet scrubber.
Key Takeaways
- A scrubber sizing calculation splits into two completely different chains, and the first decision is which one you are in. A gas–liquid separator is sized by settling velocity and liquid retention time. A wet scrubber absorber is sized by flooding velocity, HTU–NTU, and liquid-to-gas ratio.
- Both chains use the Souders–Brown equation with a capacity factor K. The K ranges nearly coincide — 0.15–0.40 ft/s for separators, 0.05–0.10 m/s for packed beds — but they set different physical limits. Copying a K value without its definition can put a packed column at six times its flooding velocity, and the diameter that follows is less than half what the service needs.
- Percentage of flooding is the one check that works on any quoted gas velocity. Convert first, judge second. Above 80% of flooding, a packed column sits on the vertical part of the pressure drop curve, where the next flow excursion is a step change rather than a gradual loss.
- A packed bed is not finished at the diameter calculation. The minimum wetting rate check fails on a first-pass design more often than not, and it forces either a higher L/G or a smaller column.
- Three numbers most published guides leave out: the itemized fan total pressure budget, the coupled recirculation / makeup / blowdown water balance, and the diameter change caused by an unquenched hot gas.
- Imperial and metric sources describe the same kind of vessel in units that do not land on standard shell sizes. A 42 in separator and a φ1.6 m absorber are not the same machine.
Two Devices Share the Name “Scrubber”
How to size a scrubber is not decided by what the equipment is called. It is decided by what the vessel has to remove. If the incoming gas carries liquid droplets that must not reach a compressor, a glycol contactor, or a custody meter, you are sizing a gas–liquid separator. If the incoming gas carries a contaminant that must be absorbed or neutralized, you are sizing a wet scrubber absorber. Same word in the inquiry, two different machines on the shop floor.
The Disambiguating Question: Liquid Droplets or a Gaseous Contaminant?
Ask three things about the stream. First, is the target entrained liquid, or a gas-phase species? Second, does the contaminant react with a scrubbing liquid, or does it merely need to be knocked out of the flow? Third, is there a chemical reagent in the loop at all? A separator runs on water or on whatever the process liquid happens to be. An absorber runs on a reagent whose concentration you have to control, which is why an absorber always arrives with a pH loop and a makeup line and a separator does not.
Gas flow rate alone tells you nothing. A 10,000 m³/h stream of natural gas carrying 0.3 barrel per MMSCF of condensate and a 10,000 m³/h stream of pickling-line exhaust carrying 120 mg/m³ of hydrogen chloride have the same volumetric flow and belong in different chapters of the same handbook.
What Each Chain Outputs
The output of the two chains is not comparable, which is the practical reason to separate them early. A separator calculation ends with a vessel inside diameter, a tangent-to-tangent height, a liquid retention time, and a mist eliminator selection. An absorber calculation ends with a column diameter, an active packing depth, a recirculation flow rate, a liquid distributor specification, and a pressure drop that sets the fan motor.
| What the stream carries | Which chain | Sizing parameter that controls | Final output |
|---|---|---|---|
| Entrained liquid droplets, no reagent | Chain A — gas–liquid separator | Maximum allowable settling velocity | Vessel ID, T–T height, retention time, demister type |
| Soluble or reactive gas, reagent loop | Chain B — wet scrubber absorber | Flooding velocity, then mass transfer depth | Column diameter, packing height, L/G, ΔP |
| Submicron particulate, no reagent | Neither — venturi service | Throat velocity and pressure drop | Throat diameter at 45–150 m/s, ΔP 2.5–20 kPa |
| Both droplets and a soluble gas | A then B, in series | Each chain sized independently | Separator plus absorber, two vessels |
One number carries over between the chains and only one: the actual volumetric gas flow, corrected for temperature and pressure. Everything downstream of that number diverges.
One Equation, Two K Factors: Souders–Brown in Both Chains
The Souders–Brown equation appears in both chains, which is the single largest source of confusion in scrubber sizing calculation work. It sets a maximum allowable superficial gas velocity from the density difference between the two phases. What changes between chains is not the equation. It is the capacity factor K, and with it the physical limit the equation is protecting.
The Equation, in Both Unit Systems
In separator practice the equation is written Vmax = KSB × √[( ρL − ρG ) / ρG], with velocity in feet per second, densities in pounds per cubic foot, and KSB likewise in feet per second. In packed-bed practice the same equation appears as uflood = K × √[( ρl − ρg ) / ρg], with velocity in metres per second and K in metres per second.
The density term is dimensionless, so the equation is dimensionally consistent in either system. That is exactly why the error is easy to make: a K of 0.35 and a K of 0.06 look like the same kind of number, and both multiply the same square root.
K for Droplet Entrainment — Separator Service
In a separator, K caps the upward gas velocity so that liquid droplets can settle out against the rising flow instead of being carried into the outlet. The value depends on what internals you have and how much margin the service demands. The figures below follow the API 12J / GPSA Chapter 7 framing used across midstream separator work; both are paid standards rather than public documents, so they are named here rather than linked.
| Configuration | Mist eliminator | KSB, ft/s (default) | Range |
|---|---|---|---|
| Vertical | Wire mesh pad | 0.35 | 0.245–0.40 |
| Vertical | Vane pack | 0.25 | 0.18–0.29 |
| Vertical | None — gravity only | 0.15 | 0.105–0.17 |
| Horizontal | Wire mesh pad | 0.40 | 0.28–0.46 |
| Horizontal | Vane pack | 0.30 | 0.21–0.35 |
| Filter separator | Coalescing elements | 0.08–0.12 | separate sizing basis |
Two adjustments sit on top of that table. At pressures above 100 psig the density ratio falls and K is reduced by 0.01 per additional 100 psi, so a 600 psig mesh separator runs a correction factor near 0.86. Compressor suction service stays deliberately conservative, commonly K = 0.24–0.28 with wire mesh and a design velocity at or below 75% of Vmax.
K for Flooding — Packed-Bed Absorber Service
In a packed absorber, K caps the upward gas velocity so that the descending liquid film is not held up and blown back out of the bed. The failure mode is flooding, and the consequence is not a wet outlet but a column that cannot achieve its design efficiency at all. Packed-bed practice runs K = 0.05–0.10 m/s, with the lower end reserved for foaming systems and small packings and the upper end for structured packing and clean, non-foaming service. The U.S. EPA’s acid gas wet scrubber chapter treats the same flooding limit as the constraint that fixes packed-bed cross-section.
Converted to the same units, 0.05–0.10 m/s is about 0.16–0.33 ft/s. The separator table above starts at 0.15 ft/s and runs to 0.46 ft/s. The two ranges overlap almost completely.
Why the Two K Ranges Nearly Coincide While Their Meaning Does Not
The overlap is a coincidence of decades of derating practice, not a shared physical basis. A separator K of 0.35 ft/s protects against droplet carryover — the limit is whether a 200 µm droplet falls faster than the gas rises. A packed-bed K of 0.06 m/s protects against flooding — the limit is whether the gas can hold the liquid film in place against gravity inside a bed with a specific surface area near 100 m²/m³.
Nothing links the two numbers. A designer who lifts a K of 0.35 from a separator table and applies it to a packed absorber is sizing for droplets at a velocity roughly six times the flooding limit, and the column will flood on first start-up. That is the specific error this article exists to prevent, and it is the reason the next section gives you a ruler instead of another table.
The %-of-Flooding Ruler: One Number That Validates Any Velocity
Because gas velocities arrive from vendors, spreadsheets, and search results in incompatible units and under incompatible assumptions, the practical move is to stop trusting the velocity and start converting it. Percentage of flooding is the conversion. It turns any quoted superficial velocity into a statement you can accept or reject without knowing where the number came from.
Converting a Quoted Gas Velocity into % of Flooding
Three steps. Compute the flooding velocity from Souders–Brown using the K that belongs to your internals and chemistry. Divide the quoted velocity by that flooding velocity. Multiply by 100. The result is the operating point as a fraction of the limit, and everything else in the design follows from it.
The input that most often goes wrong is gas density, because it is the one property that changes with temperature and pressure while everyone is still working in normal cubic metres. Gas density at 35 °C and atmospheric pressure for a light stream sits near 1.15 kg/m³. Rise to 80 °C and it falls to about 1.0 kg/m³, which raises the flooding velocity and, as the last section shows, changes the column diameter.
The 80% Ceiling and the Failure Above It
Design operating points sit between 70% and 80% of flooding, already above the 60 to 70 percent of the gas flooding velocity that the U.S. EPA’s acid gas wet scrubber chapter reports for most packed towers. That band is not a safety factor bolted on at the end; it is where the pressure drop curve is still steep enough that a small flow increase costs a small pressure increase, not a large one. Above roughly 80%, the column is on the vertical part of the curve. A process upset, a fouled demister, or a 10% flow excursion takes it into flooding, and flooding is not a gradual loss of efficiency. It is a step change in liquid holdup, pressure drop, and outlet concentration at the same time.
The counter-error is just as real. Sizing far below 50% of flooding to gain margin produces an oversized shell whose liquid flux falls under the minimum wetting rate, which the packed-bed section below shows in full. The 70–80% band is a working width, not a direction to move in.
Applying the Ruler to a Contradiction in the Literature
Published figures for the design gas velocity in a packed scrubber span more than an order of magnitude, and the ruler is what makes them comparable. Figures around 1.5–3.0 m/s circulate for random packing. The U.S. EPA’s particulate wet scrubber chapter publishes 45 to 150 m/s for the narrowest cross-section of a venturi throat, where the limit is collection energy rather than flooding. Neither figure can be carried into a packed absorber without first being converted.
Take the packed-bed K of 0.06 m/s with a liquid density near 1,050 kg/m³ and a gas density near 1.15 kg/m³. The density ratio is 911, its square root is 30.2, and the flooding velocity is 1.81 m/s. Against that limit, a 1.5 m/s operating point is 83% of flooding and a 3.0 m/s operating point is 166%. The 1.5 m/s figure quoted for random packing therefore begins above the flooding velocity that the packed-bed K range is built on. Both cannot describe the same vessel, and the flooding ruler is what exposes it.
Worked Conversion — 10,000 m³/h at 35 °C
Take a 10,000 m³/h stream at 35 °C, ρg = 1.15 kg/m³, ρl = 1,050 kg/m³ (a 5% sodium hydroxide solution), and 50 mm polypropylene Pall rings with K = 0.06 m/s. Flooding velocity is 0.06 × 30.2 = 1.81 m/s. For a 1.4 m column the cross-section is 1.54 m², so the actual superficial velocity is 10,000 / (1.54 × 3,600) = 1.80 m/s — 99% of flooding, and unusable.
At φ2.2 m the cross-section is 3.80 m² and the velocity falls to 0.73 m/s, which is 40% of flooding. At φ1.6 m it is 1.38 m/s, or 76%. The ruler has now told you which of three candidate shells is the only one inside the working band, without any reference to which source supplied the velocity.
Chain A — Sizing a Gas–Liquid Separator Scrubber
A separator scrubber is a settling device. Gas enters through a side nozzle, slows down, and lets entrained liquid fall out while a mist eliminator catches what gravity alone will not. The sizing sequence is short and every step is a capacity check, not a chemistry calculation.
Step A1 — Maximum Allowable Velocity
Apply Souders–Brown with the K from the internals table. For a vertical separator with a standard wire mesh pad, K = 0.35 ft/s. Densities are the only other inputs: liquid density in pounds per cubic foot, gas density at operating conditions in pounds per cubic foot. The output, Vmax, is the superficial gas velocity at which the vessel stops separating.
Step A2 — The 75–85% Design Margin
Design velocity is 75% to 85% of Vmax. Compressor suction service sits at the bottom of that band deliberately, because the consequence of a liquid slug reaching a reciprocating compressor is valve damage, bent rods, and cracked cylinders, and the cost of that failure dwarfs the cost of a slightly wider vessel. Pipeline and meter-station service can use 80–85%.
Step A3 — Vessel Diameter and Standard Shell Sizes
Divide actual volumetric flow by design velocity to get the required cross-sectional area, then convert to a diameter. The result will not be a purchasable size. Standard vessel nominal diameters run in a fixed family — 12, 16, 20, 24, 30, 36, 42, 48, 54, 60, 66, 72, 84, and 96 inches — and the design rounds up to the next one. Rounding up lowers the actual velocity, which is why the final vessel usually operates well below its design margin. A vessel selected this way commonly lands near 60–65% of Vmax.
Step A4 — Liquid Retention Time and Level Bands
Separator scrubbers hold little liquid, so the liquid volume is set by retention time rather than by separation performance. Minimum retention is 1 to 3 minutes; compressor suction scrubbers use 1 to 2 minutes because little liquid is expected, while pipeline inlet scrubbers use 2 to 3 minutes because condensate slugs do arrive.
Below the calculated volume sits a mechanical floor that frequently governs the real liquid section height. Instrument nozzle spacing needs 6 inches minimum between high-high and normal level and another 6 inches between normal and low-low, with 12 inches preferred in each gap. Add 12 inches of clearance below the low-low-low level to the bottom tangent line. In light-liquid service the resulting mechanical minimum is often the whole liquid section.
Step A5 — Mist Eliminator Type Sets K
The demister choice and the K value are the same decision seen twice. A wire mesh pad gives the highest capacity factor and the lowest pressure drop but fouls in sticky service. A vane pack accepts a lower K in exchange for fouling tolerance and better performance at high liquid loads. Choosing the eliminator after finishing the diameter calculation means redoing the diameter calculation.
Worked Example — 15 MMSCFD to a 42 in Vessel
Take a vertical compressor suction scrubber at a gas gathering station. Flow 15 MMSCFD of natural gas at specific gravity 0.65; suction 200 psig; suction temperature 90 °F; expected liquid 0.3 barrel per MMSCF; gas density at conditions 0.72 lb/ft³; liquid density 45 lb/ft³; wire mesh pad with a conservative K = 0.26 ft/s.
Vmax = 0.26 × √[(45 − 0.72) / 0.72] = 0.26 × 7.84 = 2.04 ft/s. Apply the 75% margin: Vdesign = 1.53 ft/s. Convert the flow to actual conditions at 200 psig and 90 °F, which gives 754 ACFM, or 12.57 ft³/s. Required area is 12.57 / 1.53 = 8.22 ft², and the diameter is √(4 × 8.22 / π) = 3.24 ft, or 38.8 in. Round up to a 42 in vessel: area 9.62 ft², actual velocity 1.31 ft/s, which is 64% of Vmax.
The liquid section is negligible on volume — 15 × 0.3 = 4.5 barrels per day, or 0.00625 barrel over a 2 minute retention — so the height comes from mechanical clearances: 12 in below the low-low-low, 24 in of liquid section, 18 in of inlet nozzle zone, 36 in of gravity settling, 6 in of mesh pad, and 12 in of outlet clearance. Total tangent-to-tangent height 108 in, or 9 ft, giving an L/D of 2.6 inside the recommended 2:1 to 4:1 band.
Chain B — Sizing a Wet Scrubber Absorber
Wet scrubber sizing is a mass transfer problem. The vessel has to move a contaminant out of the gas phase and into a liquid phase, and that requirement adds three calculations a separator never needs: the depth of packing required, the liquid rate required to wet it, and the pressure drop that packing imposes. A scrubber sizing calculation for absorber service therefore runs six steps, and each one feeds the next.
Step B1 — Flooding Velocity to Column Diameter
Packed bed scrubber sizing starts the way every absorption design starts. Apply Souders–Brown with the packed-bed K, then derate to the 70–80% operating band the ruler section defined. The required cross-section is Q / (u × 3,600) with Q in cubic metres per hour and u in metres per second. The diameter follows as √(4A/π).
Round to a fabrication increment, not to a standard pipe size. Polypropylene columns are commonly built in 100 mm steps, so 1.61 m becomes φ1.6 m, and the rounding changes the actual velocity, which changes the flooding percentage, which is why the rounded value is the one you carry forward.
Step B2 — NTU from the Removal Target
Wet scrubber sizing depends on this number before it depends on packing. The number of transfer units measures how difficult the separation is, independent of what packing you choose. For a contaminant that reacts rapidly with the scrubbing liquid — hydrogen chloride with sodium hydroxide, ammonia with sulfuric acid — the interface reaction is effectively instantaneous, and NTU reduces to ln(Cin / Cout). A 90% removal target needs 2.3 transfer units, 95% needs 3.0, and 99% needs 4.6.
That last jump is the one that surprises project teams. Moving a permit requirement from 95% to 99% does not raise the packing height by 4%. It raises it by 53%, because the natural logarithm is not linear in the removal fraction. When a client asks whether the scrubber can be “upgraded later” to a tighter limit, this is the number that answers the question.
Step B3 — HTU from Packing and Chemistry
The height of a transfer unit is the depth of packing that achieves one transfer unit, and it is the least formula-driven part of the whole calculation. HTU comes from pilot data, vendor curves, or a published range matched to your packing size and chemistry. It is not derivable from first principles in a design office.
| Packing | Service | HTU, m |
|---|---|---|
| 25 mm random (Pall rings, IMTP) | Fast chemical reaction | 0.3–0.5 |
| 50 mm random (Pall rings, Super Intalox) | Fast chemical reaction | 0.4–0.6 |
| 76 mm random | Fast chemical reaction | 0.6–0.8 |
| Structured (Mellapak 250Y class) | Fast chemical reaction | 0.2–0.4 |
| 50 mm random | Physical absorption, water solvent | 1.0–2.0 |
Note the last row. Physical absorption costs two to four times the bed depth of chemical absorption with the same packing, because the liquid-phase resistance stops being negligible once there is no reaction consuming the dissolved species at the interface. A scrubber sizing calculation that borrows an HTU from a chemically reacting system and applies it to a water-only VOC absorber will undersize the bed by a factor of three.
Step B4 — Packing Height and Total Column Height
A packed bed scrubber sizing sheet is not finished at the diameter. Active packed height is NTU × HTU. To that add the space the packing cannot use: roughly 0.3 m above the bed for the liquid distributor and 0.3 m below for gas distribution, so a 1.5 m active depth becomes a 2.1 m packed section.
Then check the height-to-diameter ratio. Packed towers normally run H/D between 2 and 6. Below 2, gas distribution across the bed is poor and an open spray tower is often the better answer. Above 6, wind loading and mechanical stability start driving the structural design, and tall polypropylene columns need guy wires. A total column height near 4.8 m on a φ1.6 m shell gives H/D about 3.0, comfortably inside the band.
Step B5 — L/G Ratio and the Minimum Wetting Rate Check
The liquid-to-gas ratio sets the recirculation pump duty, and it has to satisfy two independent requirements at once. Chemistry sets a floor: enough reagent to neutralize the incoming contaminant, with 10% to 50% excess to keep a driving force across the interface. Hydraulics sets a second floor that is usually higher, and that one is the minimum wetting rate.
Wetting rate is not a suggestion. The transfer area in an NTU calculation is the wetted area of the packing, and dry packing contributes nothing to it. The minimum wetting rate is calculated as MWR = MWRfactor × ap, where ap is the packing’s specific surface area in square metres per cubic metre and the factor runs 0.08–0.12 m³/(h·m) for plastic and 0.15–0.25 for ceramic. The U.S. EPA’s acid gas wet scrubber chapter writes the same requirement in its own units — a minimum wetting rate of 0.85 ft²/hr for rings larger than 3 in. and for structured packing, and 1.3 ft²/hr for everything smaller — which for a packing with ap near 100 m²/m³ works out to about 8 and 12 m³/(m²·h). Those two ends are where the 0.08–0.12 factor range comes from. For 50 mm polypropylene Pall rings, which are smaller than 3 in., the governing figure is the top of the range: MWR ≈ 12 m³/(m²·h). The actual liquid flux is recirculation flow divided by column cross-section.
The Iteration Every First-Pass Design Needs
Work the numbers and the failing case appears immediately. At 10,000 m³/h with an L/G of 0.9 L/m³, liquid flow is 9.0 m³/h. On a φ1.6 m column with 2.01 m² of cross-section, flux is 4.5 m³/(m²·h) — under 40% of the 12 m³/(m²·h) the packing needs. The bed dries in bands and the column underperforms its NTU prediction by 30% to 60%.
Shrinking the column raises the flux on two counts at once, because flow stays the same while area falls — but the smaller shell also raises the gas velocity, and φ1.4 m already fails the flooding check at 99%. Raising L/G on the φ1.6 m shell keeps both checks inside their limits. At L/G = 2.5 L/m³ the liquid flow is 25 m³/h and the flux is 25 / 2.01 = 12.4 m³/(m²·h), just over the 12 m³/(m²·h) the packing needs. That is acceptable, but only with a distributor that delivers 40 to 60 pour points per square metre: at the minimum wetting rate a poor distributor leaves dry bands and a good one does not, which is why the distributor specification belongs in the design, not in the purchase order.
Step B6 — Pressure Drop and the Packing Factor
Packing pressure drop closes a scrubber design calculation that has already fixed diameter and depth. It is read from a vendor curve or estimated from the packing factor Fp at the design liquid load. For 50 mm polypropylene Pall rings Fp is about 52 m−1; 25 mm runs near 95 m−1; structured Mellapak 250Y class packing near 22 m−1. Packing factors are not universal constants: Fp is defined by the correlation it is published with, and the packing table in the U.S. EPA acid gas wet scrubber chapter linked above lists Fp = 25 ft−1 (about 82 m−1) for the same 2 in. polypropylene Pall ring, roughly 1.6 times the figure used here. At 70–80% of flooding, 50 mm random packing costs roughly 250–350 Pa per metre of depth.
Two corrections matter. Wet pressure drop runs 1.3 to 1.5 times dry pressure drop at an L/G near 2.5 L/m³, because the liquid film occupies void space the gas used to have. And a 10% error in the packing factor translates to a 15–20% error in predicted pressure drop near flooding, which is why the vendor figure beats a generic table at final design.
Worked Example — 10,000 m³/h HCl Packed Bed
Inputs: 10,000 m³/h at 35 °C from a pickling line, 120 mg/m³ hydrogen chloride, 95% removal required so the outlet stays under 6 mg/m³, 5% sodium hydroxide as the reagent, 50 mm polypropylene Pall rings. Packed bed and tray towers are the type the U.S. EPA lists for hydrogen chloride service, and the same document puts typical wet scrubber removal efficiency for such duties between 95% and 99%, so the 95% target used here sits at the low end of what this configuration routinely achieves.
Diameter: K = 0.06 m/s gives uflood = 1.81 m/s; at 75% the design velocity is 1.36 m/s; area 10,000 / (1.36 × 3,600) = 2.04 m²; diameter 1.61 m, rounded to φ1.6 m. Height: NTU = ln(120 / 6) = 3.0; HTU for 50 mm Pall rings with a fast reaction is 0.5 m; active depth 1.5 m, packed section 2.1 m. Liquid: the φ1.6 m shell sits comfortably on flooding but fails the wetting check at the default L/G of 0.9 L/m³, so the design keeps the shell and raises L/G to 2.5 L/m³, giving 25 m³/h of recirculation and a flux of 12.4 m³/(m²·h). The heavier liquid load lowers the flooding velocity, so the 76% figure above is a first-pass number — re-run the vendor flooding correlation at the final L/G before the shell is released. Pressure drop: 1.5 m of packing at 250–350 Pa/m gives 375–525 Pa, plus 100–150 Pa for the demister and nozzle transitions, for a system total near 500–700 Pa.
What This Chain Does Not Give You
It stops at the vessel. Nothing in the six steps above tells you what the fan has to overcome once the scrubber is connected to a hood, a duct run, and a stack, and nothing tells you how much water leaves the loop per hour. Those two gaps are the reason the next two sections exist, and they are the calculations that decide whether the installed system meets its guarantee.
The Unit Bridge: Imperial and Metric for the Same Vessel
Separator practice is imperial and absorber practice is largely metric, so any engineer working across both spends time converting. Most of the conversions are routine. Six of them cause disproportionate trouble, and each one appears in a scrubber sizing calculation at a point where an error survives all the way to fabrication.
| Quantity | Imperial | Metric | Where it bites |
|---|---|---|---|
| Superficial velocity | ft/s | m/s | K values look interchangeable across the two systems |
| Gas / liquid density | lb/ft³ | kg/m³ | 1 lb/ft³ = 16.02 kg/m³; only the ratio matters in Souders–Brown |
| Standard gas flow | MMSCFD | Nm³/h | The standard conditions differ: 14.696 psia & 60 °F vs 101.325 kPa & 0 °C |
| Liquid volume | barrel (bbl) | m³ | 1 bbl = 0.159 m³; retention times compound the error |
| Vessel diameter | inch (nominal) | mm / φ | Nominal and actual bore differ; PP is built on 100 mm steps |
| Pressure | psig | kPa | Feeds the GPSA K correction and the density |
The Six Conversions That Cause the Most Error
The standard-condition mismatch is the most expensive one, because it hides inside a flow rate that everyone treats as a given. 15 MMSCFD is 625,000 standard cubic feet per hour, which is 17,700 m³/h if you keep the 60 °F basis — and 16,700 Nm³/h once you correct it to 0 °C. Two figures, same gas, a 6% difference that carries into the density, the actual volumetric flow, and the diameter. A European datasheet quoting Nm³/h at 0 °C and 101.325 kPa is describing the second of those amounts, not the first.
Nominal diameter is the second. A 42 in vessel is a nominal outside designation, and polypropylene columns are fabricated on 100 mm internal steps. Nothing in the imperial family maps onto the metric family, so a separator sized to 42 in does not become a φ1.07 m absorber when you switch systems. It becomes a 42 in separator.
Why 42 in and φ1.6 m Are Not the Same Scrubber
A 42 in separator and a φ1.6 m absorber differ by more than a conversion factor. They differ in design velocity by nearly threefold — 1.53 ft/s against 1.36 m/s — in what sets the height, and in what the vessel contains. The separator’s height comes from liquid retention and mechanical clearances; the absorber’s height comes from transfer units. Put the same gas flow through both and you get two vessels of similar diameter and unrelated proportions.
That is why the unit bridge is worth a section, not a footnote. Getting the conversions right is necessary and not sufficient. The two chains remain two chains after the units match.
Fan Total Pressure Budget, Itemized
The fan is where a scrubber sizing calculation stops being about the vessel. The column pressure drop you computed in Step B6 is one line item in a budget that runs from the capture point to the stack exit, and a fan selected on packing pressure drop alone will run short on site.
The Seven Line Items
| # | Item | Typical allowance | Notes |
|---|---|---|---|
| 1 | Capture hood / enclosure | 50–150 Pa | Rises sharply if the hood is too far from the source |
| 2 | Branch ducts | 60–150 Pa | Per run; depends on length and bends |
| 3 | Main duct | 80–250 Pa | The largest variable in most retrofits |
| 4 | Packed bed | 375–525 Pa | 1.5 m active depth at 250–350 Pa/m, wet |
| 5 | Mist eliminator | 100–200 Pa | Wire mesh; rises as the pad loads |
| 6 | Silencer (if fitted) | 50–150 Pa | Often omitted from the first estimate, then added |
| 7 | Stack exit | 30–80 Pa | Exit velocity head plus stack friction |
Totals for a mid-sized packed absorber commonly land between 800 and 1,600 Pa once all seven items are counted, against the 500–700 Pa the column alone accounts for. A separator has a different profile: the demister dominates and the vessel itself is almost free, so the total is usually lower and less sensitive to the internals.
Item 1 is the one most often underestimated. The U.S. Occupational Safety and Health Administration’s ventilation investigation manual documents how rapidly capture velocity falls off as the hood moves away from the source, so a hood a short distance further from the process can cost more static pressure than the entire packed bed.
Wet versus Dry Pressure Drop
The packed-bed figure in the table is a wet pressure drop. Dry pressure drop through clean packing runs 1.3 to 1.5 times lower at an L/G near 2.5 L/m³, because the descending liquid film occupies void space. Using a dry figure to select the fan produces a system that cannot reach design flow on start-up, before any fouling has occurred.
Total Static Pressure to Fan Selection
Sum the seven items, add the plant’s own duct allowances, and then add a margin of 15% to 20% on both flow and pressure to cover capacity growth and filter loading. For the worked HCl example, a total near 900 Pa at 10,000 m³/h is an air power of (10,000 / 3,600) × 900 = 2.5 kW. With the 15% to 20% margin above and a fan efficiency in the 60% to 70% range, the shaft power lands near 4.5 kW and the selection is a centrifugal fan with a 4 to 5.5 kW motor.
The margin is not padding. Packing fouls, demisters load, and ducts accumulate deposits, all of which raise resistance over the life of the installation. A fan selected at exactly the calculated duty has no room to absorb that, and the first symptom is a scrubber that met its guarantee during commissioning and no longer does two years later. Pressure differential is one of the three primary performance indicators the U.S. EPA’s wet scrubber monitoring guidance names for an absorber, alongside scrubbing liquid flow rate and scrubber liquid outlet concentration — with scrubber liquid pH, specific gravity, and makeup and blowdown rates accepted as alternatives where the outlet concentration is not trended. The fan budget and the monitoring plan are the same set of numbers seen from two directions.
Water Balance: Recirculation, Makeup, and Blowdown
The water side of a scrubber sizing calculation is where a design either closes or quietly fails. The recirculation rate comes from the L/G ratio and is the number everyone computes. The makeup and blowdown rates come from what leaves the loop, and they are the numbers that decide whether the sump pump runs dry in August or the reagent concentration drifts out of range in month three.
Evaporation Loss
Gas leaving a scrubber is saturated at the outlet temperature, so the loop loses water at whatever rate the exhaust can carry it. That rate is the dry gas mass flow multiplied by the difference in humidity ratio between outlet and inlet:
E = mdry gas × ( xout − xin )
For a cold-gas absorber the difference is small and evaporation is nearly negligible. For a hot-gas duty the same equation produces a large number, because a gas entering at 150 °C dry and leaving saturated at 60 °C picks up roughly 0.15 kg of water per kg of dry gas. On 12,900 kg/h of dry gas that is about 1,900 kg/h, or 1.9 m³/h of evaporation — enough to matter for both the water supply and the sump level control.
Blowdown Rate from the Concentration Ratio
Every kilogram of water that evaporates leaves its dissolved solids behind. Without a deliberate bleed, dissolved salt, unreacted reagent, and accumulated chloride concentrate until they precipitate, scale the packing, and blind the distributor. Blowdown is the deliberate bleed that holds the concentration at a setpoint.
Where evaporation is the only route by which pure water leaves the loop, the balance is set by the concentration ratio N — the factor by which dissolved solids are allowed to concentrate relative to the makeup water:
B = E / ( N − 1 )
A concentration ratio of 3 is common where dissolved salt is the binding constraint. In a reactive scrubber there is a second source that the evaporation balance ignores entirely: the reaction itself manufactures dissolved solid. Scrubbing hydrogen chloride with sodium hydroxide produces sodium chloride at a rate set by the inlet loading, and in many acid-gas duties that salt production, not evaporation, is what fixes the blowdown rate.
Makeup = Evaporation + Blowdown
Makeup water replaces both losses and nothing else, so the equation is a sum, not a margin. Where a level control adds water on a float, the controller is implicitly setting the blowdown rate, which is why the concentration ratio in a real plant is often an accident of the level setpoint, not a design decision.
Worked Water Balance at 10,000 m³/h
Take a hot-gas quench duty: 10,000 Nm³/h of dry gas, 12,900 kg/h, entering at 150 °C and leaving saturated at 60 °C, with a recirculation rate of 25 m³/h from the L/G calculation. Evaporation is 1.9 m³/h. At a concentration ratio of 3, blowdown is 1.9 / (3 − 1) = 0.95 m³/h. Makeup is 1.9 + 0.95 = 2.85 m³/h, or about 11% of the recirculation rate.
That 11% is the number that catches people out. The recirculation pump circulates 25 m³/h continuously, and a makeup line sized on “a little topping up” cannot deliver 2.85 m³/h. Size the makeup line and the sump level control from the balance, not from a rule of thumb about the recirculation rate.
Temperature Correction on Column Diameter
Temperature is the variable that most often invalidates a scrubber sizing calculation that is otherwise arithmetically correct, because it changes the one property the diameter calculation depends on. Gas density falls as temperature rises, so a fixed mass flow occupies more volume, and the column has to be wider to keep the superficial velocity inside the flooding band.
Actual Volumetric Flow versus Mass Flow
Every manufacturer datasheet, permit condition, and fan rating uses a different flow basis, and only one of them sizes a vessel. Normal cubic metres describe a mass. Actual cubic metres describe a volume, and the vessel cares about volume:
Qactual = Qnormal × ( T / 273.15 ) × ( 101.325 / P )
with T in kelvin and P in kilopascals. A figure quoted in Nm³/h is a mass in disguise, and it must be converted before it touches Souders–Brown. This is the single most common basis error in a scrubber sizing calculation, and it is invisible because the units both say “per hour”.
The Diameter Scaling Rule
At a fixed design velocity, cross-sectional area scales with volumetric flow, so diameter scales with the square root of flow. Because flow scales with absolute temperature at constant pressure, diameter scales with the square root of absolute temperature:
D ∝ √T
The consequence is that diameter grows more slowly than temperature, which is reassuring but not licence to ignore it. Raising a gas from 35 °C to 80 °C raises absolute temperature by a factor of 1.146 and the diameter by a factor of 1.071 — about 7% wider for a 45 °C increase.
35 °C versus 80 °C at the Same Mass Flow
Take 10,000 Nm³/h — a normal basis, deliberately different from the actual 10,000 m³/h used earlier — and a design velocity of 1.36 m/s. At 35 °C the actual flow is 11,281 m³/h, the required area is 2.30 m², and the diameter is 1.71 m. At 80 °C the actual flow is 12,929 m³/h, the area is 2.64 m², and the diameter is 1.83 m.
Rounding to fabrication increments, the same scrubber sizing calculation run at two temperatures lands on a φ1.7 m column and a φ1.9 m column. Skip the correction and the 80 °C design is built as a φ1.7 m shell running at 87% of the flooding velocity it was supposed to operate at 75% of. That column floods.
When Temperature Forces a Material Change
Temperature decides the material at the same time it decides the diameter. Polypropylene is the default for acid-gas service on cost and chemical resistance grounds, but its structural margin falls away as process temperature approaches its ceiling. Above the limit the design has to step up, and each step costs.
| Material | Practical maximum | Relative cost | Acid resistance |
|---|---|---|---|
| Polypropylene (PP) | about 80 °C | 1× | Excellent |
| FRP, vinyl ester resin | 120–180 °C | 1.5–2× | Good |
| 304 stainless steel | 400 °C and above | 2.5× | Poor in chlorides |
| 316 / 316L stainless steel | 400 °C and above | 3.5× | Moderate |
| Hastelloy C276 | 400 °C and above | 15× and up | Extreme environments |
An unquenched 90 °C exhaust routed into a standard PP shell fails on two counts at once: the shell deforms, and the diameter was computed for the wrong density. A quench stage upstream solves the material problem and simultaneously lowers the temperature that the diameter calculation has to use, so the two effects work in the same direction rather than opposing each other.
One Input, Two Chains — A Side-by-Side Comparison
Run one scrubber sizing calculation input set through both chains and the separation becomes concrete. Take 10,000 m³/h at 35 °C, a gas density of 1.15 kg/m³, and a liquid density of 1,050 kg/m³ — and then decide what the stream contains.
The Shared Input Set
Both chains begin from the same five values: volumetric flow at actual conditions, gas density at operating temperature and pressure, liquid density, target performance, and available space. Everything after those five diverges, and no downstream value transfers.
Chain A Output versus Chain B Output
| Output | Chain A — separator, droplets | Chain B — absorber, HCl |
|---|---|---|
| Controlling velocity | 1.53 ft/s (75% of 2.04 ft/s) | 1.36 m/s (75% of 1.81 m/s) |
| Vessel size | 42 in ID, 9 ft tangent-to-tangent | φ1.6 m, about 4.8 m total height |
| Height set by | Liquid retention and clearances | NTU × HTU |
| Internals | Wire mesh demister, 6 in | 2.1 m packed section, 50 mm Pall rings, 40–60 pour points/m² |
| Liquid | 1–2 min retention | L/G 2.5 L/m³, 25 m³/h recirculation |
| Chemistry | None | 5% NaOH, 10–50% excess |
| Pressure drop | Demister-dominated | 500–700 Pa across the column |
Why the Two Outputs Are Not Interchangeable
A scrubber sizing calculation that outputs one of these vessels cannot be read as a specification for the other, and the reason is physical rather than dimensional. The separator has no packing, no reagent, and no transfer units. The absorber cannot tolerate the liquid loads a separator handles, because a packed bed floods.
Where the two get confused is in procurement. A separator drawing and an absorber drawing look similar on a general arrangement — a vertical cylindrical vessel with a side inlet and a top outlet — and the difference between them is internals and height, which is exactly what a general arrangement drawing does not show. If you are comparing quotes for a “scrubber”, the question to ask is which chain produced the sizing sheet.
When Both Are Needed in Series
Some streams need both, and then the two chains run one after the other rather than competing. A dirty exhaust carrying both abrasive particulate and a soluble gas is normally handled by a venturi to knock down the solids followed by a packed bed to absorb the gas. A wet gas carrying entrained liquid and a soluble contaminant is handled by a separator and then an absorber.
The order matters. Put the absorber first and the particulate blinds the packing; put the separator second and it has nothing left to separate. Size each vessel on its own chain and let the sequence do the integration.
Scrubber Type Quick Reference
Once you know which chain you are in, the geometry is the last choice. For the full comparison of packed bed, spray tower, venturi, and crossflow scrubber design calculation ranges — pressure drop, L/G, height, footprint, and relative cost — use our wet scrubber design guide. For the interior of a packed tower, see packed bed wet scrubber, and for spray tower liquid loading and velocity, see spray tower scrubber.
Five Errors That Break a Scrubber Sizing Calculation
Copying a K Factor Without Its Definition
The first thing to check in any scrubber sizing calculation is where the K came from and what limit it protects. A K of 0.35 ft/s from a separator table and a K of 0.06 m/s from a packed-bed table describe different failure modes, and taking the number 0.35 into the packed-bed equation puts the column at close to six times its flooding velocity — with a diameter that comes out less than half the size the service needs. Write the units and the internals next to every K you use.
Skipping the Minimum Wetting Rate Check
This is the error that survives spreadsheets, quotations, and fabrication and then appears at a stack test. A column that passes the diameter and height calculations and fails the wetting check loses 30% to 60% of its effective transfer area to dry bands, and the loss is invisible until the outlet is measured.
Using a Vendor’s Default HTU
HTU comes from data. A default value embedded in a calculator is a placeholder, and a placeholder borrowed from a chemically reacting system applied to a water-only physical absorption duty can undersize the bed by a factor of three. Get HTU from pilot data or from a range that matches both your packing size and your chemistry.
Sizing at 100% of Flooding
Sizing the vessel at the flooding velocity to save shell cost leaves no margin for a flow excursion, a fouled demister, or a fouling packing surface. The 70–80% band exists because the pressure drop curve is nearly vertical above it, and the transition into flooding is a step change rather than a gradual decline.
Ignoring the Temperature Effect on Density
An unquenched hot exhaust has a lower density, therefore a higher actual volumetric flow, therefore a larger diameter for the same mass flow. A 45 °C temperature rise moves the diameter about 7%. Treat temperature as both a hydraulic variable and a materials variable, because it decides the shell material at the same time it decides the width.
Frequently Asked Questions
How do I do a scrubber sizing calculation for a new project?
How to size a scrubber begins with deciding which chain you are in. If the stream carries droplets that must not reach downstream equipment, you are doing separator sizing: Souders–Brown for maximum velocity, a 75–85% margin, a diameter, and a retention time. If it carries a contaminant that must be absorbed, you are doing absorber sizing: flooding velocity for diameter, NTU × HTU for depth, L/G for liquid rate, and a minimum wetting rate check to validate the combination.
A complete scrubber sizing calculation then adds the fan total pressure budget and the water balance, because the vessel alone does not determine whether the installed system works.
Why do two sources give different gas velocities for the same packing?
Usually because one is quoting a velocity without stating the basis. A figure of 1.5–3.0 m/s for random packing sits at 83% to 166% of the flooding velocity that a K of 0.06 m/s and a density ratio of 911 define. A scrubber sizing calculation that quotes 1.5–3.0 m/s is either using a much higher capacity factor or omitting the flooding derating.
Convert both figures to percentage of flooding before comparing them. That is the only basis on which two published velocities can be judged against each other. The same gap appears in wet scrubber sizing guides that quote a design velocity without stating its flooding basis.
What is the K factor, and which table do I use?
K is the capacity factor in the Souders–Brown equation. It caps the superficial gas velocity at the point where the vessel stops separating liquid from gas. Use the separator table — 0.15 to 0.40 ft/s depending on orientation and internals — when the vessel has no packing and the limit is droplet entrainment. Use the packed-bed value of 0.05 to 0.10 m/s when the vessel contains packing and the limit is flooding.
The two tables are not alternatives for the same vessel. They describe different vessels. In packed bed scrubber sizing, the second value is the one that governs the diameter.
Can I use an online scrubber sizing calculator instead?
A calculator is useful for a first pass and unreliable as a final answer, for one reason: the two inputs that matter most are usually defaults. The HTU value is a placeholder unless you supply one from your own system, and the pressure drop correlation is typically a dry-gas model, while wet pressure drop runs 1.3 to 1.5 times higher. Use a scrubber sizing calculator to bracket the geometry, then replace both defaults with your own data before the number reaches a quotation.
How much does a scrubber cost?
For a polypropylene counterflow packed bed in the 5,000 to 15,000 m³/h range, base ex-works equipment cost commonly falls between about $8,000 and $25,000 depending on shell diameter, packing depth, and material. Fabrication in Europe or North America pushes that upward significantly compared with Asian manufacture.
Equipment cost is the starting point. Installation, ductwork, and electrical work typically add 50% to 100% on top, and operating cost then adds continuous fan and pump electricity plus reagent consumption for reactive duty.
Get a Scrubber Sized Against Your Actual Duty
Decide which chain you are in before you choose a formula. If your stream carries droplets, size a separator. If it carries a gas-phase contaminant, size an absorber. If it carries both, run the two chains in series and size each vessel on its own method.
Then close the three loops most sizing sheets leave open: the fan total pressure budget, the water balance, and the temperature correction. Those three are what separate a scrubber sizing calculation that produces a vessel from one that produces an installation.
For the full design walkthrough, start with wet scrubber design. For the interior of a packed tower with its four interdependent calculations, see packed bed wet scrubber. For spray tower liquid loading and velocity, see spray tower scrubber. If you have a gas stream and five inputs, send them to our engineering team and we will run both chains against your actual conditions.
Note on the design figures — The velocity bands, HTU ranges, retention and clearance times, distributor pour-point density, the 1,050 kg/m³ density assumed for the 5% caustic solution, the humidity ratio behind the evaporation figure, and the seven fan-budget allowances in this article are design estimates drawn from equipment practice rather than limits published by a standards body. Where a figure traces to an official publication, that publication is linked in the text and listed under Sources below. Three of the estimates deserve a published cross-check before they reach a quotation: packed-tower pressure drop, where the U.S. EPA gives 0.5 to 1.0 in. H2O per foot of packing (about 408 to 817 Pa/m) against the 250–350 Pa/m used here for 50 mm random packing at a modest liquid load; the wet-to-dry pressure-drop ratio of 1.3 to 1.5; and the equipment cost range in the FAQ above.
Sources
- U.S. EPA, Office of Air Quality Planning and Standards – EPA Air Pollution Control Cost Manual, Section 5.2, Chapter 1: Wet Scrubbers for Acid Gas (flooding as the constraint that fixes the packed-bed cross-section, with most packed towers operating at 60 to 70 percent of the gas flooding velocity; the minimum wetting rates of 0.85 and 1.3 ft²/hr for ring packings larger than 3 in. and for everything smaller, which are the source of the 0.08–0.12 m³/(h·m) factor range used in this article; the 2 in. polypropylene Pall ring specific surface area of 31 ft²/ft³ and packing factor of 25 ft−1; the packing depth obtained from Hpack = NtuHtu, where the number of overall transfer units follows from the removal efficiency being designed for; and the 0.5 to 1.0 in. H2O per foot of packing pressure-drop band for packed towers).
- U.S. EPA, Office of Air Quality Planning and Standards – EPA Air Pollution Control Cost Manual, Section 6, Chapter 2: Wet Scrubbers for Particulate Matter (the 45 to 150 m/s gas velocity at the narrowest cross-section of a venturi throat; the 10 to 80 in. w.c. pressure loss across a venturi; and the collection-efficiency spread from greater than 99% for venturi scrubbers down to 40–60% for simple spray towers).
- U.S. Environmental Protection Agency (EPA) – Monitoring by Control Technique — Wet Scrubber for Gaseous Control (Air Emissions Monitoring Knowledge Base) (the three primary wet scrubber performance indicators — pressure differential, liquid flow rate, and scrubber liquid outlet concentration — together with the parameters named as alternatives to scrubber liquid outlet concentration: scrubber liquid pH, scrubber liquid specific gravity, and scrubber makeup/blowdown rates).
- U.S. Environmental Protection Agency, Office of Air Quality Planning and Standards – EPA Air Pollution Control Cost Manual, Section 5, Chapter 1: Wet and Dry Scrubbers for Acid Gas Control (Response to Comments) (packed bed and tray towers among the absorber types listed for hydrogen chloride service, alongside HF, HBr, F2, Cl2, and SO2; and the 95 to 99% removal efficiency that wet scrubbers typically achieve across most industrial applications).
- U.S. Occupational Safety and Health Administration (OSHA) – OSHA Technical Manual, Section III, Chapter 3: Ventilation Investigation (the fall-off of capture velocity with distance between the hood and the contaminant source — 300 fpm one duct diameter in front of a hood that carries 3,000 fpm, falling by a factor of 10 at two duct diameters — which is what makes the capture-hood allowance the most volatile line item in a fan budget).
- U.S. National Library of Medicine (NIH) – PubChem CID 14798 — Sodium Hydroxide (identity and properties of the sodium hydroxide reagent named in both worked examples).