
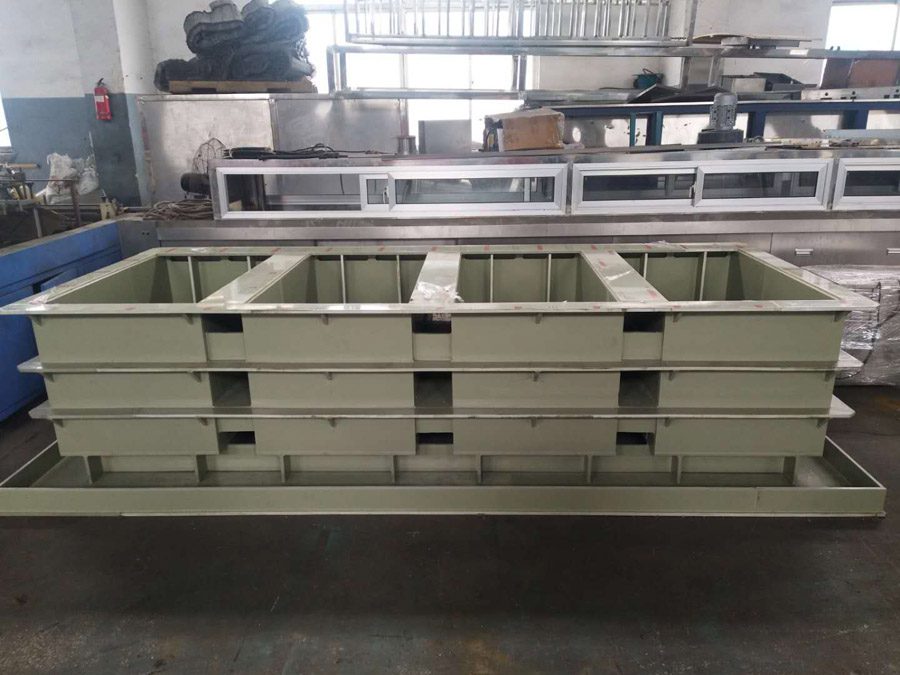
A chemical dosing tank is usually chosen by its volume, and the volume is usually the last number that should be fixed. The tank in a dosing system is not a store of water; it is the reservoir that a metering pump draws from, at a rate measured in litres per hour, to deliver an active chemical measured in grams per hour. Those two facts decide the size, the shape and the fittings, and none of them is the plant’s process flow.
This page works through the chain from dose rate to tank volume, then through the part of the design that the catalogue never shows: the tank as the suction side of a positive-displacement pump. The material comparison, the certification list and the configuration table belong to the PP dosing tank page and are not repeated here.
Key takeaways
- A dosing tank is sized from the chemical consumed per hour and the refill interval, not from the flow being treated.
- The chain is dose (mg/L) × flow (m³/h) = grams per hour, then grams per hour ÷ solution strength (g/L) = litres per hour.
- The tank is the pump’s suction vessel. A falling level changes the suction condition continuously, which is why a dosing tank is shallow and wide rather than tall and narrow.
- Usable volume is the band between the low-level lockout and the high-level alarm, not the nominal capacity.
- Dilution follows one line of arithmetic: parts of water per part of mother solution = mother strength ÷ working strength − 1.
- The vent has to pass the fill rate, because the air leaving the tank is displaced at exactly the rate the liquid enters.
- “Batch tank” returns open-top mixing vessels, and “day tank design” returns diesel fuel tanks. Neither is a chemical dosing tank.
What “Chemical Dosing Tank” Actually Covers
Three unrelated products sit behind this phrase in the search results, and a buyer who orders from the wrong one gets a vessel that cannot do the job. The engineering that follows on this page applies to the first of them.
Three products answer to the phrase
The first is the chemical feed tank: a small reservoir, typically 20 to 1,000 litres, that holds a working solution for a metering pump. It is the tank in a water treatment plant’s chlorine room, in a cooling tower’s biocide feed, in a boiler’s oxygen scavenger line. The bulk vessel that fills that small reservoir is a different design problem, because the stored solution changes while it waits: the poly bleach tank guide covers it. Its defining feature is that it is connected to a pump that draws a few litres an hour, and everything about its design follows from that connection.
The second is the septic dosing tank, which is a different product entirely. In on-site wastewater systems, “dosing” means releasing a measured volume of effluent to a drainfield on a timer, and the tank that holds it is a large buried concrete or plastic chamber sized to the household’s daily flow. Its sizing rules come from on-site wastewater codes, not from chemical feed practice.
The third is the fuel day tank: a small tank that holds a day’s diesel for a generator or a boiler, fed from a bulk tank by a transfer pump. It is a real and important product, and it is governed by flammable-liquid codes rather than by chemical compatibility. A search for “day tank design” returns almost nothing but these.
The three share a shape and a phrase and almost nothing else. The volume basis, the materials, the fittings and the regulations are different in each case.
A batch tank is a mixing vessel, not a dosing tank
The phrase “batch tank” is assigned to this unit in the keyword plan, and it belongs to a different product. A batch tank is an open-top vessel in which a batch of product is mixed, blended or reacted: food, paint, cosmetics, drilling fluid. It has an agitator, a large opening and usually a cone or dished bottom for emptying solids.
It can be used as a dosing tank, and often is, because any vessel that holds liquid can feed a pump. But it is not designed for that job, and the differences matter: an open top is a fume path, a wide flat bottom leaves a heel the pump cannot reach, and an agitator sized for mixing a viscous batch will shear a dilute chemical solution into foam.
What a dosing tank needs instead is a closed or vented lid, an outlet at the lowest point, a suction arrangement that keeps the pump flooded, and a volume small enough that the solution turns over before it ages. Those are not batch-tank features.
What this page is actually about
Material selection for dosing tanks is a real question and has its own page. The question here is upstream of it: how much solution a chemical dosing tank has to hold, where its outlet goes, and how the pump behaves as the level falls. A plant that gets those wrong will specify a perfectly good tank that doses inaccurately.
The rest of this page covers the dose-to-volume chain, the suction-side geometry, dilution and mixing, level control, venting and containment, and the six inputs a fabricator needs to quote.
The Volume Comes From the Dose, Not From the Plant’s Flow
A water storage tank is sized by the gap between supply and draw. A chemical dosing tank is sized by something else entirely: the mass of active chemical the process needs per hour, converted into the volume of solution that carries it, multiplied by the interval between refills.
From dose rate to grams per hour
The process requirement is almost always stated as a concentration: 5 mg/L of chlorine, 2 mg/L of antiscalant, 50 mg/L of coagulant. Multiply by the flow being treated and the result is a mass rate.
5 mg/L at 100 m³/h is 5 grams per cubic metre times 100 cubic metres per hour, which is 500 grams per hour. The arithmetic is worth writing out because the units hide it: milligrams per litre and grams per cubic metre are the same number, so the conversion is only a multiplication by flow.
That 500 g/h is the demand. Everything downstream — pump setting, solution strength, tank volume — exists to deliver it.
From grams to litres of solution
Metering pumps move volume, not mass. The bridge between the two is the strength of the solution in the tank, expressed as grams of active ingredient per litre.
A commercial sodium hypochlorite solution is sold with its available chlorine stated on the label, commonly in the range of 120 to 150 grams per litre. Take 140 g/L: 500 g/h divided by 140 g/L is 3.57 litres per hour. That is the pump’s duty, and it is the number the pump is selected on.
Two things follow. The first is that the tank volume and the pump duty are linked through the solution strength: dilute the solution and the pump has to move more of it, which may take the pump outside its accurate range. The second is that the label number is the input, not a constant — a different product at 120 g/L gives 4.17 L/h for the same 500 g/h, and the tank arithmetic has to be redone.
The refill interval sets the tank
With the solution flow known, the tank volume is the flow multiplied by the interval between refills. A tank refilled once a day at 3.57 L/h needs 85.7 litres, and a 100-litre tank gives about 28 hours of solution — a day plus a margin.
This is the definition behind the term “day tank”: a vessel that holds one day of consumption and is refilled from a larger bulk tank or from delivered drums. The interval is an operational decision, not a physical one. It depends on who refills the tank, how far the chemical store is, and whether the plant runs at weekends.
A weekend is the interval that catches people. A tank sized for one working day runs dry on Saturday morning unless somebody refills it or the dosing is stopped. Either the interval becomes three days, or the refill becomes a weekend task, and the specification should say which.
When the dose is not constant
Everything above assumes a fixed dose. In most plants it is not fixed: the chlorine dose follows the flow, the antiscalant follows the recovery of a membrane train, the pH correction follows an inlet measurement. The tank volume still comes from the same chain, but the flow used in it changes.
Two arrangements are common. In flow-paced dosing, the pump speed follows a flow signal, so the solution flow varies hour by hour while the solution strength stays constant. In set-point dosing, the pump speed follows a measured value such as free chlorine or pH, and the solution flow varies with the control error rather than with the flow.
Either way, the number that sizes the tank is the daily consumption, not the instantaneous rate. A plant that doses at 8.9 L/h for four hours, 1.8 L/h for four hours and nothing overnight consumes about 43 litres, not the 214 that a tank sized from the peak rate would imply.
Why a month of stock is the wrong answer
The instinct to buy a big tank and refill it rarely is understandable and usually wrong for a working solution. A dilute solution in a tank is not a stable product; it changes with time, temperature and exposure to air and light, and a tank that holds a month of it delivers a different concentration at the end of the month than at the start.
There is a second, more mundane cost: the larger the tank, the longer the pump draws from a level that is falling slowly, and the more the installation depends on the level control being right. A small tank that is refilled often is easier to keep correct than a large one that is refilled rarely.
The practical rule is to size for the refill interval the plant will actually keep, then check that the resulting tank is not so small that a single missed refill stops the process. Two days of solution in a 200-litre tank is a reasonable compromise for a plant that refills on a weekday rota.
| Flow treated | Dose | Active chemical | Solution at 140 g/L | 24 h consumption |
|---|---|---|---|---|
| 50 m³/h | 5 mg/L | 250 g/h | 1.8 L/h | 43 L |
| 100 m³/h | 5 mg/L | 500 g/h | 3.6 L/h | 86 L |
| 250 m³/h | 5 mg/L | 1,250 g/h | 8.9 L/h | 214 L |
| 500 m³/h | 5 mg/L | 2,500 g/h | 17.9 L/h | 429 L |
Note on the figures — the 140 g/L column is an example value for a commercial hypochlorite solution. Use the available-chlorine figure on your own product label; the arithmetic is a division either way.
| Tank volume | Hours of solution at 3.6 L/h | Equivalent |
|---|---|---|
| 25 L | 7.0 h | One shift |
| 50 L | 14 h | Two shifts |
| 100 L | 28 h | One day with margin |
| 200 L | 56 h | 2.3 days |
| 500 L | 140 h | 5.8 days |
| 1,000 L | 280 h | 11.7 days |
Note on the figures — hours are nominal volume divided by 3.6 L/h. Usable volume is lower than nominal once the control band is deducted, which is covered under level control below.
The Tank Is the Pump’s Suction Side
The part of a dosing tank that decides whether the system works is the part nobody photographs: the outlet, the suction line and the relationship between the liquid level and the pump inlet. A metering pump is a positive-displacement device, and its accuracy depends on the suction condition being the one it was calibrated in.
Flooded suction, and what it buys
Flooded suction means the pump inlet is below the tank’s lowest working level, so the liquid arrives at the pump under a positive static head rather than being lifted. The pump then has to do only one job — displace a fixed volume per stroke — instead of two.
The static head is simple arithmetic: height of liquid above the inlet, multiplied by the solution’s specific gravity, multiplied by 9.81. A solution at specific gravity 1.2 with 0.5 m of liquid above the inlet gives 0.5 × 1.2 × 9.81, or 5.9 kPa. That is not much, and it is enough: the pump is being fed rather than pulling.
The alternative, a pump mounted above the tank and drawing by suction lift, can work. Diaphragm and peristaltic pumps are sold with a rated suction lift, and a pump installed within that rating will prime. What changes is the margin. Every metre of lift, every metre of suction pipe and every fitting between the tank and the pump removes some of the pressure available to fill the pump chamber, and a pump that is working near its lift limit is a pump whose delivered volume per stroke is no longer the calibrated figure.
What a falling level does to a metering pump
A storage tank is drawn down over hours; a dosing tank is drawn down over the same hours but from a much smaller height. That difference matters because the suction head at the pump changes as the level falls.
In a flooded installation with 0.8 m of liquid above the inlet when full and 0.2 m at the low-level lockout, the static head at the pump falls from 9.4 kPa to 2.4 kPa over the tank’s working range. The pump still has positive head throughout, so the change is benign. In a suction-lift installation, the same 0.6 m of level change moves the pump from 0.2 m of lift to 0.8 m of lift, and the delivered volume can drift with it.
The design consequence is a shape decision: a dosing tank is usually wider and shallower than a storage tank of the same volume, so that the level change over the working band is small relative to the head at the pump. A tall narrow tank puts the pump through a larger suction swing for the same litres.
The foot valve, the strainer and the last 100 mm
Three small items sit between the tank and the pump, and each has a job that is easy to omit.
The foot valve holds the suction line full when the pump stops, so that the pump does not have to re-prime on every start. On a flooded installation it is less critical; on a suction-lift installation it is the difference between a pump that starts and a pump that does not.
The strainer keeps debris out of the pump’s valves. A diaphragm pump has small check valves, and a flake of undissolved chemical or a piece of lid gasket will hold one open, which turns a metering pump into a pass-through. The strainer has to be accessible for cleaning, which means it cannot be at the bottom of a tank that requires emptying to reach it.
The last 100 mm is the dead volume below the outlet. Whatever sits below the suction opening is a heel that the pump cannot draw, and it accumulates the densest part of the solution. A tank whose outlet is 100 mm above the floor of a 1 m² footprint loses 100 litres of capacity and keeps the worst of the liquid in it.
Where the outlet goes
A side outlet is the usual choice on a small tank because it is easy to weld, easy to reach and easy to connect. Its cost is the heel described above, and its second cost is that the outlet is at a fixed height: the pump cannot draw below it, so the low-level lockout has to be set above the outlet or the pump will run dry while the tank still looks full.
A bottom outlet, or a sump recessed below the floor, removes the heel and lets the tank empty almost completely. It costs a support frame, because the outlet needs clearance underneath, and it puts a connection where a leak is least visible.
Either arrangement works. What does not work is a side outlet with a low-level switch set below it, which is a common combination and guarantees that the pump’s last hour of operation is dry.
The suction line between the tank and the pump
The pipe between the tank and the pump is short, and it is the part of the installation most often left to whoever is connecting it. Three properties matter: length, bore and the absence of dead legs.
Length matters because every metre of suction pipe adds friction loss, and friction loss on the suction side subtracts from the pressure available to fill the pump chamber. A pump mounted one metre from the tank and a pump mounted six metres from it are not the same installation, even with the same static head.
Bore matters because a suction line that is too narrow turns the pump’s displacement into a velocity the pipe cannot supply without a pressure drop. The suction bore should be at or above the pump’s inlet connection, and it should not be reduced to suit a convenient fitting.
Dead legs matter because a length of pipe the flow does not sweep holds stagnant solution, and a stagnant leg on a hypochlorite line is where gas collects and where crystals form. The suction line should rise continuously from the tank to the pump, with no horizontal run that can trap gas and no unused branch left capped.
Mixing, Dilution and Concentration Drift
A dosing tank holds a solution, and a solution is only useful if its strength is the one the pump was set for. Three things move that strength after the tank is filled: the make-up arithmetic, the way the liquid stratifies, and evaporation.
Make-up ratios
Most dosing systems do not feed the product as delivered. They dilute it to a working strength, because the pump’s accurate range is a few litres an hour and the product is far too concentrated to meter directly.
The arithmetic is one line. To go from a mother solution of strength Cm to a working solution of strength Cw, the parts of water to add per part of mother solution is Cm / Cw − 1. A 12 % product diluted to 1 % takes 11 parts of water per part of product, and the twelve parts together are at 1 %.
The same formula in the other direction sizes a batch. A 500-litre batch at 2 % from a 12 % product takes 500 × 2 / 12, or 83.3 litres of product, and 416.7 litres of water.
Two errors are common. The first is treating percentages as additive rather than as concentrations: 1 litre of 12 % plus 11 litres of water is 12 litres at 1 %, not 12 litres at 12 %. The second is ignoring the volume of the product when filling to a mark: a tank filled to 500 litres with 83.3 litres of product already in it takes 416.7 litres of water, and adding 500 litres of water gives a weaker solution and an overflow.
| Mother solution | Working strength | Parts of water per 1 part mother |
|---|---|---|
| 12 % | 5 % | 1.4 |
| 12 % | 2 % | 5 |
| 12 % | 1 % | 11 |
| 12 % | 0.5 % | 23 |
| 10 % | 1 % | 9 |
| 5 % | 1 % | 4 |
Note on the figures — parts of water = mother strength ÷ working strength − 1. The ratios assume the two liquids mix without volume change, which is close enough for a tank fill and is not a laboratory standard.
Stratification, and where the suction should sit
A solution left still does not stay uniform. Denser liquid settles, warmer liquid rises, and a tank that was homogeneous at filling can have a weaker layer at the top and a stronger one at the bottom by the next morning.
Where the suction sits decides which layer the pump gets. A suction near the bottom draws the strongest solution; a suction near the top draws the weakest. Neither is automatically right, but the choice should be deliberate: a pump calibrated on a sample taken from the top of a stratified tank will over-dose once the tank is drawn down to the denser layer.
The practical answer is to draw from a point that represents the bulk, and to mix before sampling. Where a tank stratifies badly, the fix is usually the next section rather than a deeper suction.
Evaporation and the concentration that creeps up
An open or vented tank loses water vapour, and every litre lost leaves its dissolved chemical behind. Over a week, a tank that is refilled to the same mark with the same amount of product slowly becomes stronger, because the water that evaporated is not replaced.
The effect is largest on warm days, on tanks in sunlight, and on tanks with a large free surface. It is smallest on a closed tank with a small vent. It is never zero, which is why a dosing system benefits from a periodic check of the working strength rather than a single calibration at commissioning.
The control is not complicated: keep the lid closed, keep the tank out of direct sun, and refill by volume rather than by eye. Where the process is sensitive, make up a fresh batch on a fixed interval instead of topping up indefinitely.
What agitation a dosing tank actually needs
A dosing tank is not a reactor, and the agitation it needs is much less than a batch tank’s. Its job is to keep the solution uniform and to prevent the densest fraction from sitting on the floor, not to dissolve a solid or drive a reaction.
For most working solutions, the movement caused by filling and by the pump’s draw is enough, provided the outlet and the fill point are at opposite ends of the tank. Where a tank is large relative to its draw, or where the chemical tends to settle, a small recirculation loop — pump from the outlet, return to the top opposite corner — does the job without an agitator.
A mechanical agitator is the right answer only when a solid has to be dissolved or a suspension kept in suspension. On a dilute solution it adds a shaft seal, a motor and a foam problem in exchange for mixing that a recirculation loop would have provided.
Level Control and Dry-Run Protection
A metering pump running dry is not a harmless condition. A diaphragm pump with no liquid in the chamber has nothing to cushion the diaphragm, and a peristaltic pump with no liquid runs its tube against itself. Both fail, and both fail quietly.
The control band is the usable volume
The nominal volume of a dosing tank is a shell dimension. What the plant can use is the band between the low-level lockout and the high-level alarm, and that band is usually between 60 % and 80 % of the nominal volume.
On a 600 mm tall tank with a 400 mm control band, the usable volume is two-thirds of nominal. A tank sold as 100 litres behaves as 67 litres, which at 3.6 L/h is 18.6 hours rather than the 28 hours the nominal figure suggests. That gap is why the refill interval should be calculated on usable volume, not on the capacity printed on the tank.
The band also has a lower limit: the distance between the low-level lockout and the outlet. A lockout set at the outlet height protects the pump but leaves no margin for a slow response; a lockout set 50 mm above the outlet gives the pump a warning before the level reaches the suction.
Low-level lockout
The lockout does two things: it stops the pump, and it tells somebody. Stopping the pump protects the hardware; the alarm is what protects the process, because a dosing system that has quietly stopped is usually discovered when the treated water fails a test.
The switch itself is a float, a conductivity probe or a pressure sensor. Whatever the type, it has to be positioned where it sees the tank’s level rather than the liquid in the suction line, and it has to be reachable for cleaning. A float switch covered in crystallised chemical reads full forever.
Where the process cannot tolerate an interruption, the lockout should switch to a standby pump or a second tank rather than simply stopping. That is a control decision, but it is made at the same time as the tank specification, because it determines whether the tank needs two outlets.
Running out mid-process
The lockout stops the pump, and then the process continues without chemical. Whether that is a nuisance or a compliance event depends on the process: a cooling tower that misses an hour of biocide is a nuisance, and a potable supply that misses an hour of chlorine is not.
The answer is decided before the tank is ordered. A single tank with a single outlet gives one failure mode. Two tanks on a changeover, or a low-level signal that starts a refill before the lockout, gives the plant time. The second option is cheaper and is usually enough, provided the refill source is available when the signal arrives.
What does not work is a lockout with no alarm. The pump stops, the level sits at the lockout point, and nobody knows until a sample fails.
High-level alarm and overflow
The high-level alarm exists because the most common failure in a dosing system is a fill that does not stop. A float valve sticks open, a solenoid fails, an operator leaves a hose running. The alarm gives the plant a chance to act before the tank overflows.
The overflow is the second line. It must be sized for the maximum fill rate, not the average, and it must discharge to a safe place — a bund, a drain, or a container — rather than onto the floor. On a chemical tank the overflow is also a fume path, which is why it should not discharge into an enclosed space.
An overflow and a vent are not the same opening. A vent equalises pressure as the level changes; an overflow carries liquid. Combining them means that a normal fill pushes chemical vapour out through the vent at the fill rate, and an overfill sends liquid out of an opening that was sized for air.
Level measurement in a small tank
A small tank is harder to measure than a large one, because the same absolute error is a larger fraction of the range. A 10 mm error on a 2 m storage tank is half a percent; on a 600 mm dosing tank it is 1.7 %.
Sight glasses and float gauges are the simplest options and are adequate where the level only has to be seen. Ultrasonic and pressure transmitters give a continuous signal that can drive alarms and a refill interlock, at the cost of a device that has to be configured and maintained.
The choice should follow what the plant does with the reading. If the level is only checked by an operator on rounds, a sight glass is enough. If the level drives a lockout, an alarm and a refill request, the reading has to be continuous and it has to fail safe — a transmitter that fails high leaves the pump running, which is the wrong direction.
Venting, Fumes and Containment
Three physical requirements sit around the tank rather than inside it, and all three are decided at the specification stage because none of them can be added cheaply afterwards.
The vent passes the fill rate
A tank is a fixed volume, so every litre of liquid that enters displaces a litre of air. A tank filled at 500 litres an hour displaces 500 litres of air an hour, which is 0.5 m³/h or about 8.3 litres a minute.
That figure sets the vent. A vent sized for breathing — the slow movement caused by temperature change — will not pass a fill, and the tank will pressurise until the lid gasket leaks or the fill stops. The vent has to be sized for the maximum fill rate, including the case where a hose is used to fill faster than the normal supply.
The same arithmetic runs in reverse when the tank is emptied: the vent has to admit air at the pump’s draw rate, or the tank goes under vacuum. On a small tank the draw is small, but a tank emptied by a transfer pump rather than a metering pump can need a vent as large as its fill line.
Off-gassing chemicals
Some chemicals release gas while they sit. Sodium hypochlorite solutions release oxygen slowly, and the gas collects in the suction line and in the pump head. A diaphragm pump with gas in its chamber loses prime; a peristaltic pump pushes the gas through and keeps dosing.
The tank-side answer is to keep the vent open and to arrange the suction so that gas can escape upward rather than being trapped in a pocket. A suction line that rises and falls, or a foot valve that traps a bubble, gives the gas somewhere to sit.
Where the gas is hazardous rather than merely inconvenient, the vent has to discharge to a safe location, and the tank has to be in a space with adequate ventilation. That is a room-design question, not a tank question, but the tank’s vent is the point where the two meet.
Temperature belongs in the same discussion. A tank in direct sun heats its contents, and a warm solution releases gas more readily than a cool one. Shade, a light-coloured shell or a ventilated enclosure all reduce the rate. The same measures reduce evaporation, so they pay twice.
Bunds and double walls
Secondary containment for a chemical tank is usually one of two arrangements: a bund — a liquid-tight floor and wall around the tank — or a double-wall tank, in which the outer shell holds the contents of a failed inner shell. The annulus design is covered in the double wall tank article; the choice between the two is a site question.
A bund is easier to inspect and to clean, and it can be built around several tanks. A double-wall tank takes no extra floor space, which matters where the tank sits inside a plant room. Both have to be sized for the credible release, which is the tank’s contents plus whatever arrives before the fill stops.
Where the stored chemical is a hazardous waste, the containment requirement is a regulation rather than a preference. The RCRA container standard requires a containment system able to hold 10 % of the volume of the containers or the volume of the largest container, whichever is greater, and it excludes containers that hold no free liquids from that calculation. The rule governs hazardous waste container storage areas, not every dosing tank, but the principle — contain the largest credible release — is a sound one anywhere.
Labels and the stationary process container
A dosing tank holds a hazardous chemical, and the workplace hazard communication rule requires containers of hazardous chemicals to be labelled, tagged or marked. That sounds like a sticky label on every tank, and for a portable container it is.
For a fixed process vessel the rule provides a different route. The employer may use signs, placards, process sheets, batch tickets or operating procedures in place of affixing a label to an individual stationary process container, provided the alternative identifies the containers it applies to, conveys the same hazard information, and is readily accessible to employees in the work area throughout each shift.
A dosing tank in a plant room is exactly that case. A sign on the wall naming the chemical, its hazard and the pump it feeds satisfies the requirement without a label that will be covered in chemical within a month. The condition is that the sign is kept current and accessible, which is an operational task rather than a fabrication one.
What the rule does not allow is an unmarked tank with no alternative. A tank whose only identification is the colour of its lid is a tank that will eventually be filled with the wrong chemical.
Specifying a Chemical Dosing Tank
The specification reduces to six inputs, and the first two decide the volume. Everything after them constrains the shape and the fittings rather than the size.
The six inputs
The first is the dose: the concentration required, in mg/L or ppm, and whether it is constant or varies with the process. The second is the flow being treated, because dose multiplied by flow gives the mass rate.
The third is the solution strength in the tank: the product as delivered, or the working dilution, expressed in grams of active ingredient per litre. The fourth is the refill interval, in hours or days, and who does the refilling.
The fifth is the pump: its type, its flow range and whether it will be mounted above or below the tank. The sixth is the site and the chemical: the footprint, the headroom, the bund, and the material the chemical requires.
The two that are usually left blank are the solution strength and the pump position, and they are the two that change the tank. A tank quoted without a strength cannot be checked against the pump’s range, and a tank quoted without a pump position cannot have its outlet height set. Both are one line on the enquiry, and both avoid a revision.
The material question
Once the volume and the fittings are fixed, the material is usually straightforward. For a dilute chemical solution at ambient temperature, a fabricated polypropylene tank covers the widest range, and the wall is the corrosion barrier at full thickness. Moulded polyethylene is cheaper in the sizes it covers, but the standard for polyethylene upright storage tanks starts at 1,900 litres, so a small dosing tank sits below that floor and is specified some other way. Welded thermoplastic tanks have their own design standard family, which separates vertical cylindrical from rectangular construction.
For potable water duties, the shell and every wetted component have to be certified for health effects, and that certification does not cover microbial growth. The temperature limits, the potable certification and the freezing behaviour are set out in the polypropylene water tank article, and the general material comparison is in the polypropylene tank guide.
Two constraints are worth repeating. A tank feeding a potable process needs NSF/ANSI 61 certification on the shell and on every wetted part, including the fittings. And where the chemical is an acid, the concentration band decides the material before the volume does, which is the subject of the acid storage tank article.
What we build
We fabricate PP-H dosing tanks from 5 mm to 30 mm sheet, from 50 litres to more than 100,000 litres, in cylindrical, rectangular and skid-mounted forms, with the outlet, suction arrangement, level connections and vent welded in during fabrication rather than added afterwards. Where the chemical needs a second wall, the annulus is a separate design and is covered in the double wall tank article. Where the connections have to be specified, the poly tank fittings page covers the three routes through a wall.
For a quotation we need the six inputs above, plus the delivery location. Send them and the reply is a dimensioned drawing and a price. The full range and the configuration parameters are on the PP dosing tank page, and where the dosing tank sits inside a larger storage arrangement, the industrial water storage tank guide covers how the bulk volume and the day volume are sized together.
Frequently Asked Questions
How do I size a chemical dosing tank?
Multiply the dose in mg/L by the flow in m³/h to get grams per hour. Divide by the solution strength in grams per litre to get litres per hour. Multiply by the refill interval in hours to get the nominal volume, then add the control band and freeboard.
How big should a day tank be?
One day of solution at the pump’s duty, plus a margin for the control band. At 3.6 L/h a 100-litre tank holds about 28 hours of nominal volume, or about 19 hours of usable volume once the band is deducted.
Can I use a batch tank as a dosing tank?
It can hold the liquid, but it is not designed for the job. An open top is a fume path, a flat wide bottom leaves a heel, and an agitator sized for mixing will foam a dilute solution. A dosing tank needs a vented lid, a low outlet and a suction that keeps the pump flooded.
Why does my dosing pump lose prime?
The usual causes are air in the suction line, a suction lift that exceeds the pump’s rating, a foot valve that is not holding, or gas released by the chemical. Check the suction joints first, then the liquid level relative to the pump inlet.
Should the pump be above or below the tank?
Below, wherever the layout allows. Flooded suction removes suction lift from the variables the pump has to cope with, and it keeps the delivered volume per stroke close to the value the pump was calibrated at.
How often should the tank be refilled?
As often as the plant will actually keep up with. A daily refill is common; a two-day interval with a 200-litre tank suits a weekday rota. Sizing for a month is usually a mistake, because a dilute working solution changes strength while it sits.
Sources
- ASTM International. ASTM D1998-21: Standard Specification for Polyethylene Upright Storage Tanks. Scope clauses 1.1–1.3. store.astm.org/d1998-21.html
- British Standards Institution. BS EN 12573-1:2000, Welded static non-pressurized thermoplastic tanks — General principles, and the related parts −2 (vertical cylindrical tanks), −3 (single skin rectangular tanks) and −4 (flanged joints). knowledge.bsigroup.com
- NSF International. NSF/ANSI 61: Drinking Water System Components – Health Effects, scope statement. nsf.org
- U.S. Code of Federal Regulations. 21 CFR 177.1520, Olefin polymers, table item 1.1a (polypropylene). ecfr.gov
- U.S. Code of Federal Regulations. 40 CFR 264.175, Containment, paragraph (b)(3). ecfr.gov
- U.S. Code of Federal Regulations. 29 CFR 1910.1200, Hazard Communication, paragraphs (f)(1), (f)(6), (f)(7) and (f)(9). ecfr.gov
- INEOS Olefins & Polymers. Typical Engineering Properties of Polypropylene. Density, DSC melting point and Vicat softening temperature. ineos.com
