
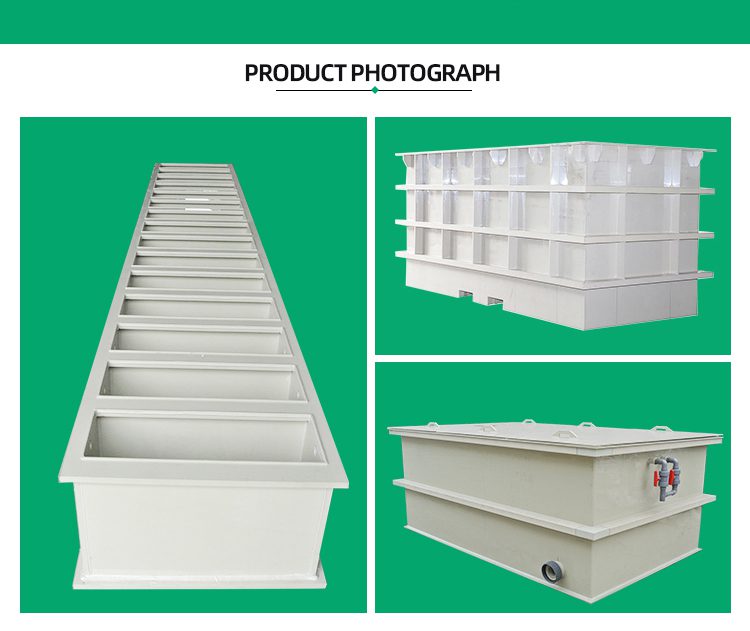
Most acid storage tank enquiries arrive backwards. The tank is already chosen — a size, a shape, a budget figure — and the acid is added afterwards as a detail to be confirmed. That order is why the same vessel gets quoted for 10% sulfuric acid and for 98%, and why one of those two vessels fails. The acid is not a detail. It is the design input, and it arrives with three numbers attached: which acid, at what concentration, and at what temperature the tank will actually run.
This page works those three numbers through the acids that get stored in bulk — sulfuric, hydrochloric, nitric, phosphoric, and hydrofluoric at the edge where a published chart is no longer enough. It treats the tank as the output of that reading. It also says plainly where the published data stops, because a compatibility table has two columns and an industrial acid duty rarely has two temperatures.
Several things here come from one document more than any other: TAPPI TIP 0606-26, the pulp and paper industry’s technical information paper on bulk concentrated sulfuric acid storage and handling, revised in 2012. It is unusually specific for an industry TIP — freezing points by concentration, materials of construction by component, inspection intervals, vent behaviour in humid climates — and it is written for the operator rather than the purchaser, which is why it answers questions that supplier catalogues avoid. Where it is silent, the ILO/WHO International Chemical Safety Cards, NOAA’s CAMEO database and the U.S. eCFR supply the rest.
Key Takeaways
- Concentration, not the word “acid”, decides the tank. On the standard five-point rating scale for polypropylene, sulfuric acid at 10% is 1/1 (20 °C / 60 °C), at 78% it is 2/4, at 93% it is 3/4. The same polymer, the same acid, three different verdicts.
- 98%, the other standard bulk strength, has no row at all in that same table. Absence of a rating is not a rating of “excellent”. It means the duty needs a written statement from the material supplier.
- Freezing, not corrosion, is what catches operators in winter. 93% sulfuric acid freezes at −35 °C (−31 °F); 98% freezes at −2 °C (28.4 °F). An uninsulated 98% tank in a cold climate is a solid block a few degrees below freezing.
- Carbon steel is the normal answer for concentrated sulfuric acid only under two conditions that quote requests rarely state: ambient temperature, and no need for periodic internal inspection. Needing to enter the tank is what turns a bare steel tank into a lined one.
- Containment for a concentrated sulfuric acid tank is 110% of tank capacity with an acid-resistant coating, because acid and sulfate salts destroy most concrete. The 10% figure that gets quoted at buyers belongs to a different rule and a different scope.
- Dilution never happens in the storage tank. Sulfuric acid added to water is violent exothermically; water added to acid boils immediately on contact.
- We warrant the tank body and welds for 12 months. Service life depends on the duty, we do not rent tanks, and we do not build transport containers.
What an Acid Storage Tank Has to Hold: Four Acids in One Vessel
“Acid” on a purchase order covers at least four substances that share a pH and very little else. They differ in how they attack metal, how they attack polymers, what their vapour does in a headspace, and whether the vapour is even the controlling hazard. Getting to a material means separating them first.
The Four Acids That Actually Drive Tank Design
Sulfuric acid dominates by volume and by difficulty. It is delivered in bulk at 93% and 98%, carried in carbon steel rail cars lined with a baked phenolic coating and in tank trucks that are, in TAPPI’s description, “predominantly 316 L stainless steel, or in some instances, carbon steel with a baked phenolic lining”. A 100-ton rail car of 93% is not insulated; a car of 98% may or may not be, and may or may not carry heating coils depending on local climate. Those two facts — the strength and the climate — already tell you what kind of storage the site needs.
Hydrochloric acid is stored as a solution, and its hazard is distributed between the liquid and the gas above it. Nitric acid is an oxidiser before it is an acid, which changes both the material question and the question of what may be stored next to it. Phosphoric acid is the mildest of the four and the most often under-specified, because its reputation for being gentle is read as permission to skip the temperature question. Hydrofluoric acid is the fifth, and the one where no chart is sufficient: it attacks glass and some plastics, and it boils at 20 °C.
Why “Acid Resistant” on a Catalogue Page Means Nothing
The ILO/WHO safety card for sulfuric acid contains a four-word line that undermines most marketing: it “attacks many plastics”. The same substance, described in a catalogue, is routinely offered in a vessel described as acid resistant. Both statements are true, and the second is useless, because resistance is never a property of a polymer alone. It is a property of a polymer against a specific chemical at a specific concentration and a specific temperature — which is why the published charts are laid out as tables and not as lists.
What the label usually hides is the temperature at which the claim was made. A rating chart with a 20 °C column answers a question that a plant rarely asks; plant services run hot, and the same chemical that scores 2 at 20 °C scores 4 at 60 °C more often than buyers expect.
Where a Storage Tank Ends and a Transport Container Begins
An acid storage tank here means a fixed, atmospheric vessel on a foundation, designed for pressures around atmospheric. A transport container is a different object with a different code basis, different loading cases, and a different regulatory regime. The dividing line is visible in the transport rules: the UN 1830 placard applies to sulfuric acid above 51% concentration, and TAPPI notes that bottom unloading of concentrated sulfuric acid rail cars is not permitted in the U.S. or Canada unless a specific exemption has been obtained, granted only for unit trains.
The design codes differ accordingly. TAPPI points vertical bulk storage at API Standard 650 (welded steel tanks for oil storage) and horizontal vessels at ASME Code Section VIII, Division 1, and then recommends that any new sulfuric acid tank design follow NACE RP0294-94 instead, because that standard addresses the corrosion behaviour of this acid specifically. We build the fixed vessels and not the transport containers, and the rest of this page stays on that side of the line.
What This Page Leaves to Our Other Guides
Three subjects belong elsewhere and are not repeated here. The polymer science of polypropylene — crystallinity, homopolymer against copolymer, why it softens over a range — is set out in our polypropylene tank guide. Venting routes and secondary-containment mechanisms, including the full argument about which rule set applies to which vessel, are treated in plastic chemical storage tanks. The use of acid in a process bath rather than in storage belongs to the pickling and plating pages.
What remains is the acid-specific part: which concentration bands exist, what each one does to each material family, and which of the operating traps actually destroys tanks.
Sulfuric Acid: Concentration Decides the Tank, Not the Tank the Acid
For an acid storage tank, sulfuric acid is the acid for which a single material recommendation is most misleading. Five different concentrations reach a plant gate, and they behave like five different chemicals in a tank.
The spelling is worth settling before the numbers, because three vocabularies arrive for the same vessel. British usage, and most of the UK and Indian literature, write sulphuric acid, and a sulphuric acid tank is the same vessel as a sulfuric acid tank. A shorter notation turns up as well: a datasheet or a request that works from the formula will list an H2SO4 tank and mean exactly the same duty. The chemistry does not change with the spelling, and neither should the tank.
Five Concentrations, Five Different Storage Problems
Dilute, around 10%. Mild in material terms and demanding in nothing much: on the polypropylene rating scale it is 1 at 20 °C and 1 at 60 °C. Dilute acid is usually a site-made or by-product stream, and the storage problem is not corrosion but what happens if the stream concentrates or if someone tops the tank up from a concentrated delivery.
Around 78%. Still pumpable, still liquid at any climate a plant operates in, and already a different answer: 2 at 20 °C, 4 at 60 °C on the same scale. A 78% duty that is genuinely at ambient is a plastic tank duty. The same duty at 60 °C is not, and the difference between those two services is a temperature reading that most enquiries do not contain.
93%. The standard strength for bulk delivery, uninsulated, at 1.8279 g/ml. On the same scale, 3 at 20 °C and 4 at 60 °C — and rating 3 is defined as “acceptable”, glossed in the source as light attack and limited use. That is a conditional pass, not a recommendation.
98%. The other standard bulk strength, at 1.8361 g/ml, and the one with no entry at all in the polypropylene table. There is no published rating to quote, at either temperature, and that absence is the single most important fact on this page for anyone specifying a plastic vessel.
Oleum, or fuming sulfuric acid. Not a concentration of sulfuric acid but a solution of sulfur trioxide in it, sold at figures such as 103% with 13% free SO3. The safety card for oleum records relative density 1.9 — it is the densest thing on this list — and states that it attacks some plastics.
Density 1.84 g/ml: What an Acid Load Does to the Shell
Water is the mental default at a specific gravity of 1.0, and every hydrostatic load in a tank scales with the density of what is actually inside it. At 1.8361 g/ml, a full shell carries about 84% more load than the same shell full of water: the same hoop stress at the base, the same bearing pressure on the base plate, the same load through the support ring, all multiplied by 1.84.
That is a structural input before it is a chemical one, and it is a figure the acid supplier will state on the specification sheet. TAPPI makes the same point about flexible hoses on the unloading side: all flexible unloading lines should be fully supported, specifically to prevent stress on the hose caused by the high density of sulfuric acid. If a hose needs support for this reason, a tank needs a structural check for it.
The 93% Line: Why the Same Acid Flips Its Verdict Here
Two things change at the 93% mark, and they change in opposite directions. Thermoplastics lose their margin: polypropylene goes from 2 to 3 at 20 °C between 78% and 93%, and the 60 °C column is 4 in both cases. Metals gain theirs: TAPPI’s materials table opens with the flat statement that mild steel is suitable for all tanks, scoped in the text to acid at normal ambient temperatures and commercial strengths.
The same document then qualifies the metal answer for piping and nozzles in a way that is worth reading closely. Where flow at an inlet or outlet will exceed 3 ft/s (0.9 m/s), carbon steel is not recommended; the recommendation becomes 316 or Alloy 20 for concentrations greater than 93%, and Alloy 20 for concentrations below it. In piping generally, Alloy 20 is specified above 6 ft/s (1.8 m/s), with 316L stainless or Kynar-lined pipe otherwise. Carbon steel pipe is acceptable only below 3 ft/s, and even then may develop pinhole leaks at localized defects in the steel. The strength of the acid does not make carbon steel better behaved in a nozzle; it makes the flow regime the deciding variable.
Concentration Band Table: Material, Temperature, Verdict
| Concentration | Density at 20 °C | PP rating 20 °C / 60 °C | Material that normally wins | What actually limits it |
|---|---|---|---|---|
| 10% | — | 1 / 1 | PP or HDPE | Nothing in the chemistry at this strength; the limit is service temperature and the fittings |
| 78% | — | 2 / 4 | PP at ambient temperature only | The second column: unacceptable at 60 °C |
| 93% | 1.8279 g/ml | 3 / 4 | Carbon steel; baked phenolic lining if entry is needed | Marginal for PP at ambient; out of the question at 60 °C |
| 98% | 1.8361 g/ml | no entry | Carbon steel | No published PP rating; freezes at −2 °C (28.4 °F) |
| Oleum (103%, 13% free SO3) | 1.9 (oleum) | no entry | Steel to NACE RP0294-94 | Attacks some plastics; melting point 2 to 21 °C depending on free SO3 |
Reading a Supplier’s Compatibility Chart the Way It Was Written
Three rules make a published chart usable rather than decorative. First, read the column headings before the rows: the standard table is two temperatures, 20 °C and 60 °C, with nothing in between, and interpolating a rating at 40 °C produces a number no source supports. Second, read the scale definitions, not the numbers: rating 3 is “acceptable” with light attack and limited use, which is a sentence about a maintenance regime rather than a green light. Third, treat a missing row as missing evidence. If a concentration is not in the table, the table has not cleared it — and for 98% sulfuric acid, one of the two standard bulk strengths, that is exactly the situation.
What fills that gap is not a better chart but a written statement. Ask the material supplier, in writing, for the service range at your concentration and your temperature, and keep it with the tank file. On our side, PP chemical storage tanks are quoted against a stated duty rather than a chemical name, precisely because this gap exists.
Carbon Steel and Thermoplastics in Sulfuric Acid: Where Each One Breaks
The short version of the material question for sulfuric acid is that metals and thermoplastics fail for opposite reasons, and the crossover sits around the commercial concentrations rather than at some natural boundary. Understanding why makes the choice auditable instead of a preference.
Carbon Steel, and the Conditions Attached to It
TAPPI’s statement is conditional, and the conditions matter more than the conclusion. Sulfuric acid attacks most common metals, but for acid at normal ambient temperatures and commercial strengths, carbon steel or certain stainless steels are generally satisfactory — if there is no need to enter the tank for inspection on a periodic basis. Read the second clause twice. The recommendation is not “carbon steel resists sulfuric acid”; it is “carbon steel is acceptable where nothing forces you to open it up”.
The moment periodic entry is expected, the same document changes its advice: consider lining a carbon steel tank with a baked phenolic acid-resistant lining. Entry and inspection are not neutral acts in a steel acid tank. Washing the iron sulfate paste from the tank to facilitate entry and inspection can cause significant corrosion, and exposure of a baked phenolic lining to both sulfuric acid and wet air or water can cause severe damage to the lining itself. The inspection regime and the lining that permits it start to consume each other.
Two consequences follow for anyone comparing a steel tank with a thermoplastic one. A steel tank in this service is really a lining system whose steel is a structural backing, and the lining is the part that fails. An unlined thermoplastic shell has no lining to inspect, no holiday to test and no paste to wash off — which is a genuine operational advantage, and also the reason a plastic tank is a poor choice for a large-volume ambient duty where steel is simply cheaper.
The Two By-Products That Come With a Steel Tank
Hydrogen. Sulfuric acid will react slowly with steel to produce hydrogen gas, which can form an explosive mixture with air. The rate is slow, which is why nothing happens for years; the accumulation is what matters, and the headspace is where it collects. TAPPI’s hot-work rule for the area around a tank containing product is not a formality: vent the tank at the top with a large volume of air, run an atmospheric explosives test to confirm no hydrogen is present, and keep the air blowing while the work continues.
Iron sulfate. The reaction leaves a sulfate paste, and the acid itself becomes discoloured — TAPPI notes that it is colourless but impurities may give it a yellow to brown colour, and that very small quantities of organic material will blacken the acid through suspended carbon. For a process that cares about acid quality rather than only about containment, both the paste and the discolouration are specification issues, not cosmetic ones.
FRP and Vinyl Ester: a Resin Question, Not a Chart Question
Fibre-reinforced plastic tanks appear in every sulfuric acid discussion and are usually defended with a single concentration number. We do not print one. The service envelope of an FRP vessel is set by the resin system, the cure, the liner and the laminate schedule, and those vary between fabricators in ways that a single figure cannot represent. The useful question is not “what is the FRP limit” but “what range will the fabricator put in writing for this resin, at this temperature, in this laminate” — and then whether the answer covers the duty.
What is worth saying is that FRP and thermoplastics fail differently. A thermoplastic shell shows mechanical damage and weld defects; an FRP shell depends on a resin-rich inner layer for its chemical resistance, and that layer is the thing to inspect. If a quotation for an FRP acid tank does not name the resin system and the liner, it has not answered the question.
Stainless: 316L, Alloy 20, and Where Each Appears
The stainless grades in this service are not chosen for general corrosion resistance but for specific components and velocities. TAPPI’s materials table names 316L for pipe, with Alloy 20 substituted above 6 ft/s, and specifies 316 or Alloy 20 around nozzles where inlet or outlet velocity exceeds 3 ft/s. Tank trucks for all grades of sulfuric acid are predominantly 316 L stainless. Alongside those it lists two things a buyer rarely asks about: Teflon-lined hoses with an abrasion-resistant outer covering, and Viton B gaskets.
The gasket specification deserves a sentence of its own. Sulfuric acid chars most organic substances on contact, which is a poor match for generic rubber, and a gasket is the smallest and most frequently replaced wetted part on the tank. Viton B is named because it survives the duty; substituting a cheaper elastomer saves a trivial amount and moves the first failure to a flange.
Where Each Material’s Failure Shows Up First
Carbon steel fails at a defect. TAPPI’s warning is specific: seamless schedule 80 carbon steel pipe may develop pinhole leaks at localized defects in the steel, and an inlet positioned too close to the shell can cause serious corrosion of the shell — which is why inlets belong near the centre of the top and should protrude about 1 inch (2.54 cm) beyond the shell. Failures are localized, and the geometry of the nozzle is part of the cause.
Thermoplastics fail at joints and at deflection. Our own inspection effort goes into the welds: thick-section welds are checked ultrasonically, and hydrostatic testing runs at 1.5 times design head. Where acid is handled in a process vessel rather than stored — pickling lines, plating baths — that is a different design problem, covered on our tanks we build for pickling lines page. Storage and use have different duty cycles and different failure modes, and the material argument does not transfer between them unchanged.
PP, HDPE and XLPE in Acid Service: Three Thermoplastic Answers
Once the decision is a thermoplastic, the acid duty narrows the field quickly. Poly tanks for sulfuric acid are sold in all three of the polymers below, they are not interchangeable, and the published data covers them unevenly. The useful question is not which one is cheapest but which one survives the concentration and the temperature on the duty sheet.
PP — the Widest Acid Coverage of the Three, and Its Two Limits
Polypropylene has the broadest acid coverage in the standard table, and the pattern is worth reading rather than skimming. Sulfuric acid: 1/1 at 10%, 2/4 at 78%, 3/4 at 93%. Hydrochloric acid: 1/1 at 10%, 2/3 at 37%. Phosphoric acid: 1/1 at both 25% and 85%. Hydrofluoric acid: 2/2. Nitric acid: 2/3 at 5%, and 4/4 at 65% — the one outright refusal in the acid list.
Two limits sit on top of those numbers. The first is the second column. Our fabricated tanks are rated for service from −10 °C to 95 °C, a range set by stiffness rather than by melting, but the resistance chart stops at 60 °C. Between 60 °C and 95 °C a plant is operating inside our structural rating and outside the published chemical data — a legitimate place to be, but only with a written material statement and not by inference.
The second limit is the acid family that oxidises. Nitric acid at 65% is rated 4 at both temperatures, defined as unacceptable, significant attack. No amount of wall thickness changes a rating of 4.
HDPE — Where It Genuinely Works, and the Temperature Question
High-density polyethylene’s place in sulfuric acid service is narrower and more specific than its general reputation suggests. TAPPI names it in one context only: small tanks, under 10,000 gallons, are sometimes made from stainless steel or a special HDPE made especially for sulfuric acid service, and these materials reduce or eliminate formation of hydrogen gas and iron sulfate. The operative words are “special” and “made especially”. A commodity HDPE tank and a sulfuric-acid-grade HDPE tank are not the same material choice, and the phrase in a quotation that matters is the one that names the grade.
The temperature question needs care. Resin data sheets give HDPE a density of 0.930–0.965 g/cm³ and a Vicat softening temperature of 132 °C for the homopolymer, but a softening point is a laboratory landmark, not a service ceiling. A tank that is still dimensionally intact at a temperature can be deflecting under load well before then, and chemical attack rates change with temperature independently of stiffness. The service limit for a specific acid has to come from the material supplier as a statement about that duty.
XLPE — What Crosslinking Buys, and Why Suppliers Disagree at 98%
Crosslinked polyethylene is the same polyethylene with its chains chemically joined after forming. That changes mechanical behaviour — the polymer is more resistant to stress cracking and holds its properties to higher temperatures than the linear material — and it does not change the chemistry of the polymer’s surface, because the repeat unit is the same. Resistance to a given acid is therefore not transformed by crosslinking, only the tank’s structural behaviour under load is.
Which is why the 98% sulfuric acid question produces contradictory answers from suppliers. The published acid tables, such as the polypropylene chart used above, do not carry an XLPE column at all, so the claim cannot be checked against a table. We do not fabricate XLPE acid tanks, and we will not quote one against a rating we cannot verify. Where a crosslinked vessel is proposed for 98% service, ask for the service range in writing, at that concentration, at that temperature, and read the warranty wording against it — a warranty that excludes the duty is an answer in itself.
Fittings, Gaskets and Bolts: the Parts That Fail Before the Shell
An acid tank is a shell plus a set of smaller decisions, and the smaller decisions cause the incidents. TAPPI’s component list is worth adopting wholesale: Viton B gaskets, Teflon-lined flexible hoses with an abrasion-resistant cover, and — against the usual instinct to avoid flanged joints — flange tank connections, because leaks at such connections can sometimes be stopped by tightening the flange bolts. A welded joint cannot be tightened.
Piping is where the two rules collide. PVC and CPVC are corrosion resistant and are still not recommended, on the grounds of risk of mechanical failure. A material can pass the chemistry and fail the mechanical duty, and acid service is full of that pattern: the fitting is rated for the medium and not for the load, the velocity or the temperature cycle.
Access is a specification item too. In TAPPI’s design recommendations, entrance manholes at the top should be a minimum of 24 inches in diameter — a figure that belongs in the drawing, not in a later conversation with a contractor. Level indication should exist as a separate, independent high-level alarm to prevent overfilling. On a tank that cannot be visually checked easily, the instrument is the only defence.
Thermoplastic Selection Table by Acid Family
| Acid and concentration | PP at 20 °C | PP at 60 °C | Position for a thermoplastic tank |
|---|---|---|---|
| Sulfuric 10% | 1 | 1 | Straightforward; confirm the temperature and the fittings |
| Sulfuric 78% | 2 | 4 | Ambient service only; a 60 °C duty is out |
| Sulfuric 93% | 3 | 4 | Conditional at ambient (light attack, limited use); not at 60 °C |
| Sulfuric 98% | no entry | no entry | No published rating; written material statement required |
| Hydrochloric 10% | 1 | 1 | Straightforward |
| Hydrochloric 37% | 2 | 3 | Good at ambient, limited use at 60 °C; watch the vapour space |
| Nitric 5% | 2 | 3 | Good at ambient, limited use at 60 °C |
| Nitric 65% | 4 | 4 | Unacceptable; no thermoplastic answer |
| Phosphoric 25% and 85% | 1 | 1 | Excellent at both temperatures; the constraint moves to structure |
| Hydrofluoric, any strength | 2 | 2 | Chart says good; the headspace is the hazard — written answer first |
Dilution, Freezing and Heat: Three Operating Traps of Acid Storage
Most acid storage failures that reach us as enquiries are not material-selection errors. They are operating events: something was diluted, something froze, or something that should have stayed dry got wet. All three are predictable, and all three are cheap to prevent at the specification stage.
Trap 1 — Dilution Heat, and Why It Must Not Happen in the Tank
The rule is older than the industry and is still broken monthly: always add acid to water, never add water to the acid. Sulfuric acid mixed with water is extremely exothermic, and TAPPI describes the consequence precisely — the water will boil immediately on contact with the acid, resulting in a violent reaction. The ILO/WHO card states the same rule in the imperative: never pour water into this substance; when dissolving or diluting, always add it slowly to the water.
The concentration dependence is what makes the trap specific to storage. CAMEO records that reaction with water is negligible unless acid strength is above 80–90%, at which point the heat from hydrolysis is extreme. A tank holding dilute acid is not a tank that is dangerous to dilute. A tank holding 93% or 98% acid is, and the danger is not only thermal: TAPPI warns that adding a small amount of water to sulfuric acid causes a violent heat-generating reaction, and separately that exposing a baked phenolic lining to both acid and wet air or water can cause severe damage to the lining.
The engineering consequence is a boundary, not a procedure. Dilution belongs in a dedicated vessel designed for it — agitated, cooled, vented, with the acid metered into the water, which is the duty our dosing tanks built in PP are sized against. If a site needs dilute acid in bulk, it should buy dilute acid or dilute downstream of storage. A storage tank that receives both concentrated deliveries and water is two incompatible duties in one shell.
Trap 2 — the Freezing Point Nobody Checks in Winter
Freezing is the trap that surprises acid storage tank operators because it runs against intuition: the more concentrated the acid, the higher the freezing point, up to a point. TAPPI gives both commercial strengths explicitly. 93% sulfuric acid freezes at −35 °C (−31 °F). 98% sulfuric acid freezes at −2 °C (28.4 °F). The stronger acid solidifies within a couple of degrees of ordinary winter weather.
The transport rules already reflect this. TAPPI notes that rail cars carrying 93% sulfuric acid are not insulated, while cars shipping 98% acid may or may not be insulated and are equipped with or without heating coils, depending on local climate conditions. If the supplier is insulating and heating a car for the delivery journey, a site that receives 98% and stores it uninsulated outdoors has removed the protection at the one point where the product sits still for weeks.
Oleum is worse in the same direction. The safety card records melting points that vary with free SO3 content: about 2 °C at 20%, 21 °C at 30%, and about 5 °C at 65%. Some oleum grades are solid at ordinary storage temperatures.
Freezing also damages in ways that thawing does not undo. A solid mass inside a shell loads fittings, nozzles and the base differently from a liquid, and expansion against a closed nozzle or a full line has nowhere to go. The specification answer is climate-specific: insulation, trace heating, or a decision to store 93% rather than 98% where the winter range demands it.
Trap 3 — the Headspace: Moisture, Padding Air, and a Vent That Must Never Block
The third trap is invisible from outside the tank. In humid environments, TAPPI warns, ingress of atmospheric moisture could cause excessive corrosion to the inside of a sulfuric acid storage tank — the headspace is where the acid meets air, and it is the surface that does not get inspected. Two remedies are named: flushing the headspace with a slight flow of a dry inert gas such as nitrogen to displace moist air, or fitting desiccant pots to the vent.
TAPPI recommends the first and warns against the second, for a reason worth recording: desiccant systems must be scrupulously maintained and isolated from rainfall, and wet desiccants could cause blockage of the tank vent, which could cause the tank to rupture or implode when acid is being pumped into or out of the tank. A device installed to protect the shell can become the thing that destroys it. Every bulk storage tank is atmospheric and depends on a goose-neck vent to survive being filled or emptied; a vent is a safety device, not an accessory.
The same moisture logic governs unloading. TAPPI requires plant air used for off-loading sulfuric acid to be very dry, below −40 °C (−40 °F) dew point, and free from entrained moisture, oil and particulate matter — and notes that many chemical suppliers now recommend mechanical pumps instead of compressed-gas padding, because stored energy in the padding gas becomes spray and leakage when a hose fails. If a site unloads with plant air, the air quality is part of the tank specification.
Operating Limits Table: What to Control, and to What Value
| Control point | Value or rule | Why |
|---|---|---|
| Dilution | Never in the storage tank; acid into water only | Water boils immediately on contact with concentrated acid; violent reaction |
| Storage temperature, 93% | Above −35 °C (−31 °F) | 93% freezing point |
| Storage temperature, 98% | Above −2 °C (28.4 °F); insulate or heat in cold climates | 98% freezing point; supplier practice for tank cars |
| Storage temperature, oleum | Above 2 to 21 °C depending on free SO3 | Oleum melting points by SO3 content |
| Headspace | Dry inert gas purge, or no desiccant pot at all | Moisture corrodes the inner shell; wet desiccant can block the vent |
| Plant or padding air | Dew point below −40 °C; no oil or particulate | Protects the acid and any lining from moisture and contamination |
| Level | Independent high-level alarm | Overfilling protection independent of the level indicator |
| Vent | Goose-neck atmospheric vent, never blocked | Rupture or implosion during fill and withdrawal |
| Hot work near a full tank | Vent with large air volume, explosives test, keep air on | Hydrogen in the headspace from slow reaction with steel |
The Other Acids: HCl, HNO3, H3PO4 and HF Choose Differently
Sulfuric acid gets the attention, but three of the other four acids are more common in chemical plants, plating shops and water treatment than in pulp mills, and each one changes the material question in its own direction.
Hydrochloric Acid: the Vapour Is the Problem, Not the Liquid
The ILO/WHO card describes hydrochloric acid as a strong acid in solution that attacks many metals in the presence of water, producing hydrogen, and notes that the gas is heavier than air. Three facts, three consequences. The attack on metal needs water present, so a dry system behaves differently from a wet one. The reaction produces hydrogen. And the vapour accumulates low, which matters for pits, sumps and the bottom of an enclosure as much as for the tank.
On the polymer scale, hydrochloric acid at 10% is 1/1 and at 37% is 2/3 — good at 20 °C, limited use at 60 °C. For a plastic tank the liquid side is usually the easy part. What needs designing is the vapour space and the connections: the headspace is continuously exposed to hydrogen chloride, and the fittings on the vapour side are the same fittings, in the same polymer, as the liquid side. A tank specified only against the liquid is specified against half the duty.
Nitric Acid: an Oxidiser First, an Acid Second
The safety card leads with the oxidising property rather than the acidity: the substance is a strong oxidant, reacts violently with combustible and reducing materials, and decomposes on warming. Its boiling point is 121 °C and its melting point −41.6 °C — it stays liquid over an unusually wide range, which is convenient in storage and means a spill spreads.
The polymer answer follows directly. Polypropylene is rated 2/3 at 5% and 4/4 at 65%. Dilute nitric acid is a marginal duty at 60 °C and a reasonable one at ambient; concentrated nitric acid has no polyolefin answer at any temperature. The incompatibility also extends beyond the shell: an oxidiser stored near organic material, reducing agents, or a sulfite or hypochlorite stream is a reaction waiting for a common drain, which is why TAPPI’s siting guidance keeps sulfuric acid storage away from caustic soda, hydrochloric acid, sodium chlorate, sodium bisulfate and sulfite, sodium hypochlorite and sulfide-containing materials.
Phosphoric Acid: the Mildest of the Four, and the Easiest to Under-Specify
Phosphoric acid holds 1/1 at 25% and at 85%, at both 20 °C and 60 °C — the only acid in the table that keeps an unqualified top rating at its highest concentration in the hot column. Nothing in the chemistry argues against a thermoplastic tank, and that is exactly where the risk moves.
When chemistry stops constraining, structure starts. Phosphoric acid at 85% is a dense, viscous liquid, and viscous liquids do not drain: the tank needs a bottom detail and a slope that will actually empty it, not one that looks like it will. A mild acid is also the acid most likely to be stored in the cheapest vessel purchased against a single figure, which is how a material with no chemical objection ends up in a shell with no structural margin. The correct answer for 85% phosphoric acid is a tank designed to the same discipline as a sulfuric acid tank, minus the chemical anxiety.
Hydrofluoric Acid: the One That Needs a Written Answer, Not a Chart
Hydrofluoric acid is the acid where the published chart and the real hazard point in different places. The polymer scale rates it 2/2 — good at both temperatures. The safety card records that it boils at 20 °C, has a vapour pressure of 122 kPa at 25 °C, attacks glass and some forms of plastic, and that exposure can cause hypocalcemia.
A liquid that boils just below room temperature is not described by a liquid-resistance rating. The controlling exposure is the vapour in the headspace, the vapour at an open manhole, and the vapour at a leaking flange, and none of those appears in a 20 °C immersion test. HF is also the acid that attacks the materials a designer reaches for by reflex — glass, sight glasses, some seal faces.
We do not quote HF service from a chart, and we do not offer a default material recommendation for it. What we will do is take the full duty — concentration, temperature, headspace conditions, wetted parts, and the site’s handling procedure — and confirm in writing which components we will supply and which we will not. On a substance with this vapour pressure, a quotation that arrives without a list of exclusions has not been thought about. For the thermoplastic options generally, the range is set out under our polypropylene tank range; HF sits outside what we will supply on a default basis.
Inspection and Compliance: Which Rule Applies to Which Acid Tank
An acid storage tank attracts more regulation by reputation than by citation, and the rules that do apply are specific about their own scope. Getting the scope right matters more than knowing the number, because most of the wrong numbers in circulation are right answers to a different question.
Three Containment Rules That Are Not Interchangeable
Concentrated sulfuric acid, 110%. TAPPI states that the storage tank should be surrounded by a dike with capacity of not less than 110% of the tank capacity, and that the dike should also be protected with an acid-resistant protective coating, since sulfuric acid and sulfate salts will rapidly destroy most concrete. It adds two details that decide whether the dike works: slope the area within the dike toward a sump where a submersible pump can be used to remove any water, and direct any tank overflow to a safe area within 18 inches (46 cm) of ground level and within the containment dike.
Hazardous-waste containers, 10% or the largest container. 40 CFR 264.175 requires a containment system with a base that underlies the containers, and capacity of 10% of the volume of containers or the volume of the largest container, whichever is greater, with the base sloped or otherwise designed to drain and remove liquid. This is a rule about containers of hazardous waste, not about acid tanks as such; it becomes the applicable figure when the vessel is being used in that role.
Oil, under SPCC. 40 CFR Part 112 defines oil as oil of any kind or in any form, and enumerates petroleum, fuel oil, sludge, synthetic oils and mineral oils. Acid is not in that definition. The 110% figure for sulfuric acid does not come from the oil pollution rules, and quoting it as though it did leaves a site without the rule it actually needs.
One further siting rule is worth adding to the dike calculation. TAPPI requires that acid storage and unloading be located so that there is no chance an accidentally released acid will contact incompatible chemicals — and names caustic soda, hydrochloric acid, sodium chlorate, sodium bisulfate and sulfite, sodium hypochlorite and sulfide-containing materials. Sulfuric acid should not come into contact with sulfide-containing streams because of hydrogen sulfide formation, and a hypochlorite stream plus acid is a chlorine release. A dike that is correctly sized and drains into a shared sump with a hypochlorite line is not containment. What a hypochlorite store needs on its own side of that sump is a separate design, and it is set out in the poly bleach tank guide.
Inspection Intervals by Material, and Why They Differ
NACE RP0294-94, the standard practice for design, fabrication and inspection of tanks storing concentrated sulfuric acid and oleum at ambient temperatures, recommends that all sulfuric acid storage tanks be inspected internally at least every five years and externally every two years. TAPPI recommends following it in preference to the generic tank codes for this service, and the recommendation is aimed at steel tanks, where the inspection is looking for wall loss and lining condition.
Fabrication and inspection are one procedure in that standard, not two, and the sequence is described in how the shell is fabricated and tested.
A thermoplastic shell does not corrode on the inside in the way that interval assumes, so copying the five-year figure across is not the same discipline applied to a different material. What a plastic tank needs is inspection of the things that do degrade: welds, mechanical damage, nozzle connections, and the effects of temperature and load over time. We do not have a published interval to quote for that, and we will not invent one.
What we can state is what the shell is built and verified to: sheet from 5 mm to 30 mm depending on duty, hydrostatic testing at 1.5 times design head, ultrasonic inspection of thick-section welds and a working tolerance of ±2 mm. Those are the records an inspector will ask for, and they exist before the tank leaves the shop.
What to Keep on File for an Inspector
The file that answers questions without argument contains the design basis and the reasoning behind it: the acid and its concentration band, the maximum and normal service temperature, the specific gravity at service temperature, the material selection with the rating table and its date, the lining specification if there is one, the dike capacity calculation against tank volume, the vent sizing, the high-level alarm specification, the SDS for the stored substance, and the inspection log since commissioning.
Two smaller items belong in it as well. The UN 1830 placard requirement applies to sulfuric acid above 51%, and TAPPI notes that placards must always be in place even when the tank is empty, and must not be removed until the tank has been cleaned and all acid neutralized. And where the site relies on emergency washing, 29 CFR 1910.151 requires suitable facilities for quick drenching or flushing of the eyes and body within the work area for immediate emergency use — TAPPI’s operating version is that showers and eye wash fountains be well marked, accessible within 10 seconds by walking, supplied with tempered water close to body temperature, and that turning on either should trigger an alarm to summon help.
The Questions We Ask Before We Quote an Acid Storage Tank
Five answers decide whether the quotation is an engineering answer or a price. Which acid, exactly, including any mixture, and at what concentration band. What the maximum and normal service temperatures are, in °C, not “ambient”. The specific gravity at service temperature. Whether the tank will ever receive water, a wash-down or a dilute stream. And what the tank sits in — indoors, outdoors, or in a heated building — because the climate decides whether freezing is a design case or an irrelevance.
With those five we can give a material recommendation and a drawing inside 48 hours. Without them, we will ask, and the answers usually change the material. That conversation is cheaper than a replacement. If you would rather describe the duty than the drawing, send us the duty data.
Frequently Asked Questions
What material is best for an acid storage tank?
There is no single answer, because the material follows the concentration and the temperature. For concentrated sulfuric acid at ambient temperature, the standard industry answer is carbon steel, with a baked phenolic lining where periodic internal inspection is expected. For dilute acids, hydrochloric acid up to 37%, and phosphoric acid even at 85%, a polypropylene vessel is a practical answer at moderate temperature. For concentrated nitric acid, no polyolefin is acceptable.
Can polypropylene store 98% sulfuric acid?
Not on the strength of published data. The standard polypropylene resistance table carries rows for 10%, 78% and 93% sulfuric acid and none for 98%. The nearest row, 93%, is rated 3 at 20 °C — acceptable with light attack and limited use — and 4 at 60 °C. A 98% duty needs a written service statement from the material supplier, at that concentration and temperature, before it can be quoted.
Why does 98% sulfuric acid freeze at a higher temperature than 93%?
Because the freezing point of sulfuric acid rises with concentration in this range. 93% freezes at −35 °C (−31 °F) and 98% at −2 °C (28.4 °F). The stronger acid is the one that solidifies in ordinary winter weather, which is why 98% rail cars may be insulated and fitted with heating coils while 93% cars are not.
How large should the containment dike be for a sulfuric acid tank?
For an acid storage tank holding concentrated sulfuric acid, the industry guidance is a dike with capacity of not less than 110% of the tank capacity, protected with an acid-resistant coating because sulfuric acid and sulfate salts rapidly destroy most concrete, and sloped to a sump with a pump for water removal. The 10% figure that is often quoted belongs to the hazardous-waste container rule and applies to a different scope.
Is a plastic tank suitable for nitric acid?
Only at low concentration. Polypropylene is rated 2 at 20 °C and 3 at 60 °C for 5% nitric acid, but 4 at both temperatures for 65%. Rating 4 means unacceptable, significant attack, and wall thickness does not change it.
What temperature can a polypropylene acid tank run at?
Our fabricated tanks are rated for service from −10 °C to 95 °C, which is a stiffness limit. The published chemical-resistance data stops at 60 °C, so a duty between 60 °C and 95 °C sits inside our structural rating and outside the published chemical evidence. We quote that range against a stated duty and a written material position, not by interpolation.
Can I dilute concentrated sulfuric acid inside the storage tank?
No. Adding water to concentrated sulfuric acid is extremely exothermic — the water boils immediately on contact and the reaction is violent. Dilution belongs in a dedicated, agitated, cooled vessel with the acid metered into the water, and a bulk user who needs dilute acid should buy it dilute or dilute downstream of storage.
Do you supply acid transport tanks or ISO tanks?
No. We build fixed atmospheric storage and process vessels. Transport containers are a different product with a different code basis and a different regulatory regime — the UN 1830 placard, for example, applies to sulfuric acid above 51%, and concentrated sulfuric acid rail cars are subject to unloading restrictions that do not apply to a fixed tank on a foundation.
Get an Acid Storage Tank Built for Your Concentration
Send us the acid, the concentration band, the service temperature, the specific gravity and whether the tank sits indoors or out, and we will tell you which material we would build and why. Where the answer is that a thermoplastic is the wrong choice for the duty, we will say so — that is cheaper for both sides than a tank that fails in service.
We have been fabricating industrial plastic equipment since 2009, which is 17 years. Our tanks use 5 mm to 30 mm sheet, hydrostatic testing at 1.5 times design head, ultrasonic inspection of thick-section welds and a working tolerance of ±2 mm. We operate more than 40 production bases and offices, and hold ISO 9001, ISO 14001, CE, SGS and RoHS. The range is set out under polypropylene tanks, and the drawing and quotation stage starts with our engineering team.
Note on the figures — Density, freezing point, viscosity, boiling point and vapour pressure figures for 93% and 98% sulfuric acid are as published by TAPPI in TIP 0606-26; safety-card data for the pure acids are from the ILO/WHO International Chemical Safety Cards and NOAA CAMEO. Chemical-resistance ratings are the published values at 20 °C and 60 °C only, with no interpolation between them, and a missing row is treated here as missing evidence rather than a pass. Regulatory figures are quoted from the U.S. Code of Federal Regulations, which is written in imperial units; metric values in brackets are our own conversions and the original is always given. Sheet thickness, test pressure, tolerance, service temperature range, warranty, lead time and the company figures are our own manufacturing and product values, not third-party standards.
Sources
- TAPPI — TIP 0606-26 — Sulfuric acid (H2SO4) safe storage and handling, revised 2012 (physical properties of 93% and 98% acid including density, viscosity of 22 and 25 cP at 20 °C, pH below 0.1, freezing points of −35 °C and −2 °C, boiling points of 279 °C and 327 °C and vapour pressures at 40 °C; the add-acid-to-water rule and immediate boiling of water on contact; carbon steel and certain stainless steels for acid at normal ambient temperatures and commercial strengths where periodic entry is not required; baked phenolic lining where entry is expected and the corrosion caused by washing iron sulfate paste; slow reaction with steel producing hydrogen and the hot-work precautions; tanks under 10,000 gallons in stainless or special HDPE, reducing hydrogen and iron sulfate; Alloy 20 above 6 ft/s and 316 or Alloy 20 at nozzles above 3 ft/s; PVC and CPVC not recommended for piping because of mechanical failure risk; Viton B gaskets and Teflon-lined hoses; dike capacity of at least 110% of tank capacity with an acid-resistant coating because sulfuric acid and sulfate salts destroy most concrete; slope to a sump; overflow within 18 inches of ground level; 24-inch minimum top manhole; separate high-level alarm; moisture ingress in humid environments, nitrogen padding, and why desiccant pots are not recommended; plant air below −40 °C dew point; showers and eye wash within 10 seconds by walking, tempered water and alarm; UN 1830 above 51% concentration and placards retained on empty tanks; bottom unloading restrictions for rail cars; NACE RP0294-94 with internal inspection at least every five years and external every two years; API 650 and ASME VIII Division 1 as baseline codes; oleum scope).
- ILO / WHO International Chemical Safety Cards — ICSC 0362 — Sulfuric acid (relative density 1.8 at 20 °C; melting point 10 °C; decomposes at 340 °C; vapour pressure negligible at 20 °C; attacks many plastics; never pour water into this substance, add it slowly to the water).
- NOAA / U.S. EPA CAMEO Chemicals — Sulfuric acid (CAS 7664-93-9) (specific gravity 1.841; melting point 50.65 °F; reaction with water negligible unless acid strength is above 80–90%, above which heat from hydrolysis is extreme).
- ILO / WHO International Chemical Safety Cards — ICSC 1447 — Oleum (mixture of sulfuric acid and sulfur trioxide; relative density 1.9; attacks some plastics; melting points of about 2 °C at 20% SO3, 21 °C at 30% and 5 °C at 65%; dilution rule).
- NOAA / U.S. EPA CAMEO Chemicals — Sulfuric acid, fuming (density 16.5 lb/gal; thick fuming yellow liquid; grades such as 103% with 13% free SO3; dissolution generates dangerous heat causing localized boiling and spattering).
- ILO / WHO International Chemical Safety Cards — ICSC 0163 — Hydrochloric acid (strong acid in aqueous solution; attacks many metals in the presence of water with evolution of hydrogen; the gas is heavier than air).
- ILO / WHO International Chemical Safety Cards — ICSC 0183 — Nitric acid (strong oxidant; reacts violently with combustible and reducing materials; decomposes on warming; boiling point 121 °C; melting point −41.6 °C).
- ILO / WHO International Chemical Safety Cards — ICSC 0283 — Hydrofluoric acid (boiling point 20 °C; vapour pressure 122 kPa at 25 °C; attacks glass and some forms of plastic; exposure can cause hypocalcemia).
- U.S. Electronic Code of Federal Regulations — 40 CFR 264.175 — Containment (containment capacity of 10% of the volume of containers or the volume of the largest container, whichever is greater; base sloped or designed to drain and remove liquid).
- U.S. Electronic Code of Federal Regulations — 29 CFR 1910.151 — Medical services and first aid (suitable facilities for quick drenching or flushing of the eyes and body within the work area for immediate emergency use).
- U.S. Electronic Code of Federal Regulations — 40 CFR Part 112 — Oil Pollution Prevention (definition of oil covering oil of any kind or in any form, including petroleum, fuel oil, sludge, synthetic oils and mineral oils).
- The Engineering ToolBox — PP Polypropylene — Chemical Resistance (five-point attack rating scale from excellent to unacceptable; ratings at 20 °C and 60 °C; sulfuric acid 10%, 78% and 93%, hydrochloric acid 10% and 37%, nitric acid 5% and 65%, phosphoric acid 25% and 85%, hydrofluoric acid).
- INEOS Olefins & Polymers USA — Typical Engineering Properties of High Density Polyethylene (density 0.930–0.965 g/cm³; Vicat softening temperature 132 °C homopolymer and 112–130 °C copolymer).
