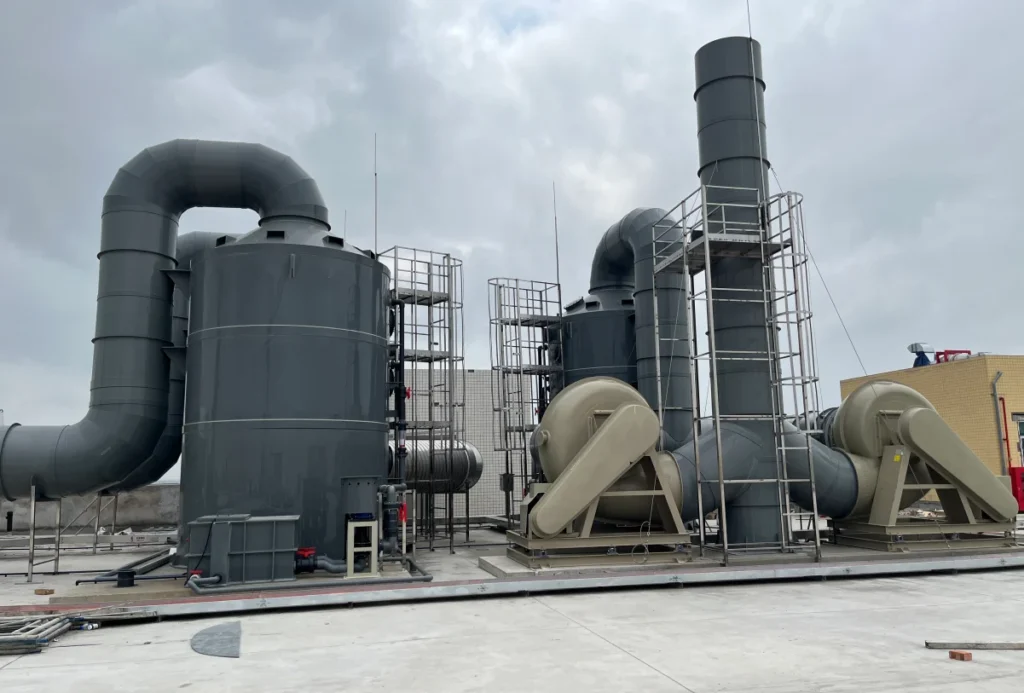
Key Takeaways: Centrifugal Exhaust Fan for Gas Treatment
- A centrifugal exhaust fan is the engine of a gas-treatment train, and its position is decided before its size. The fan either pulls from downstream of the scrubber or carbon box, holding the whole chain under negative pressure, or pushes from upstream — and that choice sets leak direction, wetted duty on the wheel, and vessel sealing before a single cubic meter is sized.
- The honest centrifugal exhaust fan starts from the worst-case system curve. Scrubber packing adds roughly 1 to 3 kPa and a carbon box roughly 1 to 2 kPa, and both climb as the media loads with contaminant, so the machine clears the dirtiest operating point the train will ever see — not the clean one a first pass suggests.
- Induced draft — the fan after the scrubber — wins for hazardous gas. With the control vessel under negative pressure, any small housing leak pulls air inward instead of pushing contaminated gas outward, which is why acid and VOC trains conventionally put the centrifugal exhaust fan on the discharge side, behind the mist eliminator.
- A wetted centrifugal exhaust fan is built PP or FRP with the motor out of the airstream. Wet, droplet-laden, acidic air on the discharge side of a scrubber is some of the hardest duty a wheel can face; welded polymer construction plus an isolated motor is the standard protective answer rather than an option.
- One single-stage centrifugal exhaust fan clears most commercial trains; tall stacks go two stages. Polymer machines handle the typical system under about 15 kPa, and for taller stacks or heavier vessels, series staging takes two centrifugal exhaust fan stages toward 30 kPa of total resistance.
Overview: Where a Centrifugal Exhaust Fan Works in Gas Treatment
A wet scrubber removes a contaminant from an air stream by contacting it with liquid, and an activated carbon box does the same job by adsorption; neither one, by itself, moves the air. The movement comes from a fan, and in industrial gas-treatment service that machine is almost always a centrifugal exhaust fan — a pressure-capable unit sitting somewhere on the treatment train, sized to hold the whole chain of hoods, ducts, and control vessels within a designed pressure window. This article keeps the machinery question in one place: which centrifugal exhaust fan do you put on the train, on which side of the scrubber or carbon box, and how do you size it so the treatment system actually performs to its permit?
The train itself is the inside story of the two sibling guides on this site. The wet scrubber fundamentals guide and its waste-gas treatment companion define what the tower must do, the VOC scrubber systems guide carries the organic side, and the activated carbon adsorption box, its OEM build guide, and carbon–HEPA hybrid define the carbon path. What those guides assume — a fan that will pull the right flow through at the right pressure — is exactly the job filled by the centrifugal exhaust fan, and it is covered here: the two layout philosophies, the resistance budget that decides the fan curve, the material and drive choices for corrosive streams, and the case where one machine is not enough.
The decision framework follows a fixed order: decide the layout (induced versus forced draft) from the gas hazard, add every pressure element from capture to stack and take the worst-case loaded value as the operating point, then choose wheel, material, and drive against that point, and verify the installed machine against the real system curve at commissioning. Worked correctly, the treatment train and its centrifugal exhaust fans are sized as one system rather than as a fan bolted to an afterthought, which is why the train’s fan question deserves its own guide.
Gas-Treatment Trains and Where the Centrifugal Exhaust Fan Sits
Every gas-treatment system is the same skeleton with different organs: an entry capture point draws contaminated air out of the process, a duct carries it to a control device, the device treats it, and a stack discharges the clean stream to atmosphere. The centrifugal exhaust fan sits somewhere on that skeleton, and its physical position — between which two organs — is a design decision with consequences for safety, corrosion, and energy, not just a plumbing detail.
Entry Capture and Duct
Fume extraction hoods, tank covers, enclosure vents, and glove box ports set the entry airflow. Their entry losses are small but never zero — an 80 to 120 fpm face velocity over a hood opening converts to a modest but real pressure loss, and long or multiply-elbowed duct runs add their share at the design flow. This entry segment fixes the minimum CFM the train must carry; nothing downstream can reduce it, and the centrifugal exhaust fan is the only component that enforces the capture velocity in the first place.
The Control Device
The scrubber tower or activated carbon box sits in the middle and is usually the single largest pressure consumer. A packed wet scrubber runs roughly 1 to 3 kPa across its packing, support plate, and mist eliminator depending on depth and liquid rate; an activated carbon box adds roughly 1 to 2 kPa across the bed and grows as adsorption proceeds; a HEPA stage on top of carbon adds another 0.6 to 1.2 kPa when it is fresh and more as it cements in dust. These figures are the raw material of the pressure budget, and they matter because the fan must hold the operating point while the device state changes over a shift, a week, and a service year.
The Fan Position
Two positions exhaust the practical layouts. In an induced-draft arrangement the centrifugal exhaust fan is the last machine, downstream of the control device, pulling air through the chain so the vessel and duct upstream of it sit under negative pressure. In a forced-draft arrangement the fan leads, upstream of the device, pushing air through so the vessel sits under positive pressure. The names are often borrowed from boiler drafting, and the safety logic transfers directly: a fan on the discharge side of a hazardous-gas treatment vessel means leaks in that vessel pull inward, while a fan on the intake side means leaks push contaminated air outward.
The Stack
The stack is not a free ride. Height generates stack draft that helps the fan, but the fan never relies on it against the elevator’s own flow resistance, and the stack discharge velocity required by plume dispersion adds exit loss on top of the duct run. For tall stacks serving heavy treatment systems, that height-related resistance is precisely what pushes the train past a single machine’s pressure ceiling — the staging case covered later.
Induced Draft vs Forced Draft: Which Side of the Scrubber?
The single most consequential choice in a gas-treatment fan design is the side of the control device the centrifugal exhaust fan sits on. It is a choice about leak direction and wetted duty more than about pressure, and it should be made from the gas chemistry before any sizing starts.
Induced Draft — Fan Downstream, System Under Negative Pressure
In the induced-draft layout the centrifugal exhaust fan pulls gas through the scrubber or carbon box. Every flange, weld, and manway upstream of the fan inlet is at negative pressure relative to the room, so if a seal is imperfect the airflow bows inward and ambient air leaks into the system — hazardous vapor does not escape. For acid fumes, VOC-laden air, and any stream that would hurt people near a small leak, this is the safety-winning arrangement, and the treatment industry uses it as the default for exactly that reason. The cost is what the fan inhales: on the discharge side of a wet scrubber the air is saturated and may carry droplets and carryover, so the induced-draft centrifugal exhaust fan must be a wetted machine with drainage, a gust and mist-tolerant wheel, and corrosion-resistant construction.
Forced Draft — Fan Upstream, System Under Positive Pressure
In the forced-draft layout the fan blows into the device. The vessel and its ductwork upstream of the discharge sit under positive pressure, so any seal fault pushes air out — acceptable when the train handles relatively benign streams, but a serious consideration when it handles hazardous ones, because an imperfect vessel then leaks contamination into the plant rather than drawing air inward. The offsetting advantage is that the fan sees the inlet side, comparatively dry and clean upstream of the treatment, and the motor and impeller live in a kinder atmosphere at the cost of demanding a tighter, pressure-rated vessel.
How to Decide
The decision table is short and defensible. Corrosive or toxic gas, wet-side treatment with a mist eliminator, and a leak that would matter → induced draft, fan after the device. Benign or non-hazardous gas where a modest outward leak is tolerable, or a scrubber that must be fed with a pre-spray fan → forced draft. Commercial practice for acid and VOC treatment on this site’s own product spreads — the industrial wet scrubber train and the chemical resistant exhaust fan guide — keeps the centrifugal exhaust fan on the discharge side behind the mist eliminator, and the remainder of this article follows that arrangement while flagging where the forced-draft variant changes the answer.
| Design decision | Induced draft (fan after device) | Forced draft (fan before device) |
|---|---|---|
| Leak direction at vessel | Inward — hazardous vapor stays inside | Outward — leaks contaminate the room |
| Fan airstream duty | Saturated, droplet-loaded, acidic after wet scrubber | Cleaner, drier inlet air before the device |
| Vessel sealing requirement | Fugitive-tolerant (vacuum side) | Pressure-tight required |
| Typical choice of service | Acid fumes, VOC, hazardous organics | Dust, benign fumes, pre-spray feed |
| Fan construction implication | PP or FRP, drained, mist-tolerant wheel | Metal sometimes acceptable; PP/FRP for corrosion |
Keeping Hazardous Gas on the Right Side of the Fan
When the train handles acid fumes, solvent vapor, or any flammable or toxic stream, three safety rules sit above the sizing math. They are the same rules the laboratory exhaust codes apply to fume cupboards, and they transfer to industrial treatment trains unchanged.
Leak Direction Is a Safety Feature, Not a Side Effect
The induced-draft arrangement is the primary way a hazardous-gas centrifugal exhaust fan enforces containment. Placing the fan downstream means the control vessel and all ductwork upstream of the inlet run negative; a hairline crack or slipped gasket then admits room air rather than discharging process gas. That single property is why treatment trains for acid and VOC duty are drawn with the fan last, and why the vessel side of the train need not be rated to the same pressure-tight standard as a forced-draft system handling the same chemistry — the vacuum works for you rather than against you.
Spark Resistance and the Wheel
The fan is the only rotating machine in the train, and the wheel is where an ignition source would appear. A polymer impeller striking nothing inside its own polymer housing cannot raise the metallic spark that a steel impeller against a steel housing can, which is the practical meaning of the spark-resistant and non-sparking fan requirement carried by the treatment and ventilation codes — the same requirement the laboratory references in the fume cupboard exhaust guide. A centrifugal exhaust fan built with a polypropylene or FRP wheel on a steel shaft, that shaft sealed against the casement, satisfies the requirement as a construction property rather than as a coating patch.
Motor Isolation
The electric motor is the machine most likely to arc in normal operation, so it has no business living in the airstream. Belt-driven centrifugal exhaust fans keep the motor outboard, outside the corrosive and potentially flammable gas path, and direct-drive builds mount the motor shaft-sealed and isolated at the casement. Where the gas or the code demands it, the motor carries an explosion-proof classification and the fan is specified as spark-resistant per the ventilation standard — the same three-part test the fume cupboard regulations apply, and here applied to the whole industrial train.
Budgeting Every Element’s Resistance
A centrifugal exhaust fan is selected against a number, and that number is the total system resistance at the required flow — nothing more and nothing less. The method, the same one the high pressure blower selection guide teaches for process duty, is to add every pressure-consuming element from capture to stack, write the sum, and take the worst-case loaded value — not the cleanest — as the operating point.
Control-Device Losses and Their Dirty Factor
The control device dominates the budget. A packed scrubber is roughly 1 to 3 kPa across packing, support plate, and mist eliminator at design liquid rate; an activated carbon box is roughly 1 to 2 kPa and climbs as the bed loads; a HEPA stage adds roughly 0.6 to 1.2 kPa fresh and more as it traps dust. None of these are fixed. Media loading is a unidirectional ratchet: carbon bed pressure rises across the service life, packing accumulates solids, and a HEPA element marches toward replacement pressure. The system curve a carbon–HEPA hybrid box follows is therefore a family of curves that climbs with time, and the worst — the loaded, pre-change-out state — is the honest design point.
The Worst-Case Setpoint Rule
Specifying a centrifugal exhaust fan against clean filters is the classic commissioning failure: the machine runs flat and quiet at start, then starves the capture points as the media loads and the exposed system resistance climbs past the fan’s dotted curve. The rule that prevents it is to write the budget with the dirtiest every component will be immediately before service or change-out — the worst-case system resistance — and to select so the fan crosses that highest curve with margin, because with a fixed-speed machine there is no second chance to buy back pressure later. For the wet scrubber path, the train and its exhaust fan should be specified so the operating point sits on the fan curve with the packing at its practical maximum loading; the same rail applies to every element in Table 2.
| Train element | Typical clean ΔP | Dirty / loaded multiplier | Notes for the budget |
|---|---|---|---|
| Capture hood / duct entry | 0.1–0.3 kPa | ~1.0 | Fixed; sets the required CFM |
| Duct run with elbows | 0.2–1.0 kPa | 1.0–1.2 | Grows with dust settlement / deposition |
| Packed scrubber | 1–3 kPa | 1.3–1.5 | Scaling and solids raise packing ΔP |
| Activated carbon box | 1–2 kPa | 1.5–2.0 | Rises as bed loads; rate-limiting element |
| HEPA stage | 0.6–1.2 kPa | 1.5–2.5 | Rises toward change-out pressure |
| Mist eliminator | 0.2–0.5 kPa | 1.2 | Tests in the scrubber element budget |
| Stack duct + exit | 0.3–1.0 kPa | 1.0–1.2 | Tall stacks add height-related resistance |
The Induced-Draft Layout (Fan After the Scrubber)
With the decision made for hazardous, wet-side service, the natural home of the centrifugal exhaust fan is after the mist eliminator on the scrubber’s discharge, or after the ductwork connecting the carbon box, pulling negative on everything upstream. This is the “fan last” arrangement that gives the train its leak-direction safety, and it gives the fan the hardest air in the system — so the construction details are what keep the arrangement practical.
Wet-Side Protection for the Wheel and Housing
Air leaving a wet scrubber is saturated and can carry droplets of the scrubbing liquid, which means the centrifugal exhaust fan on that duty sees moisture and whatever chemistry the liquid holds. The protective standard is a welded polymer machine: a polypropylene or fiberglass-reinforced wheel and casement that treats the occasional droplet as a wetted-wall surface rather than a corrosion event, a drain at the scroll’s lowest point to shed accumulated liquid between runs, and a shaft seal so the bearing and motor end stay out of the vapor zone. The wheel type follows the droplet load — a backward-curved wheel keeps droplets moving through cleanly on moderately clean scrubber discharge, while a radial wheel with a recessed or covered side plate shrugs off heavier carryover and particles, a construction the general centrifugal fan reference and the forward versus backward curved fan comparison both place concretely in wheel-construction terms.
Fitted to the Carbon Side Too
The carbon path earns the same layout. An activated carbon adsorption box downstream of a scrubber, or feeding a HEPA stage, puts the exhaust fan on the discharge side of the last vessel, and the same rules apply: negative pressure on the box, the fan seeing near-dry treatable air on the clean path yet still specified in PP or FRP where any acid carryover precedes it, plus the speed headroom to answer a rising carbon bed. This is the exhaust fan for a carbon box’s operating life — it must be sized so that when the bed reaches its practical loading and the system curve climbs, the fan still clears the required capture flow, a behavior that leads directly to the speed-control question later in this guide.
The Forced-Draft Layout (Fan Before the Scrubber)
When the process stream is benign enough that an occasional outward leak is tolerable — dust-laden air, cooling-tower carryover, non-hazardous ventilation exhaust that still needs treatment before discharge — the fan can lead the train. A forced-draft centrifugal exhaust fan sits at the train’s intake, blows into the scrubber or baghouse, and trades the safety of negative pressure for a cleaner life for the machine.
Sealing the Vessel Under Positive Pressure
The price of fan-first is written on the vessel. With the fan pushing, the scrubber tower and its connection duct sit above ambient, so every flange and inspection hatch must be rated and proven pressure-tight; a forced-draft train leaks process air outward through any imperfection, which is exactly the failure mode induced draft exists to avoid. Vessel sealing, gasketed connections, and leak-testing the vessel before commissioning therefore stop being optional on the forced-draft side, and the same raising applies to the carbon box where a forced-draft fan feeds it — the carbon path is sensitive to this because a pressure-tight carbon vessel is harder to field-verify once duct is attached.
The Dry-Inlet Advantage
What the arrangement buys is kindness to the rotating machinery. The fan sees inlet air before any wet contact — dry, close to ambient temperature on the majority of streams, free of the saturated droplets the discharge side would throw at the wheel — so a metal or coated impeller may survive where a discharge-side machine would eat itself in weeks, and the motor room stays ordinary. The practical recommendation is narrow, not a wildcard: a forced-draft centrifugal exhaust fan for dust or low-corrosion benign fume, with the wheel selected from the material guide below when the incoming stream still carries chemistry, and the vessel itself upgraded to the pressure-tight standard the layout demands.
Corrosion, Motor Isolation, and Speed Control
The machine itself resolves into three linked choices — material by the stream’s chemistry, drive by the need to isolate the motor and span the operating range, and speed control by the fact that the system curve of a treatment train moves over its service life. Each one is decided against the others, and a centrifugal exhaust fan for gas treatment is the sum of all three.
PP vs FRP for the Exhaust Stream
Material follows the chemistry and temperature of the air at the fan flange. Polypropylene takes dilute mineral acids, dilute caustics, and common organic solvent vapors at the ordinary exhaust temperatures of a scrubber discharge, welds into a corrosion vessel for the gas, and carries continuous service to roughly 180 to 190°F; fiberglass-reinforced plastic succeeds it where the stream is hotter, stronger in acid, or mechanically harder duty, adding the structural margin that high-static and carbon-train fans need as the glass-reinforced plastic reference and this site’s FRP versus PP comparison lay out together.
The screw-turn on this fan duty is that the exhaust streams here are wet-side: PP handled a wetted wall by surface and shrugs off carryover, and FRP adds the strength where the wheel and shaft seals carry the droplet load — so the practical split is a polypropylene exhaust fan for the standard dilute-acid scrubber discharge, an frp exhaust fan where the stream is hotter, stronger in acid, or mechanically stressed, and fiberglass ahead where the wheel and shaft seals carry the heaviest droplet load — exactly the spread covered across the corrosion resistant blower guide and the machine lines of PP blowers and FRP blowers.
Belt vs Direct Drive — Putting the Motor Outside the Gas
The drive’s first job is distance. Belt-driven centrifugal exhaust fans park the motor outboard of the casement, out of the corrosive and potentially flammable gas path, at the cost of keeping sheaves, belts, and their alignment; direct-drive builds run the impeller on the motor shaft with a shaft seal and skip the belt maintenance, at the cost of the motor living closer to the wetted machine. The direct drive selection guide keeps the practical chart: belt drive for streams where the motor must be isolated and some speed range is welcome, direct drive where shaft sealing is clean and uptime beats adjustability, and the polymer wheel’s own limits respected on tip speed in both — the wheel side is covered by the polypropylene fan blade and impeller guide.
VFD for a Shifting System Curve
Last comes speed, and it is the one requirement the treatment train imposes that a plain fixed-speed machine answers poorly. Because the carbon bed and packed media load, the honest system curve climbs across the service life; a variable-frequency drive lets the exhaust fan for that carbon box run faster as the resistance rises, holding the capture CFM constant from fresh media to change-out instead of watching flow decay with the bed. Specify the motor and the polymer wheel so the VFD band covers the dirty setpoint with margin — the machine crosses the clean system curve near the bottom of its speed band and the loaded curve near the top, which is the operating pattern that keeps a gas-treatment centrifugal exhaust fan affordable through a whole media cycle rather than oversized only on day one.
| Choice | For the wet acid discharge side | For the cleaner inlet or carbon path |
|---|---|---|
| Material | PP or FRP welded, drained housing | PP/FRP for carryover; metal OK if truly dry |
| Wheel | Backward-curved (clean) / radial (carryover) | Backward-curved or forward-curved light duty |
| Drive | Belt, motor outboard of the casement | Direct drive with shaft seal, or belt |
| Speed control | VFD — mandatory for carbon bed aging | Fixed or VFD by capture-point stability needs |
| Motor class | Explosion-proof / flameproof where gas is flammable | Standard TEFC for benign streams |
When One Fan Isn’t Enough (Staging for Tall Stacks)
Most commercial gas-treatment trains stay under roughly 8 kPa of total resistance — a scrubber, its duct, a modest stack — and a single centrifugal exhaust fan clears them. Past that ceiling, and for tall stacks whose height adds real resistance back into the system, the honest engineering answer is not a bigger single machine but series staging: two centrifugal exhaust fans in the same airstream, adding pressure stage on stage while sharing the flow.
The Single-Stage Ceiling and the Two-Stage Answer
A polymer centrifugal exhaust fan has a practical pressure ceiling set by wheel tip speed and the material’s structural limit. For PP and FRP impellers this site’s engineering family puts the single-stage ceiling near 15 kPa — beyond which the composite wheel itself is the constraint, not the motor. Series staging answers it: two single-stage fans in one duct, the second taking the first’s discharge, each doing its share so the pair delivers roughly twice the pressure while both run inside their comfortable speed band. The two-stage and multistage blower guide holds the full pressure ladder — single stage to 15 kPa, shell-internally two-staged to about 30 kPa, and lined-steel beyond — and the same staircase carries here: a tall stack or a heavy carbon-plus-HEPA chain that totals past the single ceiling is exactly the case built as two stages in series.
Where Staging Is Worth It on a Treatment Train
Staging earns its cost in three concrete situations on the gas-treatment side. The tall-stack discharge train, where stack height and exit loss push the total past the single-stage curve; the carbon-heavy chain, where a thick deep bed plus a HEPA stage compound to a resistance a single machine would have to run at its structural limit to clear; and the high-capacity acid scrubber where the packing is deep enough that one fan would need an oversized wheel. In all three, the two stages are specified as one matched pair on a shared system curve, each assigned its part of the total, sharing a VFD strategy so the lead machine follows the base load and the second trims — the same division the single-machine budget learns from the worst-case rule, now split between two centrifugal exhaust fans sized once and run in tune.
Commissioning: Fan Curve vs the Real System Curve
A centrifugal exhaust fan delivers published performance only when the installed system actually behaves like the curve it was chosen against, and on a gas-treatment train the gap between the designed system and the welded, ducted, silencer-and-stack reality is where the classic failures hide. Commissioning closes the loop with two checks.
Certified Ratings and the Nameplate Story
Start from ratings that mean something: a fan tested against an air-movement standard — the ANSI/ISO test methods whose certification the AMCA (Air Movement and Control Association) administers through independent laboratories — is a fan whose curve, sound, and power data were measured, not estimated. Insist on certified fan curves from the supplier, read the nameplate pressure against the budget you wrote in the resistance table, and treat a claimed curve without a test standard as a resume you cannot audit. The same discipline in the selection phase is what the Department of Energy fan system resources teach for system efficiency: a fan system performs along its system curve, and the machine is only as good as the honesty of that curve — clean bids, dirty reality.
Field Checks Before the Permit Runs
With the machine installed, verify rather than trust. Read static pressure at taps on each side of the train — before the scrubber, across the carbon box, across the fan — convert the differentials to the operating point, and plot the measured point against the supplier curve: a centrifugal exhaust fan whose measured point lands on its curve where the budget expected it is a fan sized correctly; one that lands short or to the right of expectations is a sign of an underestimated system — longer duct, higher loaded media, or a closed balancing damper — not a sign to ignore. Repeat the pressure scan as the media loads in the first weeks, confirm the VFD rides the rising system curve instead of letting flow decay, and only then treat the capture-point velocities as proven. That measured closeout is the difference between a treatment train that performs to its permit from day one and one that starves its own scrubber before the first change-out.
FAQ
Should a centrifugal exhaust fan go before or after the scrubber?
For hazardous, acidic, or VOC-laden air, put the fan after the control device — induced draft — so the scrubber and duct upstream run under negative pressure and any imperfect seal pulls air inward instead of pushing contaminated gas into the room. Choose fan-first (forced draft) only for benign streams where a small outward leak is tolerable. The induced arrangement is the default for the acid and carbon trains this guide covers.
How do I size the exhaust fan for a gas-treatment train?
Add the pressure of every element from capture to stack — hood entry, duct, scrubber packing roughly 1 to 3 kPa, carbon bed roughly 1 to 2 kPa, HEPA stage, mist eliminator, stack exit — at the design flow, and use the worst-case loaded value, not the clean one. Draw that system curve and select a fan whose certified curve clears the worst point with margin. Most commercial trains land under about 8 kPa and fit a single single-stage machine.
Why does a carbon box fan need a variable-frequency drive?
Because an activated carbon bed’s resistance rises as it loads. Fresh media sits at the low end of its pressure range; by change-out the bed can sit at roughly 1.5 to 2 times its clean resistance. A VFD lets the exhaust fan run faster as the system curve climbs, holding the capture flow constant from fresh media to change-out instead of letting it decay with the bed.
Polypropylene or FRP for the exhaust stream — which do I pick?
Polypropylene takes dilute mineral acids, dilute caustics, and common solvent vapors at normal exhaust temperatures up to roughly 180 to 190°F, and welds into a leak-free wetted-wall vessel; fiberglass-reinforced plastic takes over for hotter, stronger-acid, or mechanically heavier duty. On a scrubber discharge, PP is the standard dilute-acid answer and FRP the strong-acid and high-static answer.
Can one fan serve a scrubber and a carbon box in series?
Yes, when the combined resistance stays inside one single-stage machine’s curve. A scrubber feeding a carbon box — or a carbon box feeding a HEPA stage — is one chain with the fan on the discharge side of the last vessel, sized for the sum of both devices plus duct at the worse loaded state. When that sum passes the single-stage ceiling, the honest answer is series staging two fans rather than pushing one machine to its structural limit.
When do I need two fans in series instead of one?
When the honest worst-case system resistance passes the single-stage pressure ceiling — near 15 kPa for polymer wheels, per this site’s engineering family. Tall stacks, deep carbon beds plus HEPA, and deep-packed acid scrubbers are the practical triggers. Two single-stage fans in one duct split the total, each running inside its comfortable band, and the pair is controlled as one system with shared VFD strategy.
Get Your Gas-Treatment Fan Sized to the Real Curve
This guide reduces to one exchange: the gas chemistry (which sets the induced-versus-forced decision and the material), the required capture CFM, the worst-case system resistance taken loaded, and the stack height. Anyone can supply those four numbers and get a centrifugal exhaust fan specified to the operating point rather than to a catalog page — induced-draft discharge side for the hazardous train, PP or FRP by the stream, radial or backward-curved wheel by the carryover, motor outboard, and VFD wound for the carbon bed’s rise. The machines on the PP and FRP blower range are built on exactly that material and curve logic, and sending the four numbers gets a matched recommendation for the whole train — scrubber and fan specified against the same curve, not bolted together afterwards.